48-Inch ANSI B16.9 A234 WPB Carbon Steel Welding Tee Enquiry
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty1 Yearcustomized supportOEM
-
TechnicFORGEDConnectivityWelding
-
shapeEqualhead codeHexagon
-
Overall LengthCustomized SizeHeightCustomized Size
-
Surface TreatmentPlainPressureHigh Pressure
-
System of MeasurementMetricMounting hole diameterCustomized Size
-
Pipe FeaturesOtherPipe ClassOther
-
ApplicationOtherThread TypesCustomized Size
For this 48-inch ANSI B16.9 A234 WPB carbon steel welding tee enquiry, establish what the title’s size describes. Confirm whether it refers to the run, branch or another dimension, and obtain individual supply confirmation. The actual size option is a shared half-inch-to110-inch label rather than a detailed availability list.
Approve the large-size run and branch arrangement
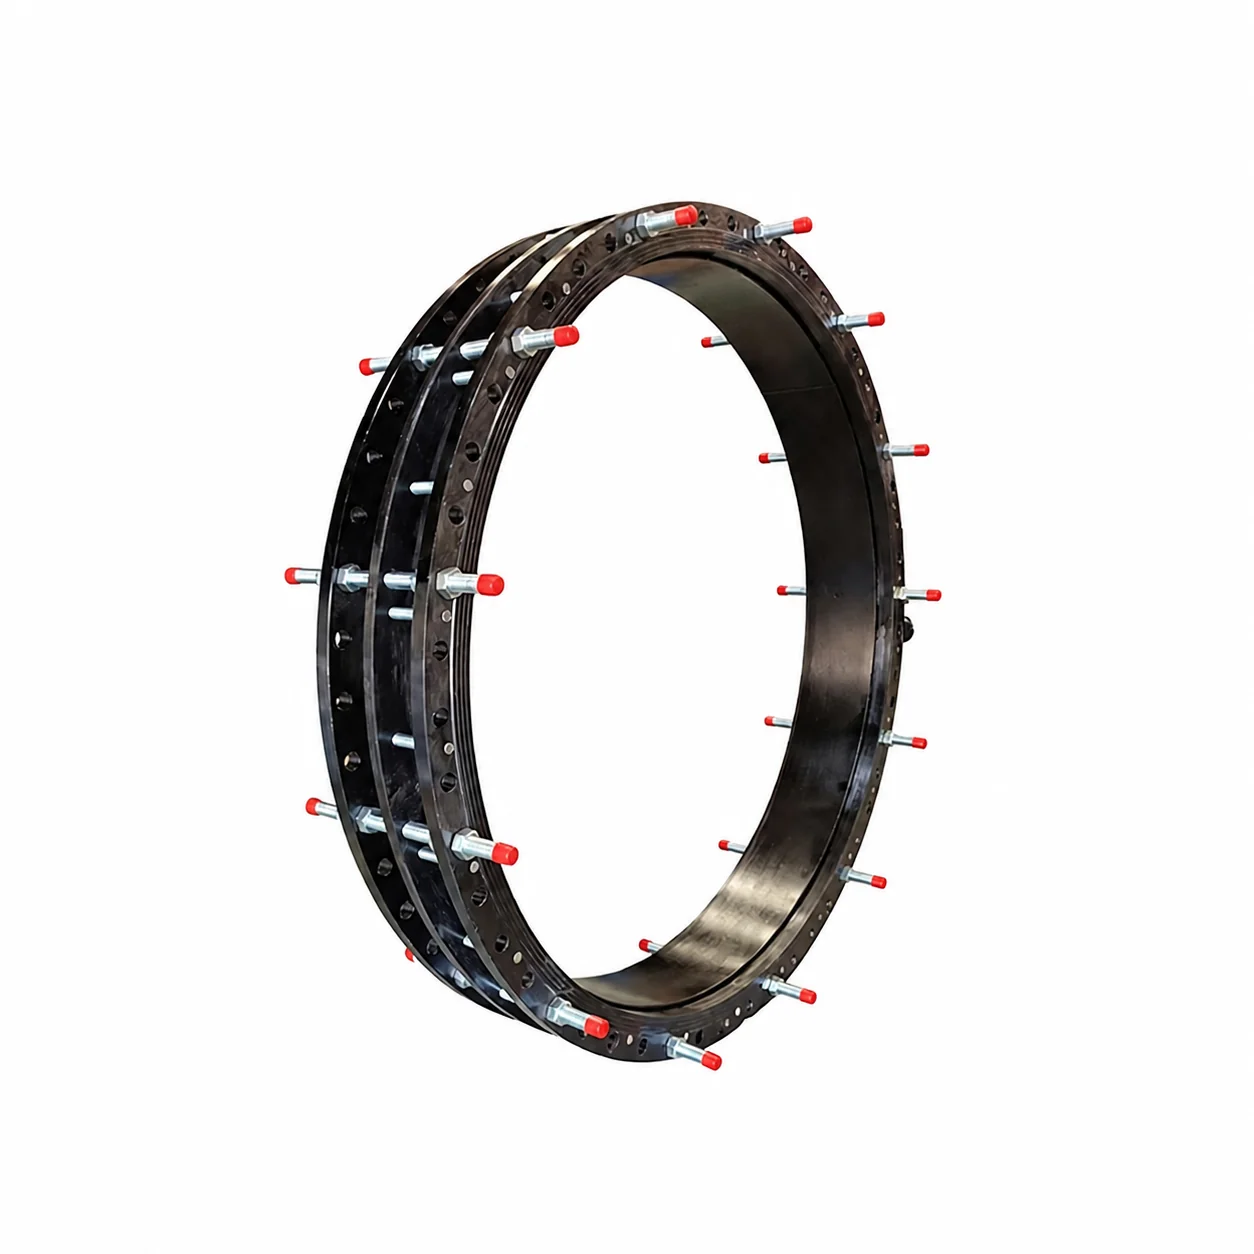
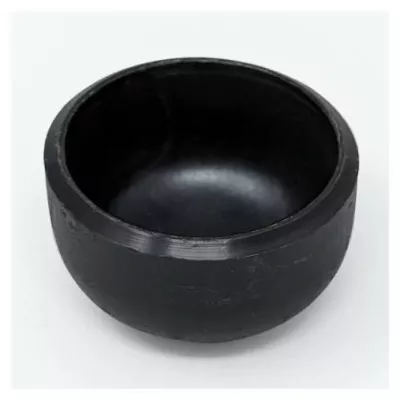
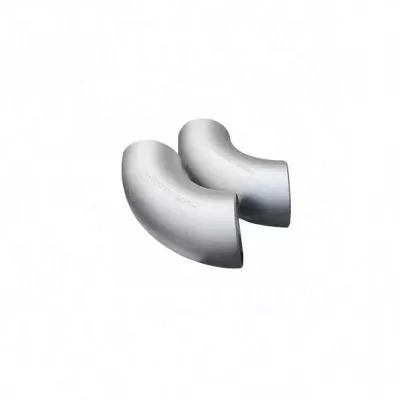
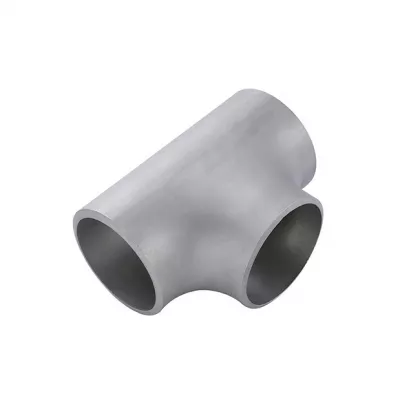
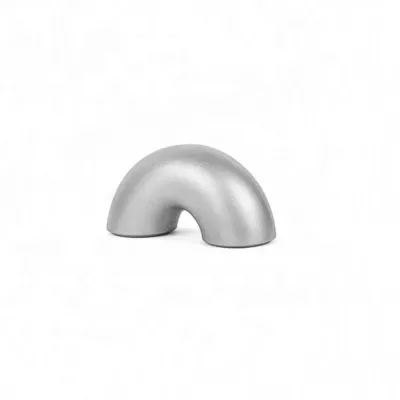
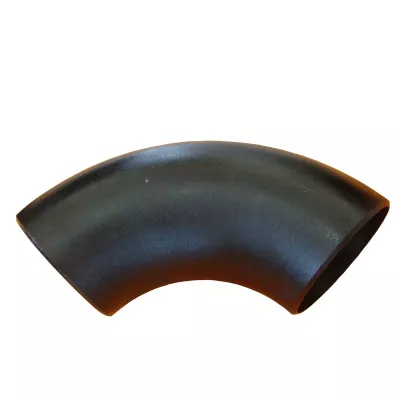
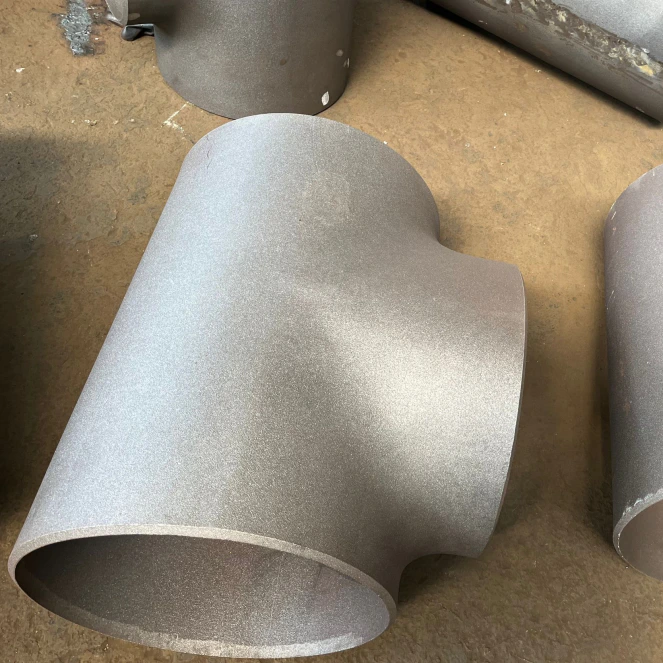
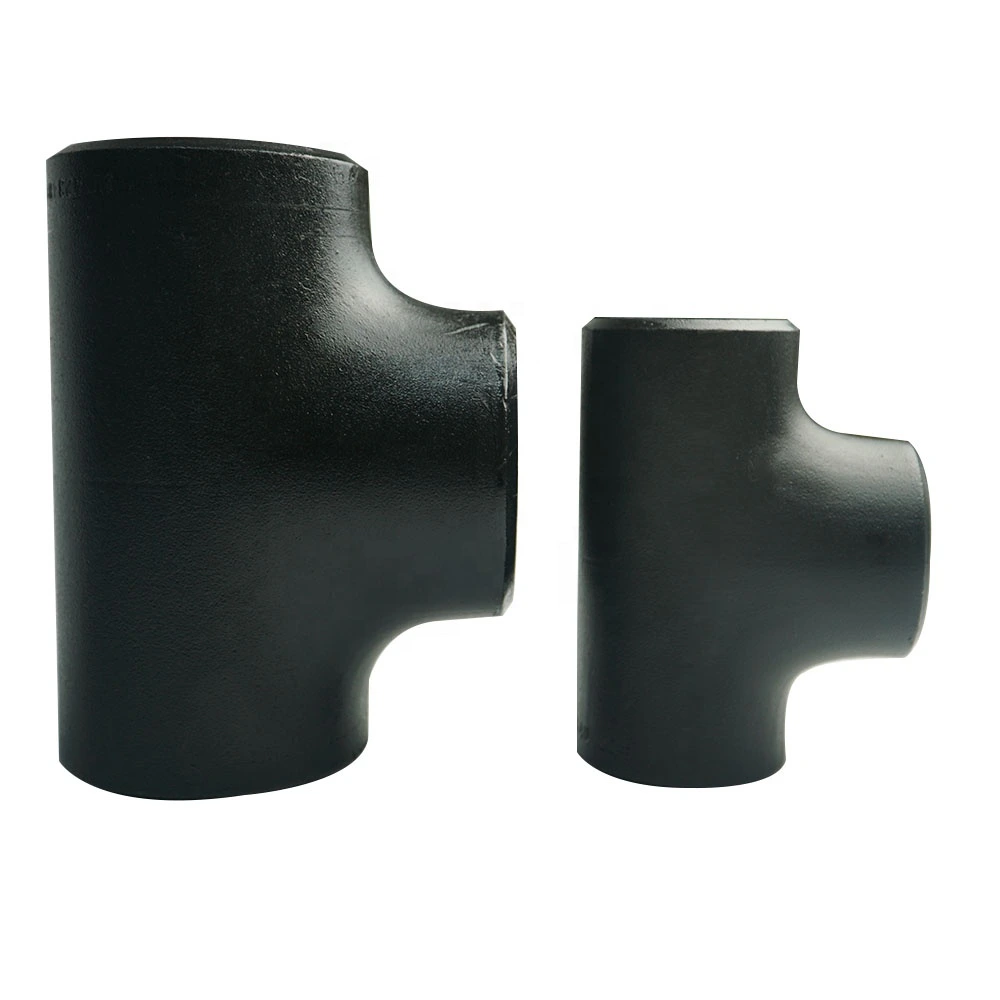
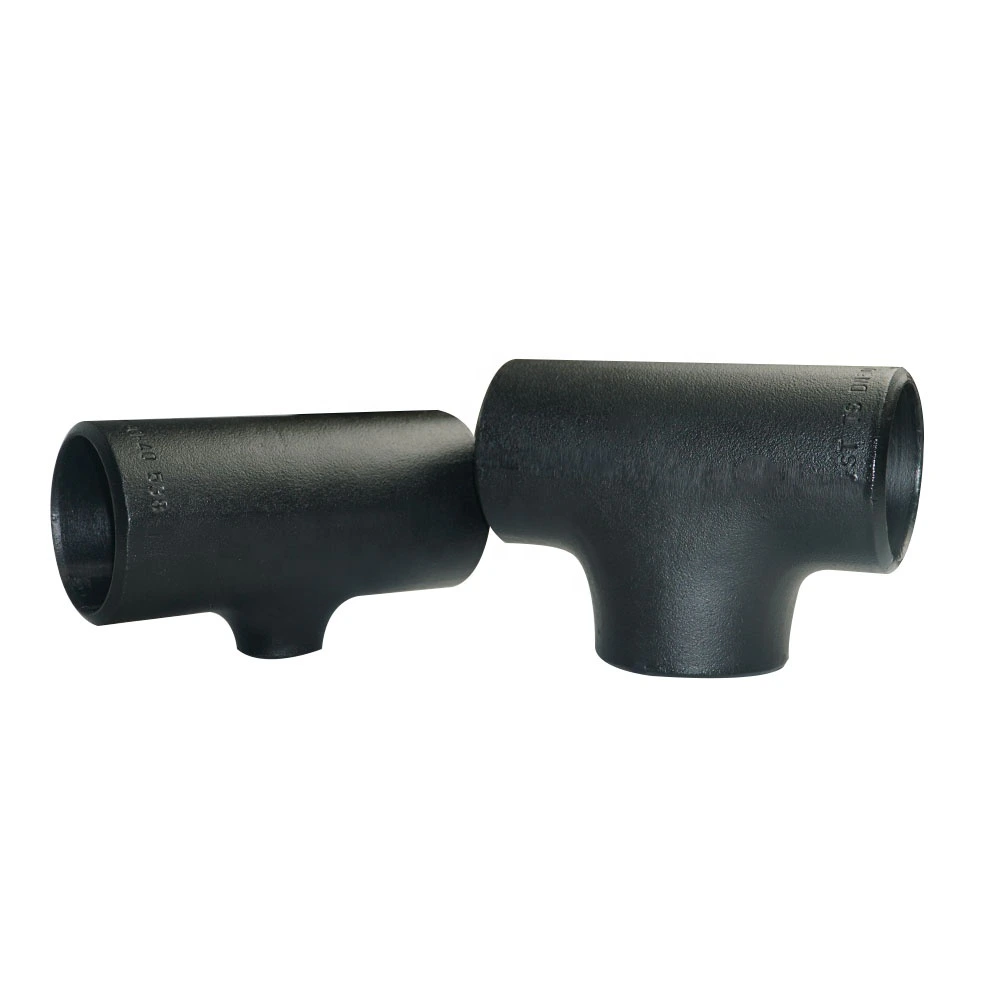
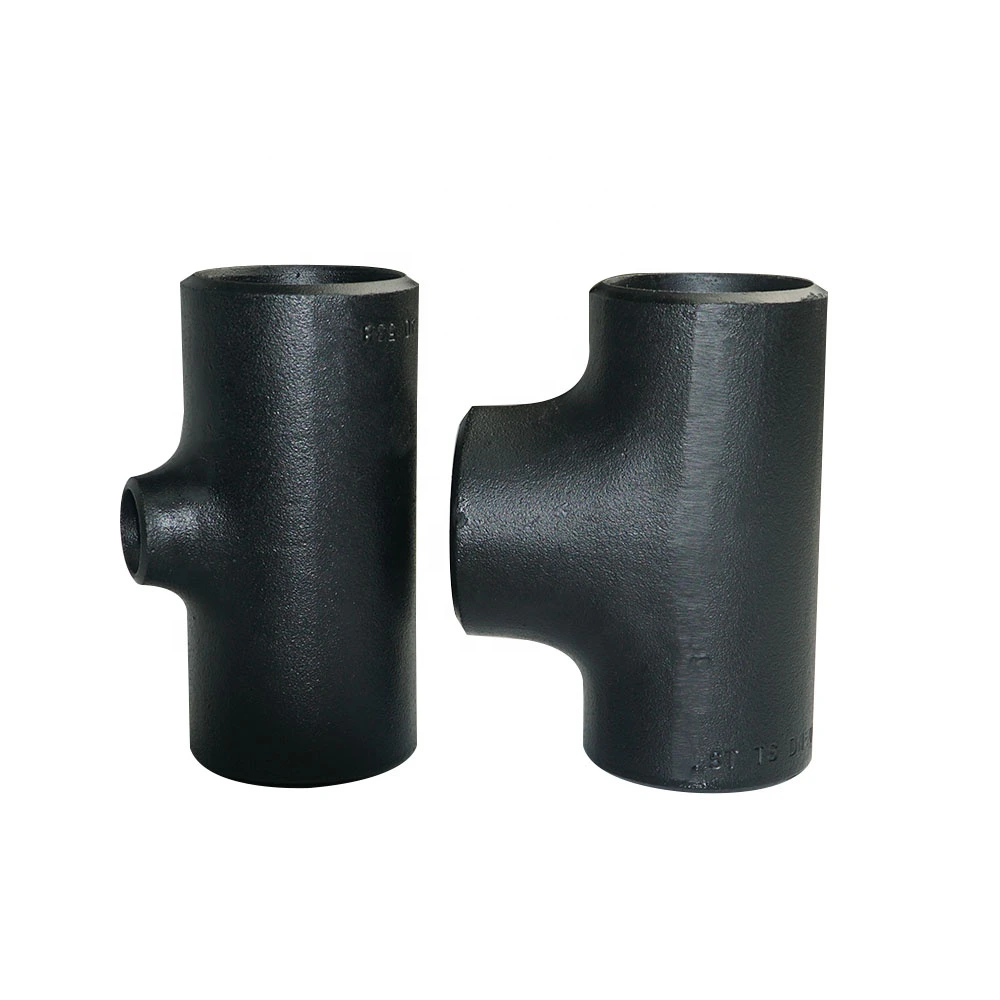
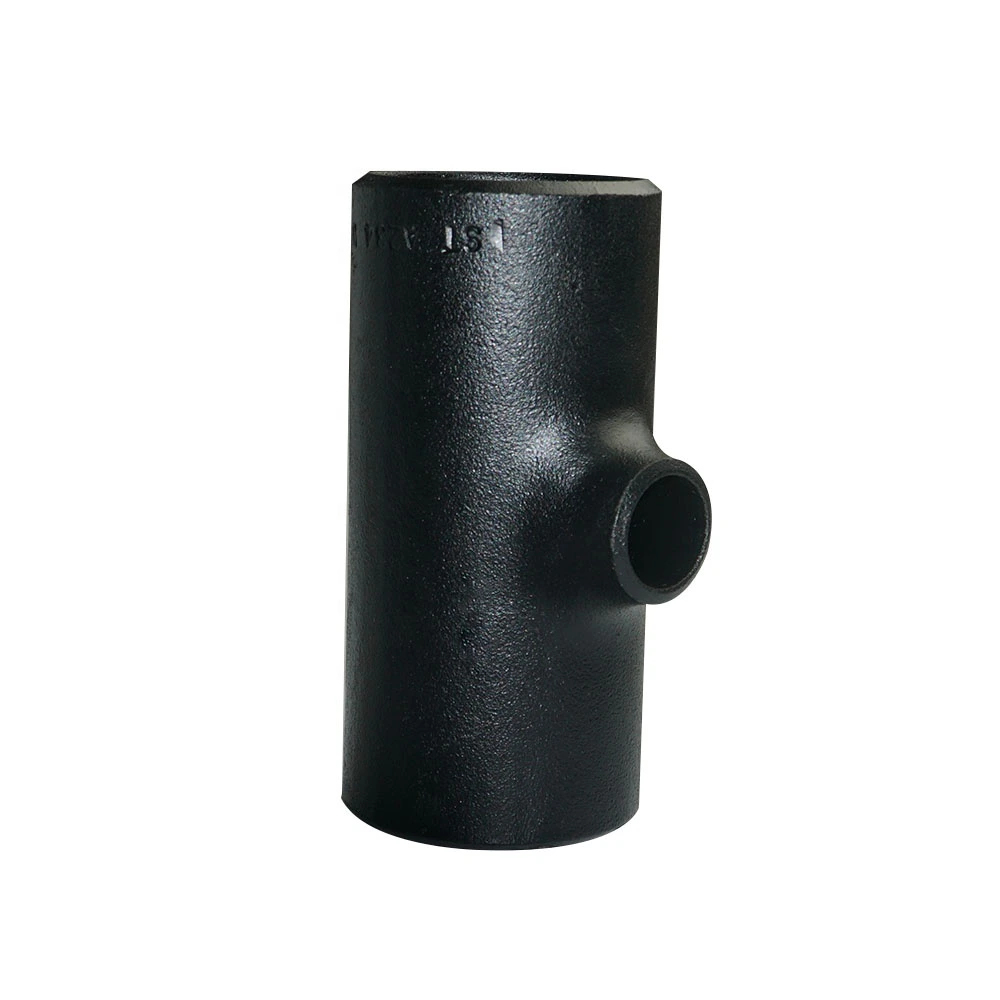
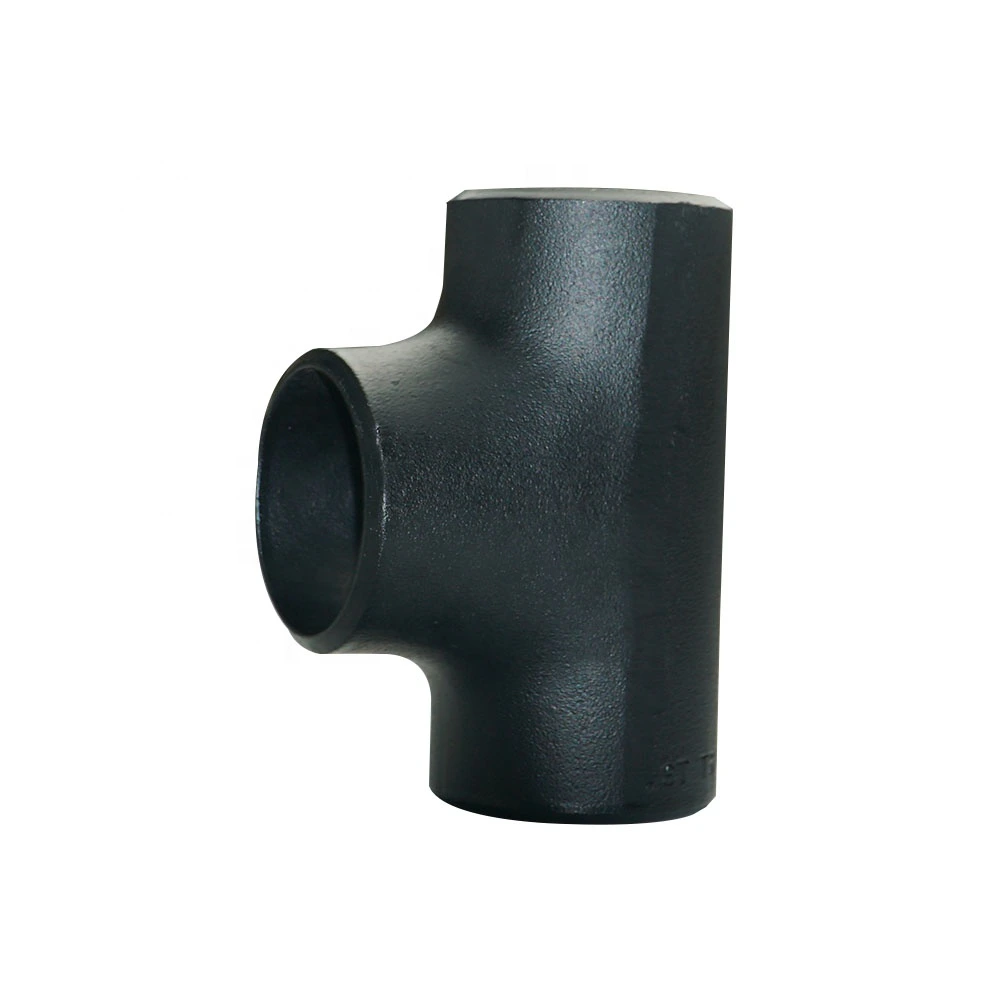
The table says Equal, while both actual variants use Reducer. Reference images show tee forms, including visibly smaller branches, without a reliable scale. Ask the supplier to identify the delivered shape and provide both nominal sizes, bores, outside diameters, center-to-end dimensions, orientation and tolerances.
Clarify the Hexagon field and customized length/height entries on that drawing. Generic mounting-hole and thread fields should not add unsupported interfaces. Identify the governing B16.9 document and edition and confirm its agreed dimensional scope for the requested large-size component.
Specify actual wall and traceable carbon steel
Carbon Steel and a234wpb are the two actual material labels. Confirm the full material specification, grade, condition and accepted traceability documents. No wall schedule or numerical thickness is recorded; provide actual wall and tolerance at each end before matching the fitting to pipework.
Request manufacturing evidence for the table’s FORGED wording and clarify the actual body route. Welding connectivity does not establish seam condition. Agree end preparation, mating pipe fit, alignment, welding and installation inspection. Plain finish and light/dark photographs do not establish protective coating performance.
Confirm the duty of the completed welded connection
The qualitative High Pressure entry gives no numerical capability, with Pipe Class and Application listed as Other. Specify medium, pressure, temperature, cycling, loads and compatibility. Obtain fitting/joint acceptance and agree material/manufacturing/dimensional records, marking, individual-size supply, quotation scope and warranty/OEM terms.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.