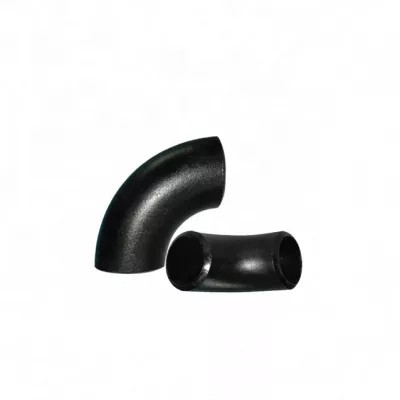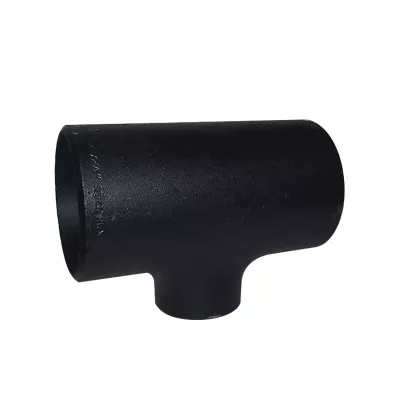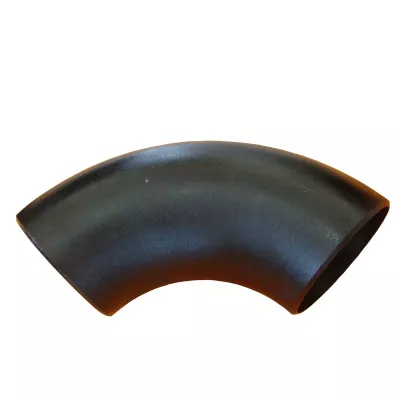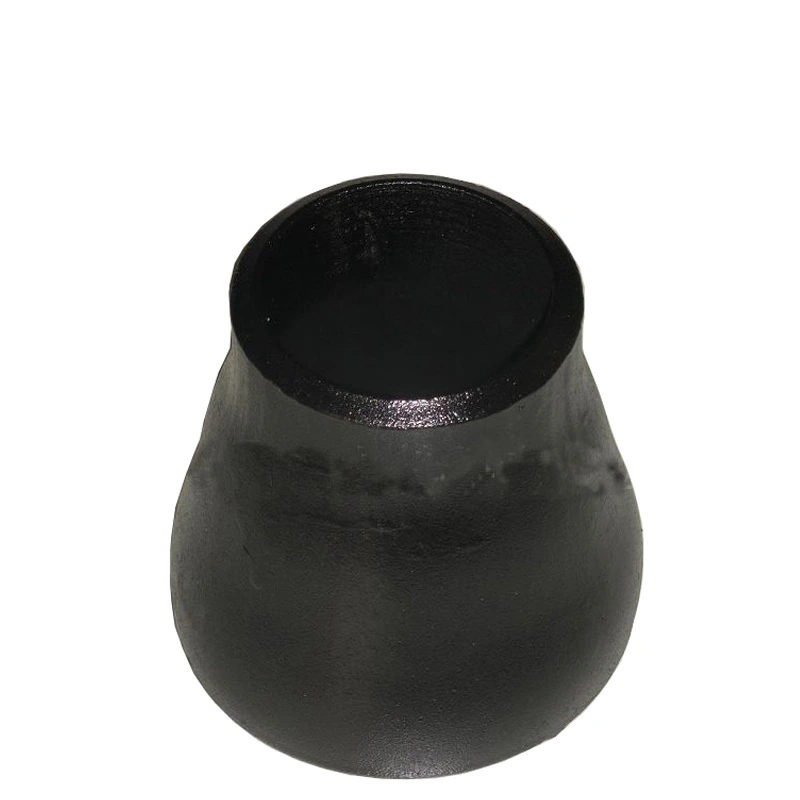
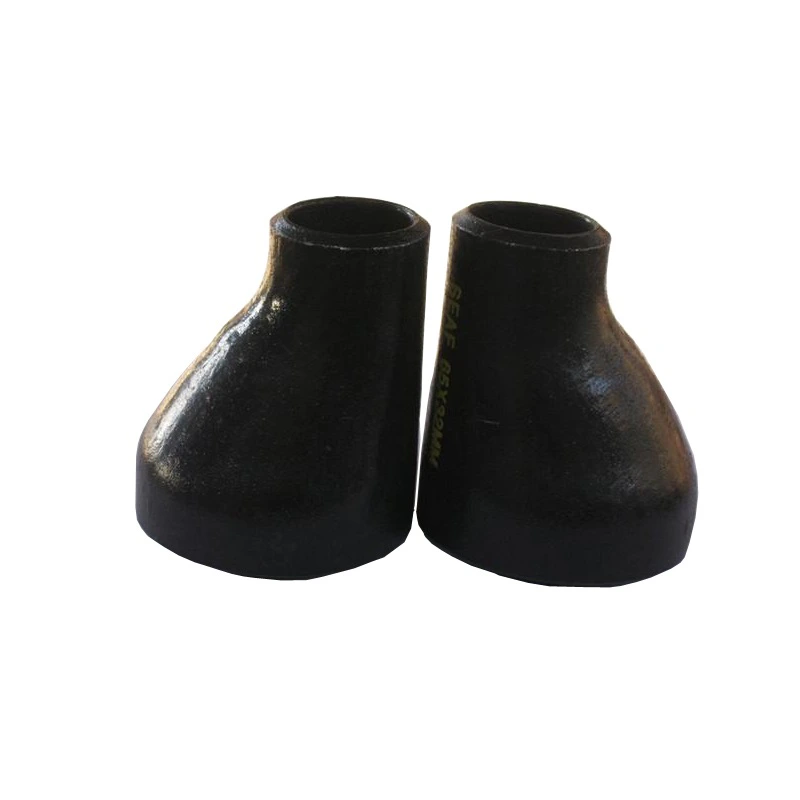
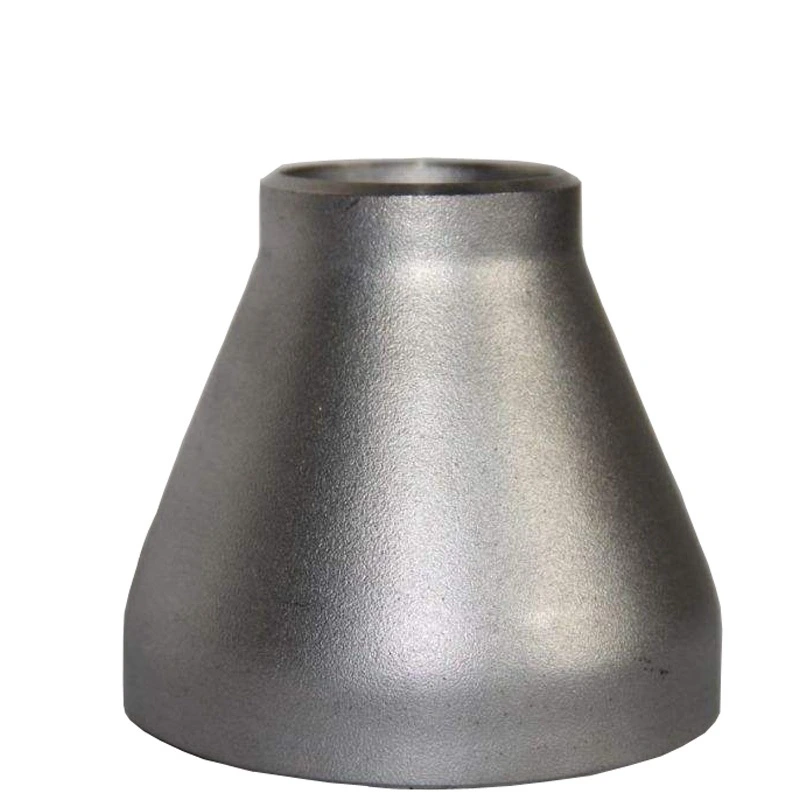
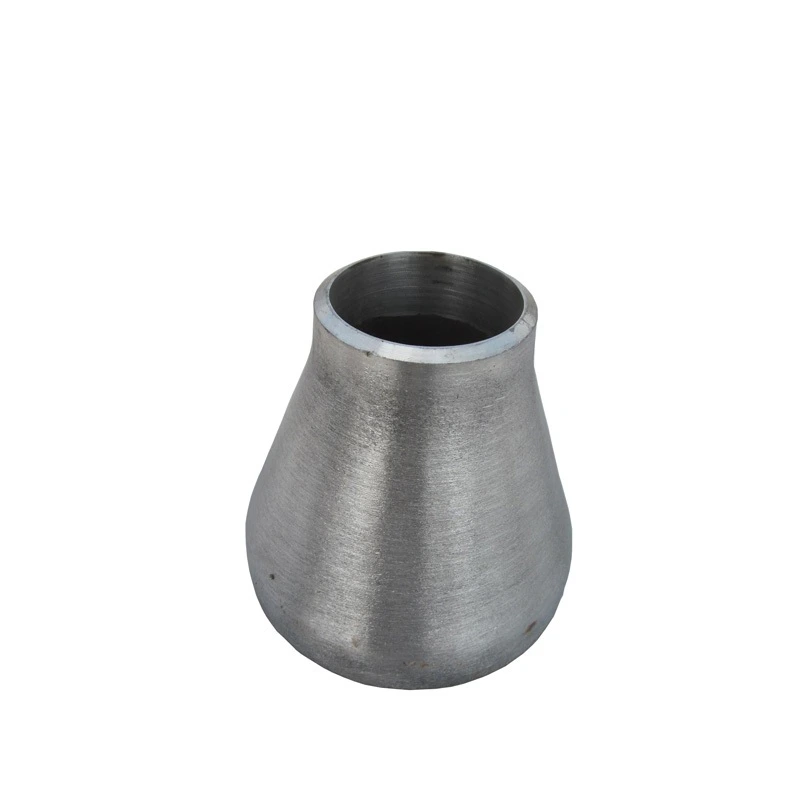
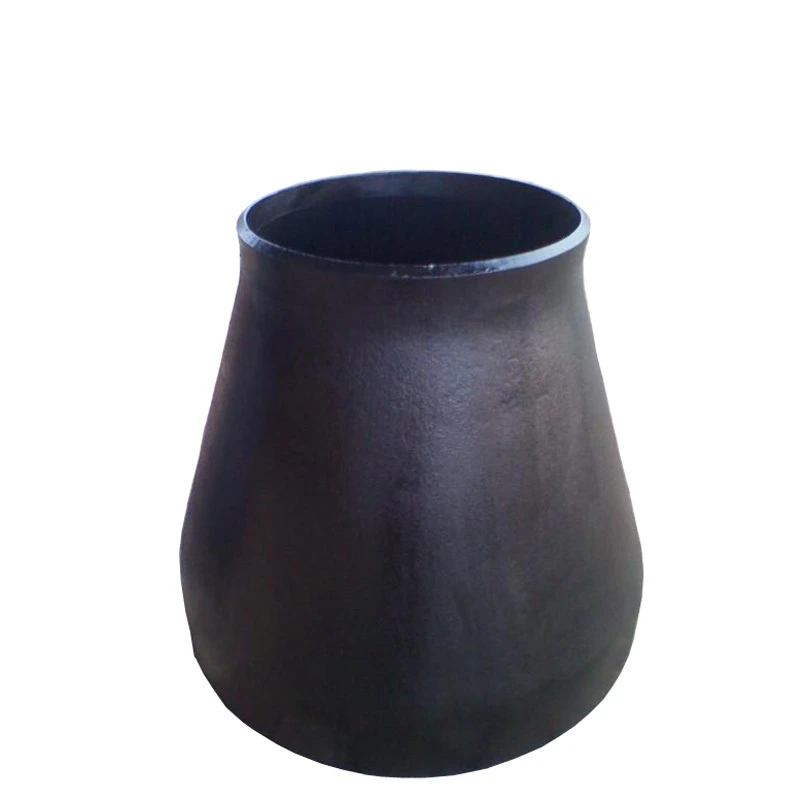
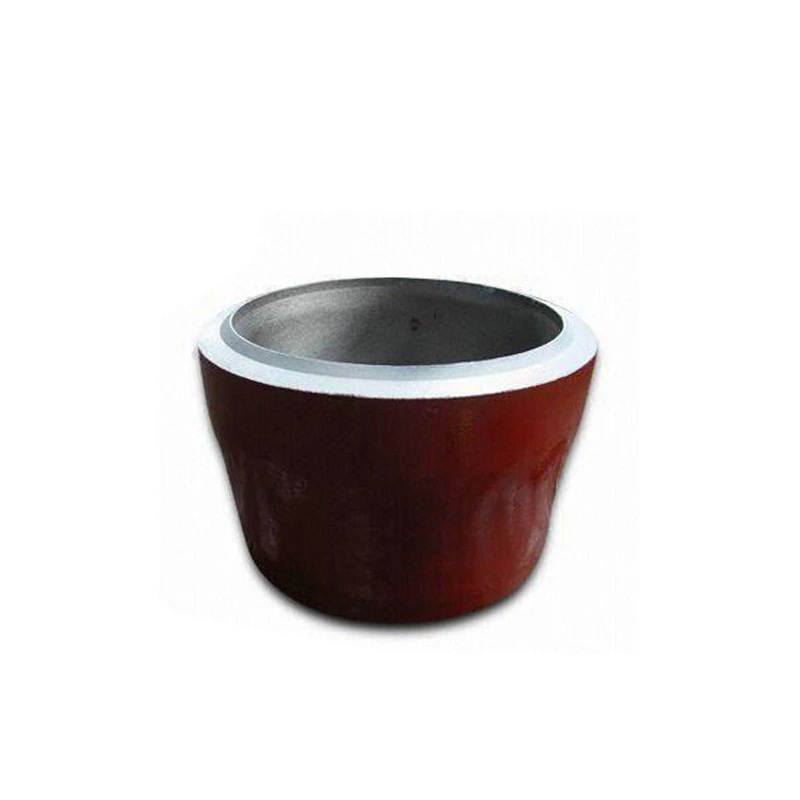
ANSI B16.9 Stainless Steel Eccentric & Concentric Butt Weld Reducer
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty1 yearcustomized supportOEM, ODM, OBM
-
TechnicForgedConnectivityWelding
-
shapeEqualhead codeHexagon
-
Surface TreatmentPaintingMounting hole diameter0.2 in
-
Pipe Class150
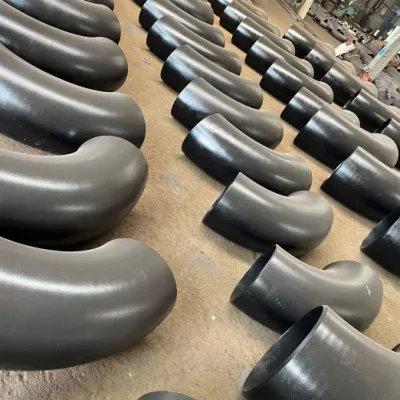
This ANSI B16.9 stainless steel butt-weld reducer enquiry covers eccentric and concentric transition requests. Choose the required centreline arrangement, then confirm actual unequal end dimensions, selected material and weld preparation for the specific pipe transition.
Select alignment with a complete large-by-small drawing
An eccentric request needs a defined offset and installation orientation; a concentric request needs the specified centreline relationship. Neither arrangement can be assigned to the selected component from gallery examples alone. Obtain large and small nominal sizes, outside diameters, both-end walls, end-to-end length and dimensional tolerances.
The five size labels of 10, 12, 14, 50 and 30 mm do not provide a complete reducing pair. Confirm actual reduction and nominal-size mapping on the accepted drawing. Mounting-hole diameter 0.2 in does not establish pipe bore or either end size.
Separate material selection from weld-end acceptance
Stainless Steel, Alloy and Carbon Steel are distinct choices. Alloy does not identify a grade, and no specific material specification is established here. Request the selected specification, grade and heat-traceable certificate. Confirm the applicable B16.9 document and edition associated with the ANSI enquiry wording.
Define actual end preparation, bevel, matching pipe dimensions and wall thickness at both ends, together with welding and inspection requirements. Forged requires selected manufacturing records; it does not establish a seamless route. Photographed components and markings cannot qualify the supplied grade, schedule or weld-end dimensions.
Class 150 and painted-surface requirements
Pipe Class 150 alone does not establish a numerical working pressure. Assess material, wall, welded joint, medium, temperature and governing design requirements for the actual service. Define paint system, coating extent, exposure and inspection criteria rather than assuming a corrosion rating or weld-ready finish. Include chosen alignment, full size pair, grade certificate, weld drawing, manufacturing acceptance and operating conditions with the enquiry.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.