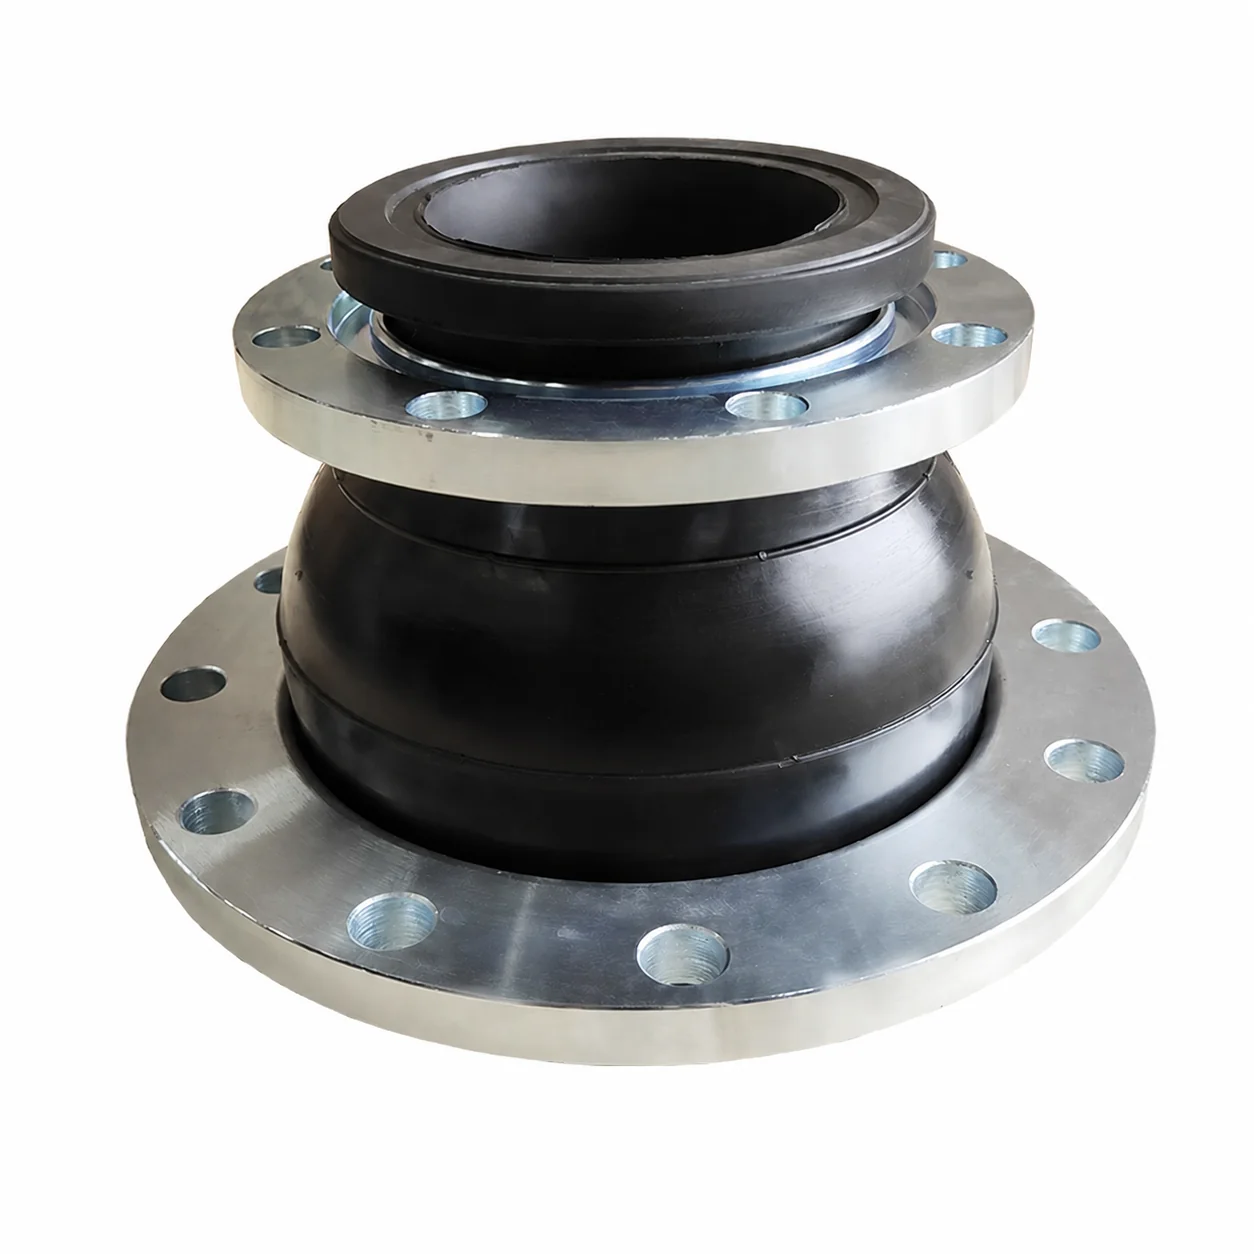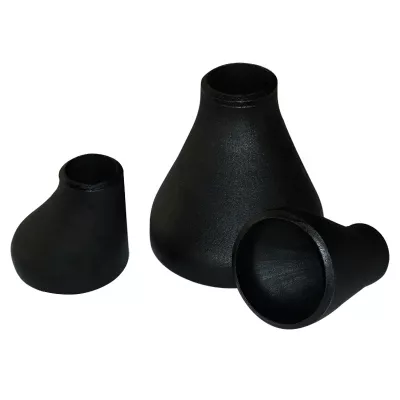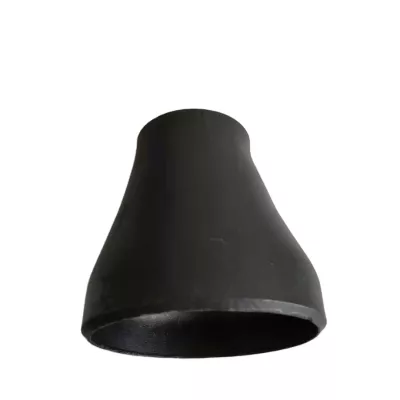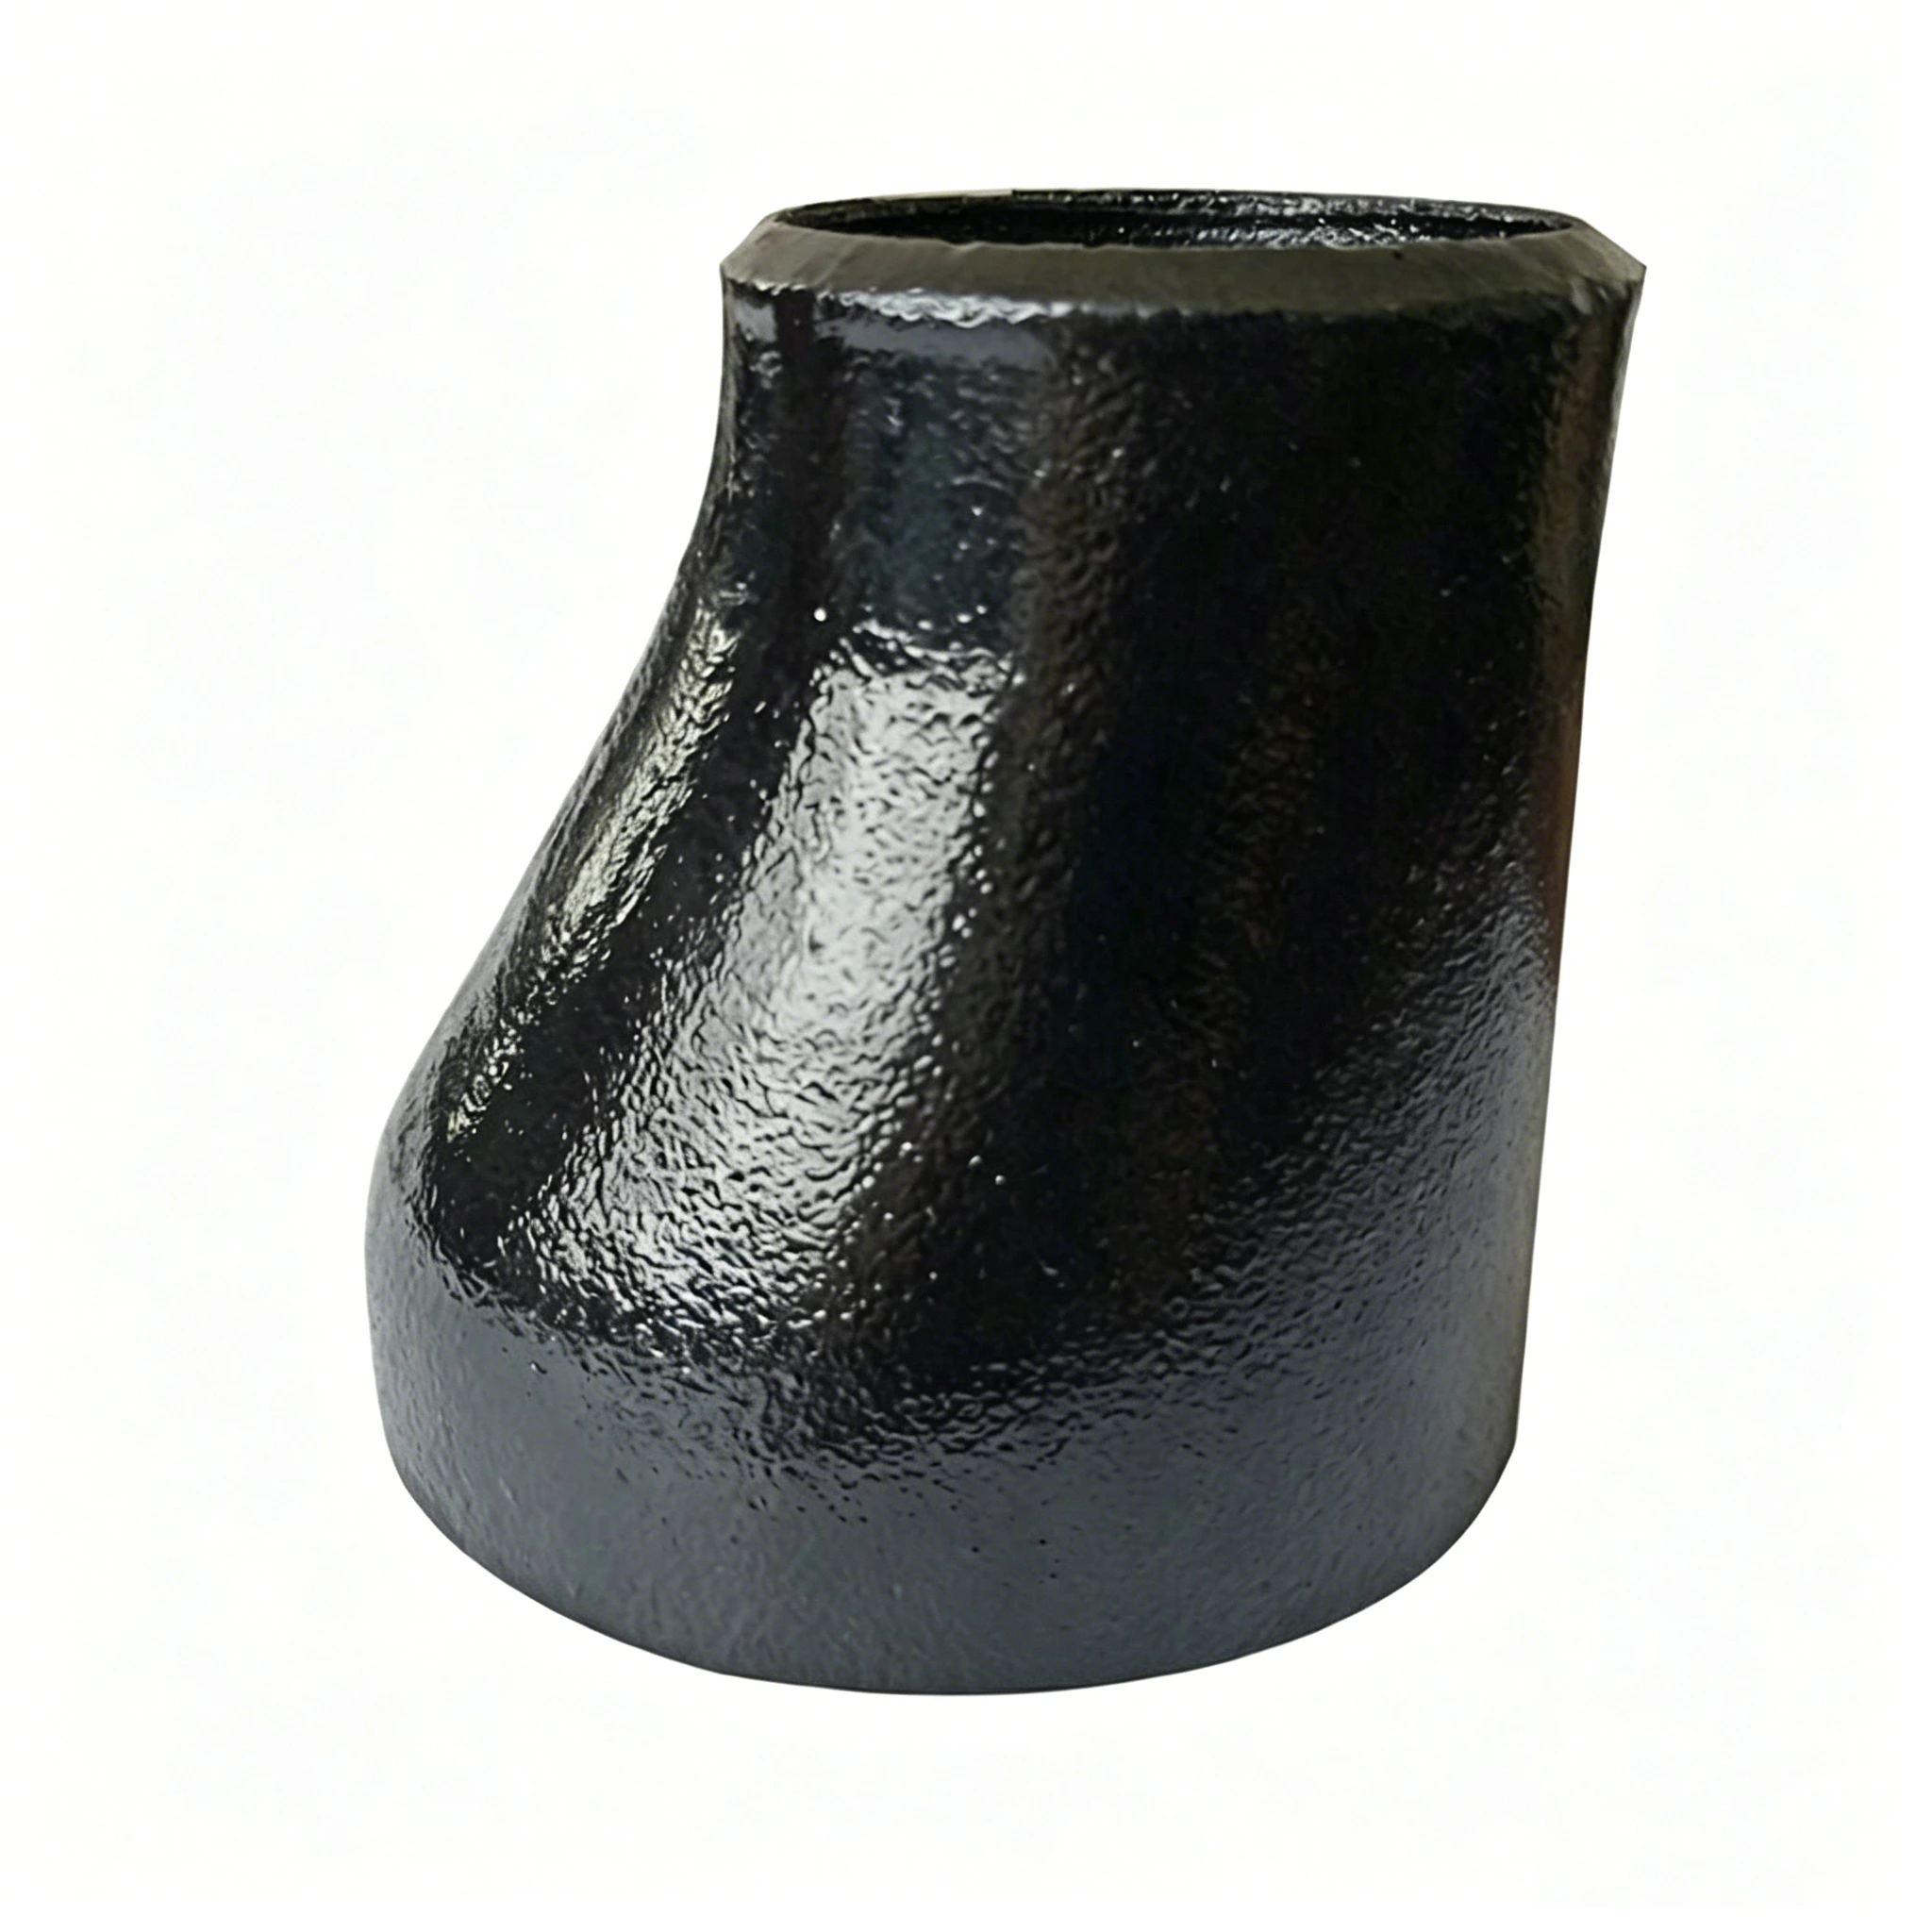
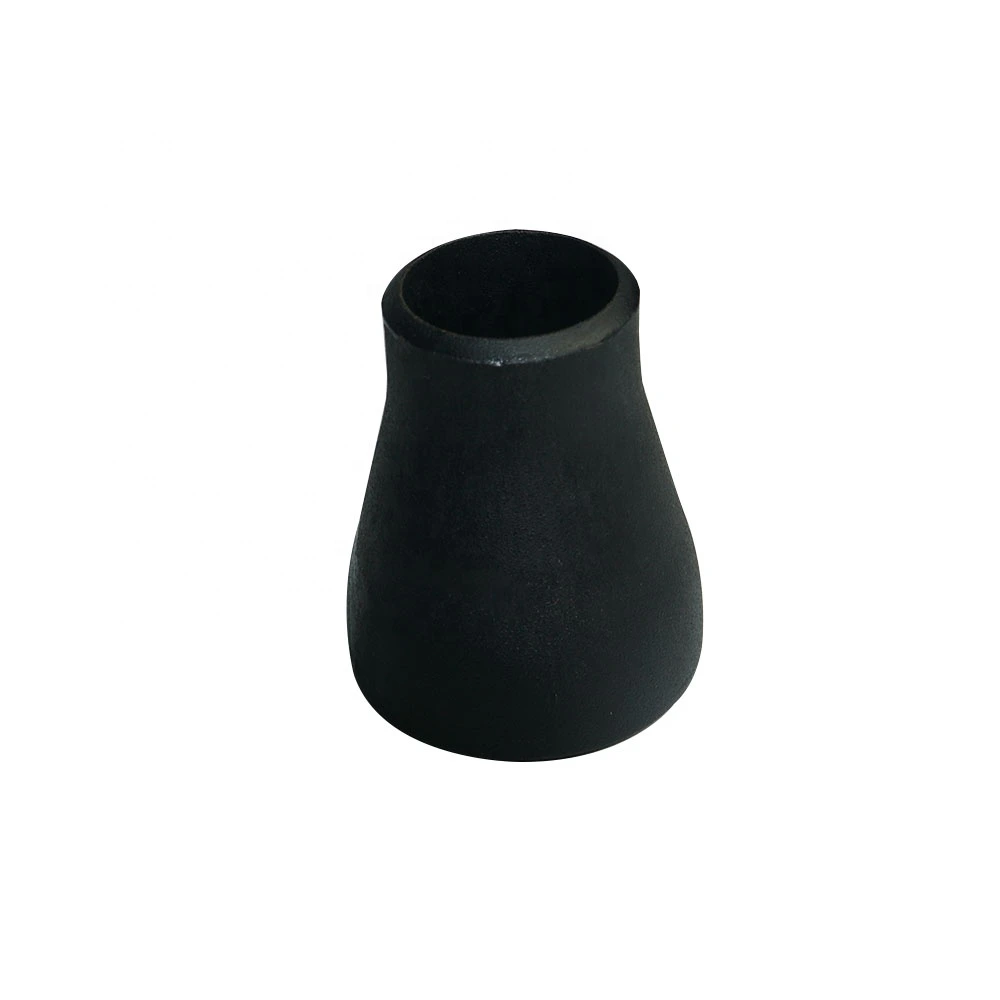
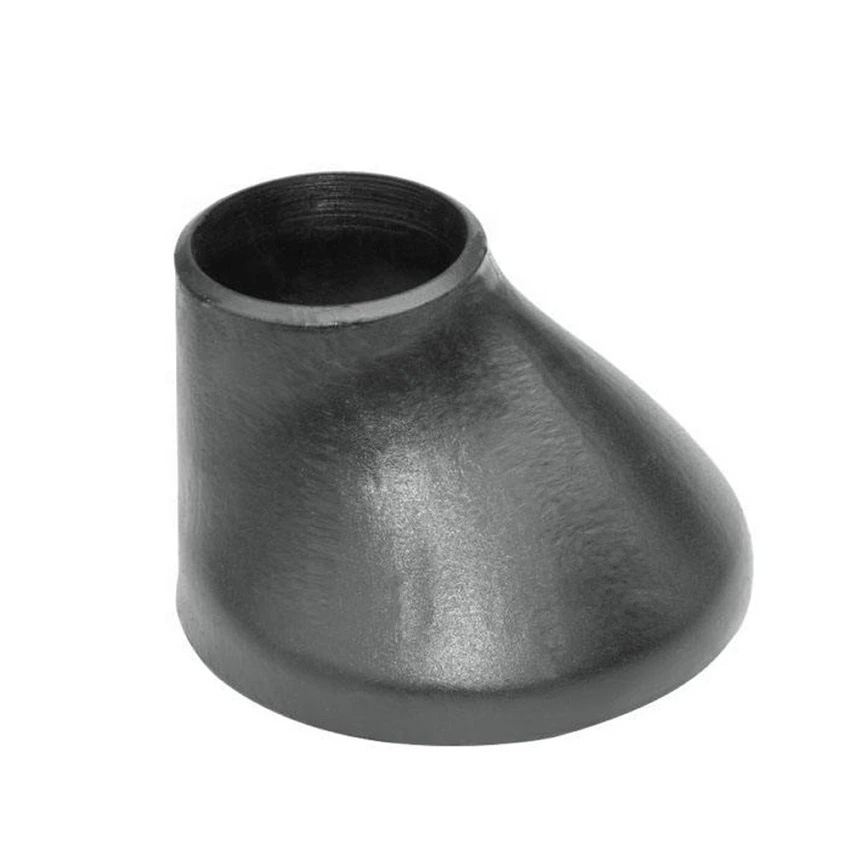
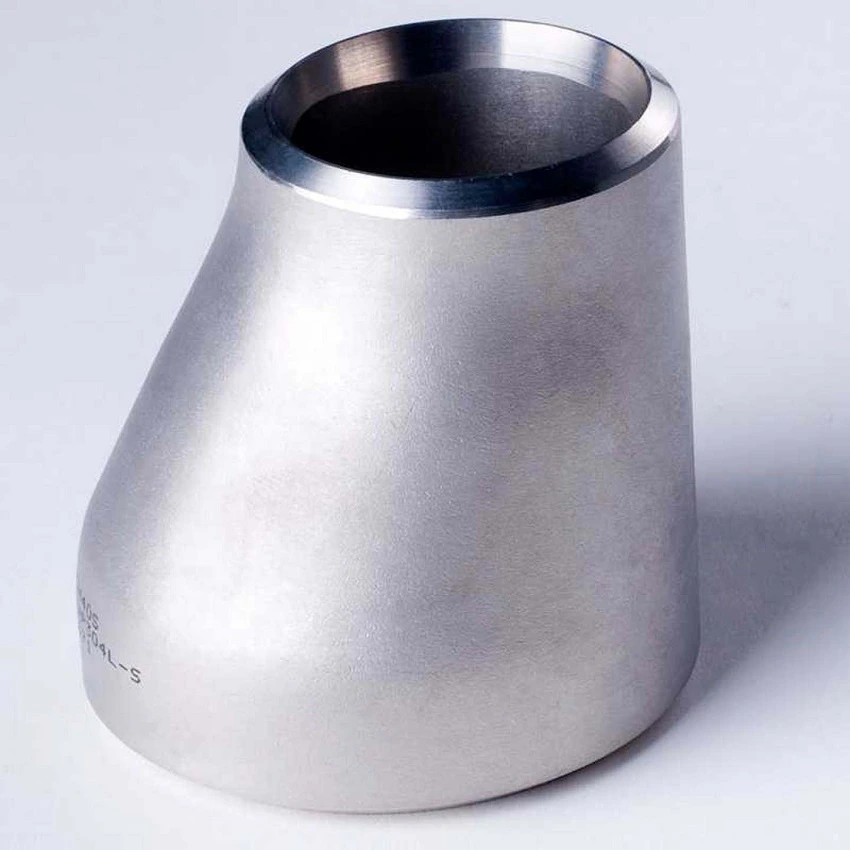
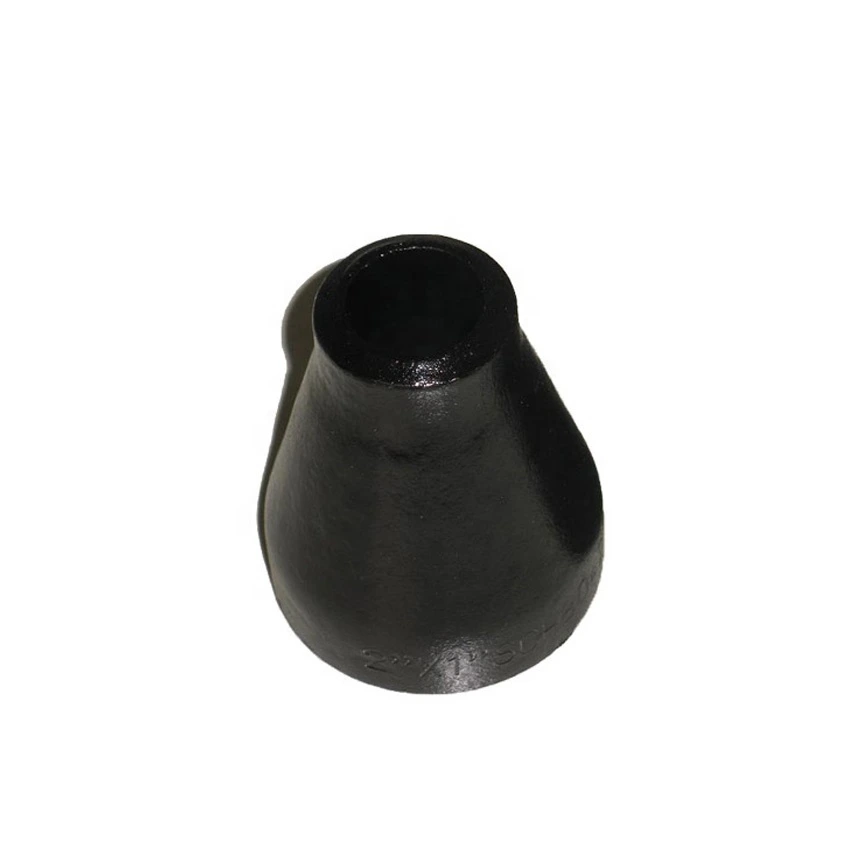
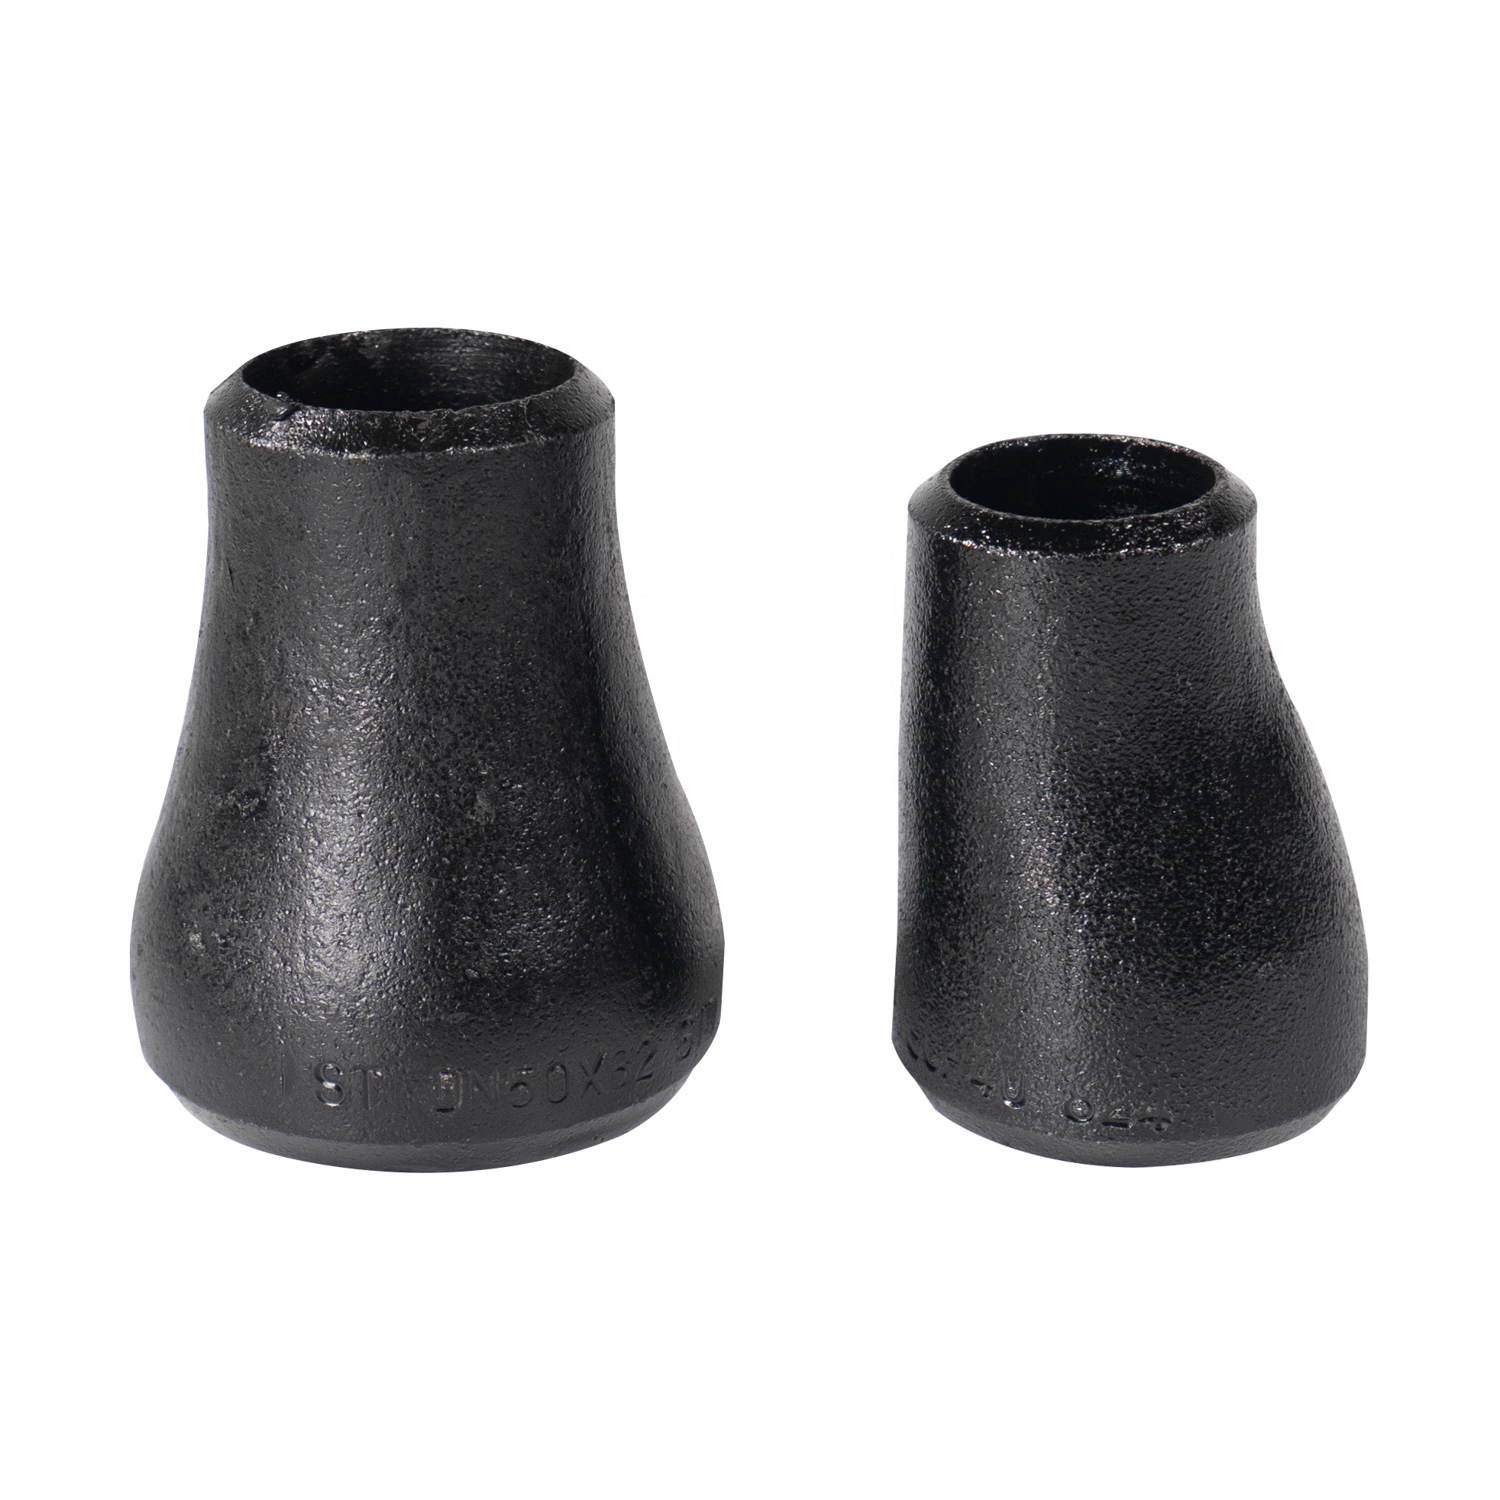
Seamless Carbon Steel Eccentric and Concentric Reducer
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty3 Yearscustomized supportOEM, odm
-
TechnicForgedConnectivityWelding
-
shapeReducinghead codeOther
-
Overall Length1/2"-4"Height1/2"-4"
-
Surface TreatmentPolishedPressureLow Pressure
-
System of MeasurementMetricMounting hole diameter1/2"-4"
-
Pipe FeaturesCorrosion-resistantPipe ClassOther
-
ApplicationOtherThread TypesNPT
This seamless carbon steel reducer listing describes eccentric and concentric configurations with DN150, DN125 and DN100 choices. Each actual variant contains one nominal label, not a complete reducing pair. Confirm the selected construction and manufacturing records before specifying an individual item.
Document the seamless and forged manufacturing scope
Request the full carbon steel material specification, grade, condition, traceability and certificates. Obtain records supporting both seamless and forged wording for the actual component. The general ASME reference lacks a document number, so agree the governing document and edition without automatically adding B16.9.
Factory Direct is title wording rather than proof of factory ownership. Confirm the actual quotation and supply arrangement. Define polished surfaces and inspection requirements, and request corrosion compatibility evidence instead of treating a generic corrosion-resistant feature as a coating or service guarantee.
Allocate each nominal choice to a complete reducer
Identify larger and smaller ends, eccentric or concentric profile, outside diameters, bores, wall thickness and transition dimensions. Agree offset/orientation where relevant and the required tolerances. Confirm availability of the chosen pair; individual DN labels do not establish every reducing combination.
Length, height and mounting-hole diameter repeat half-inch-to4-inch ranges that need selected drawing allocation. They do not provide measured geometry or establish holes. Resolve Welding and NPT entries through an actual end drawing, mating pipe details and agreed preparation rather than assuming a combined connection.
Specify the operating envelope and inspection scope
Low Pressure and Other class leave numerical limits unconfirmed. State medium, pressure, temperature, cycling, loads and corrosion environment. Obtain complete system acceptance, then agree joining procedure, alignment, inspection, marking, required records and quotation scope for the individual configuration.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.