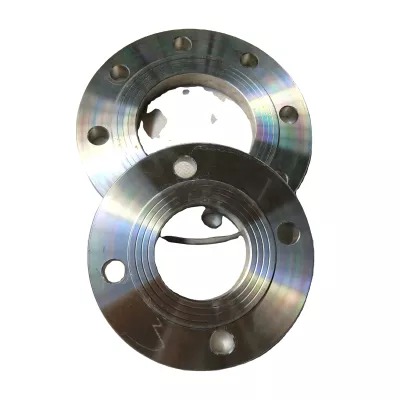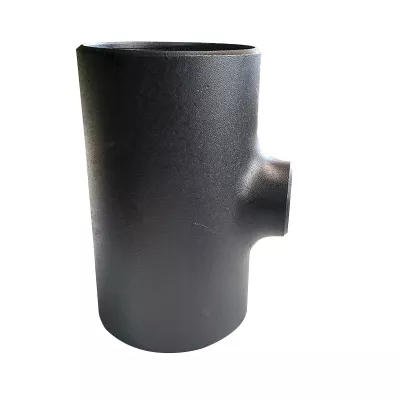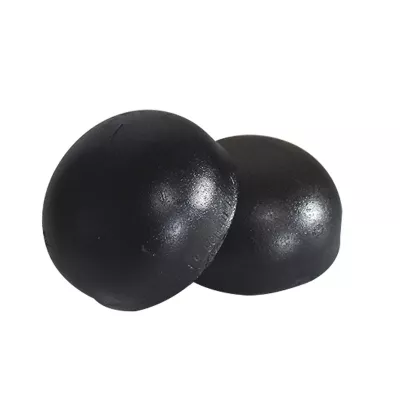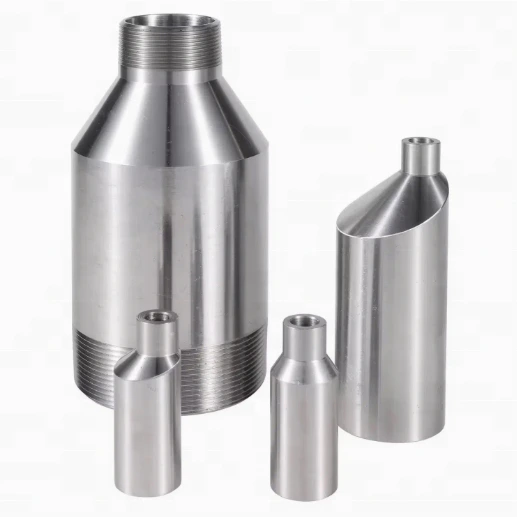
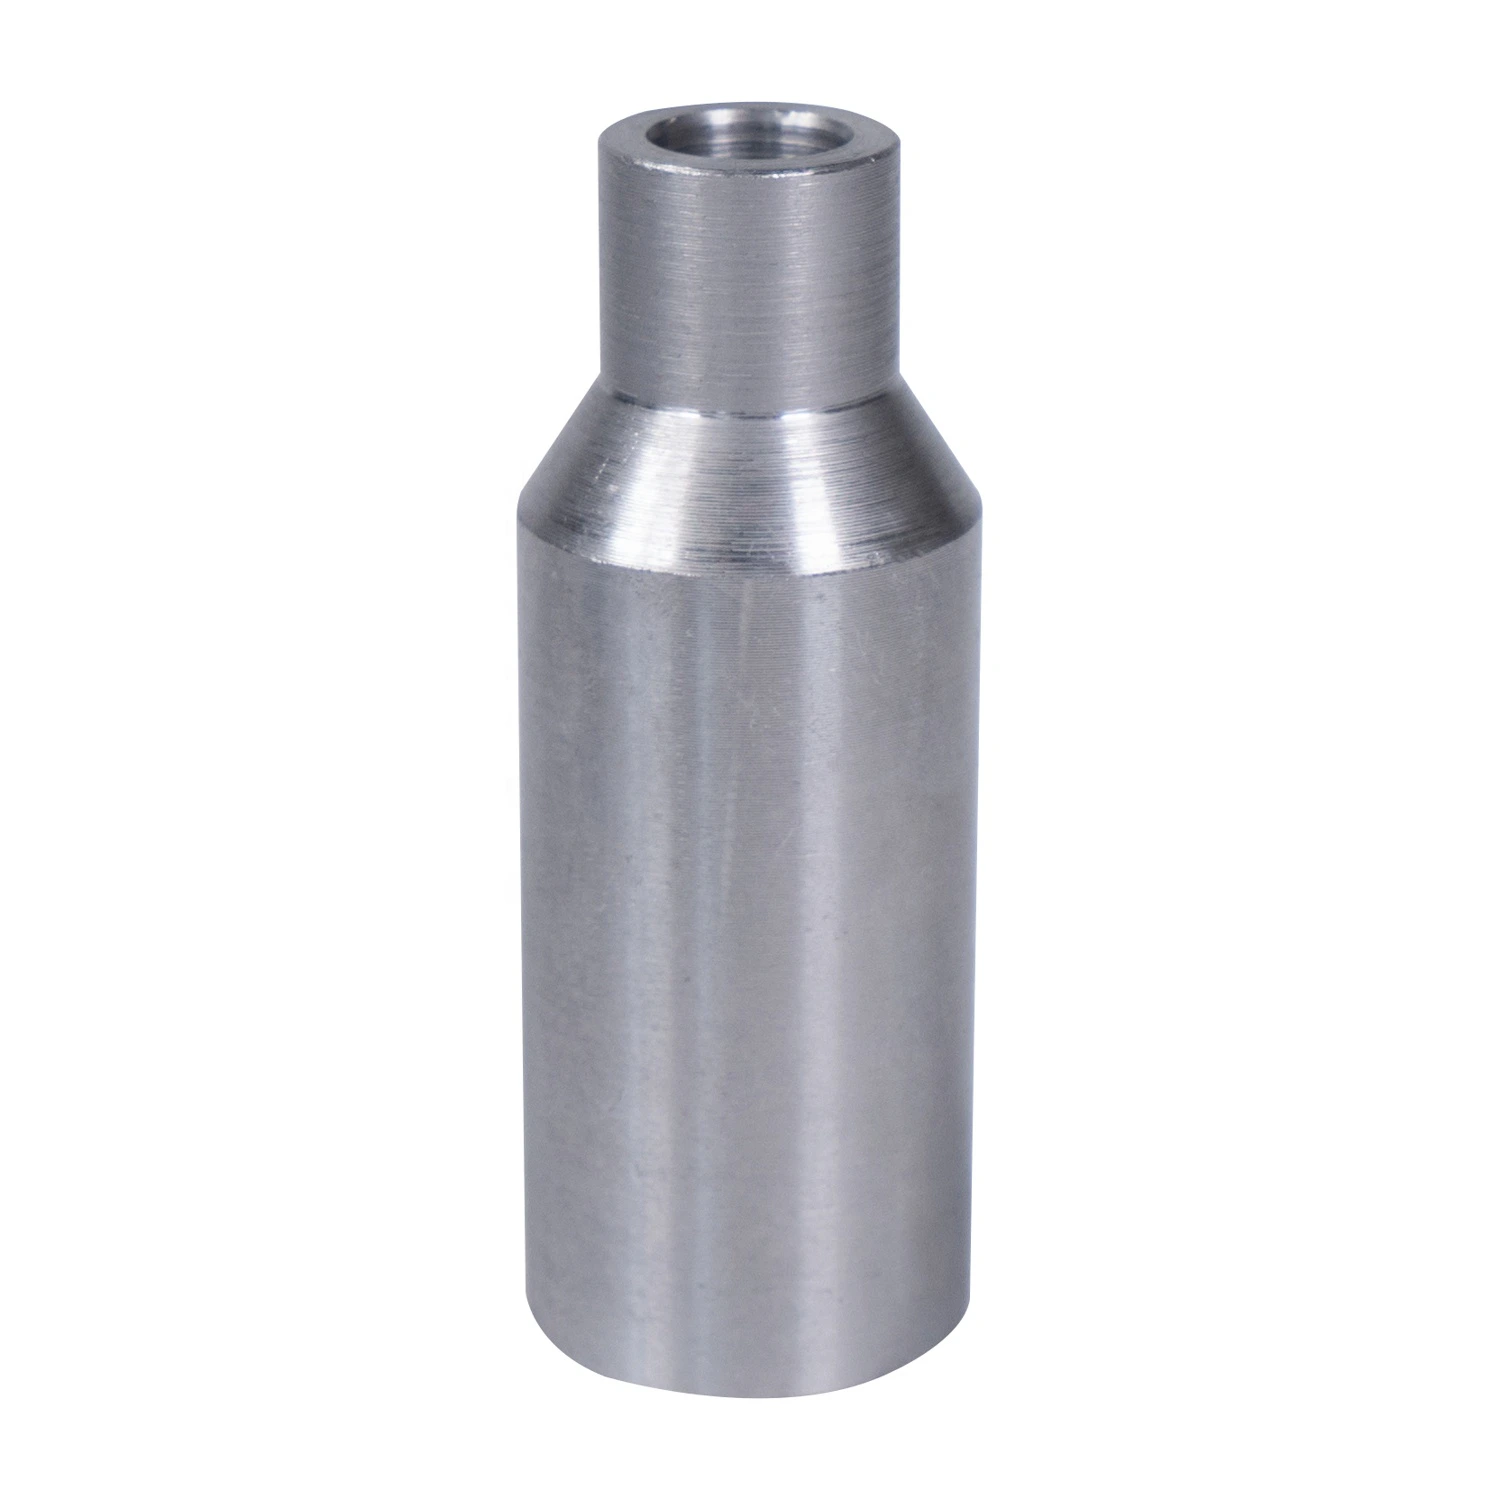
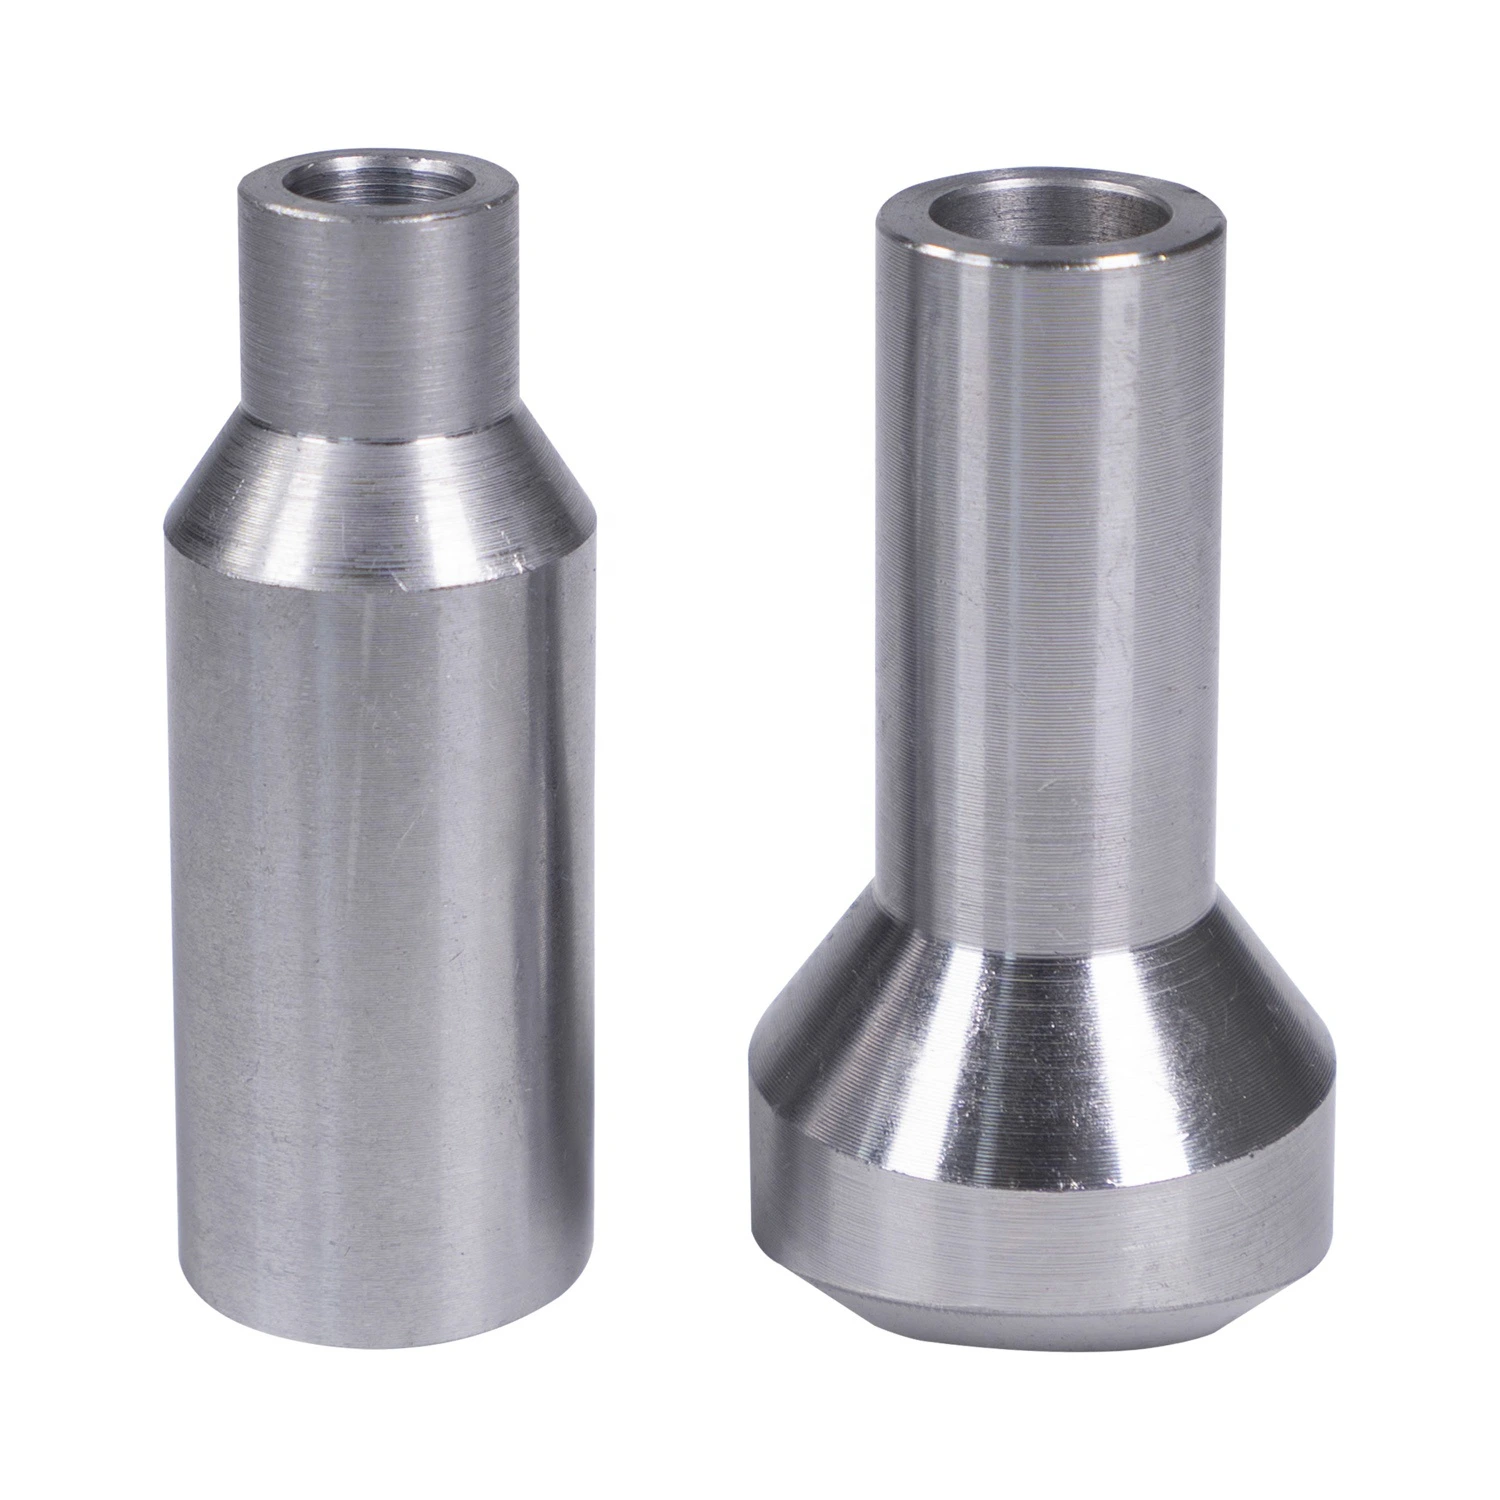
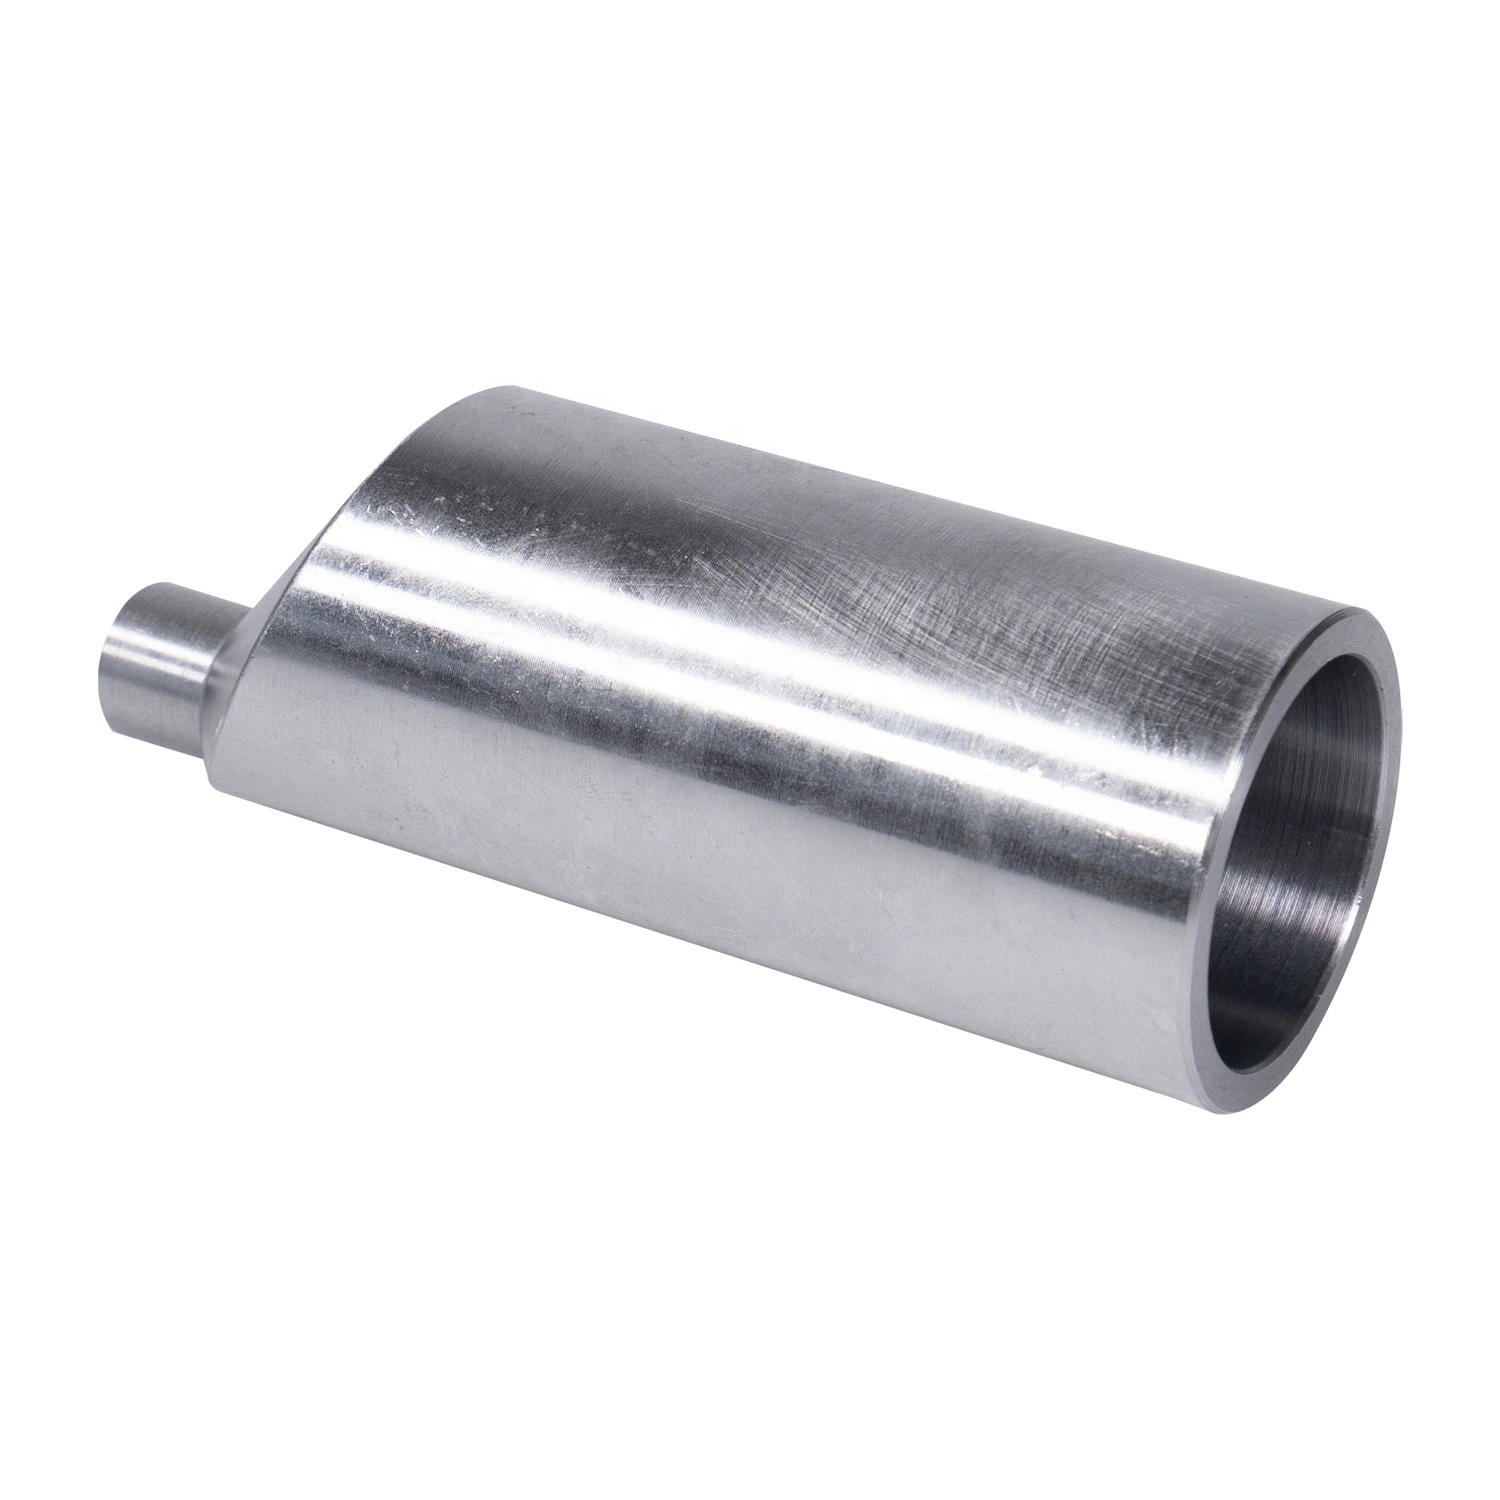
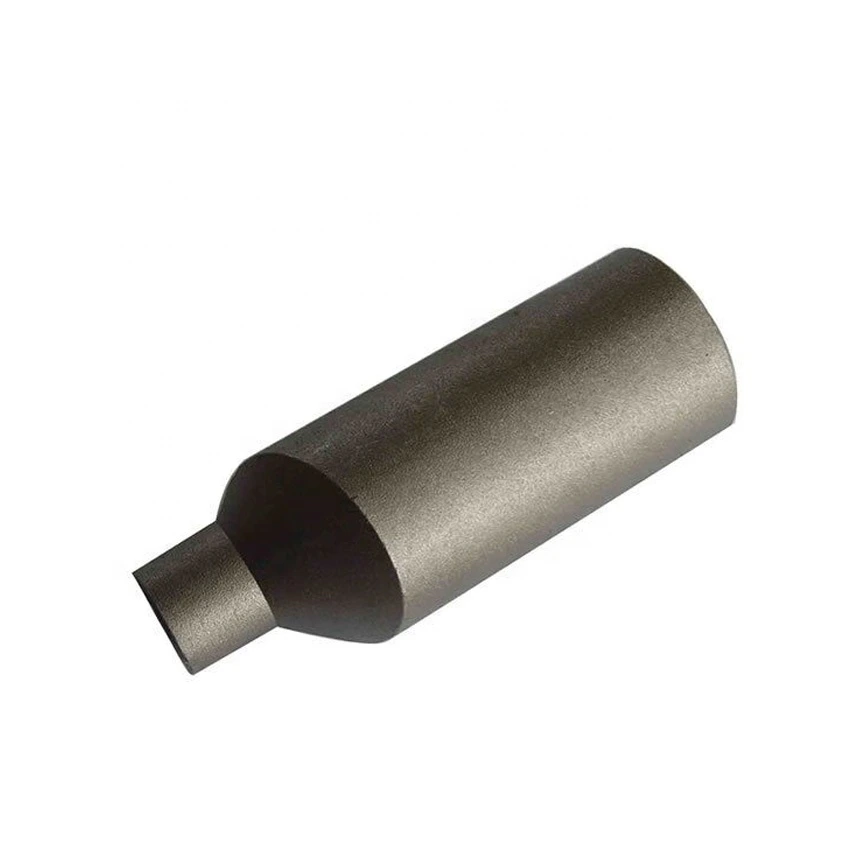
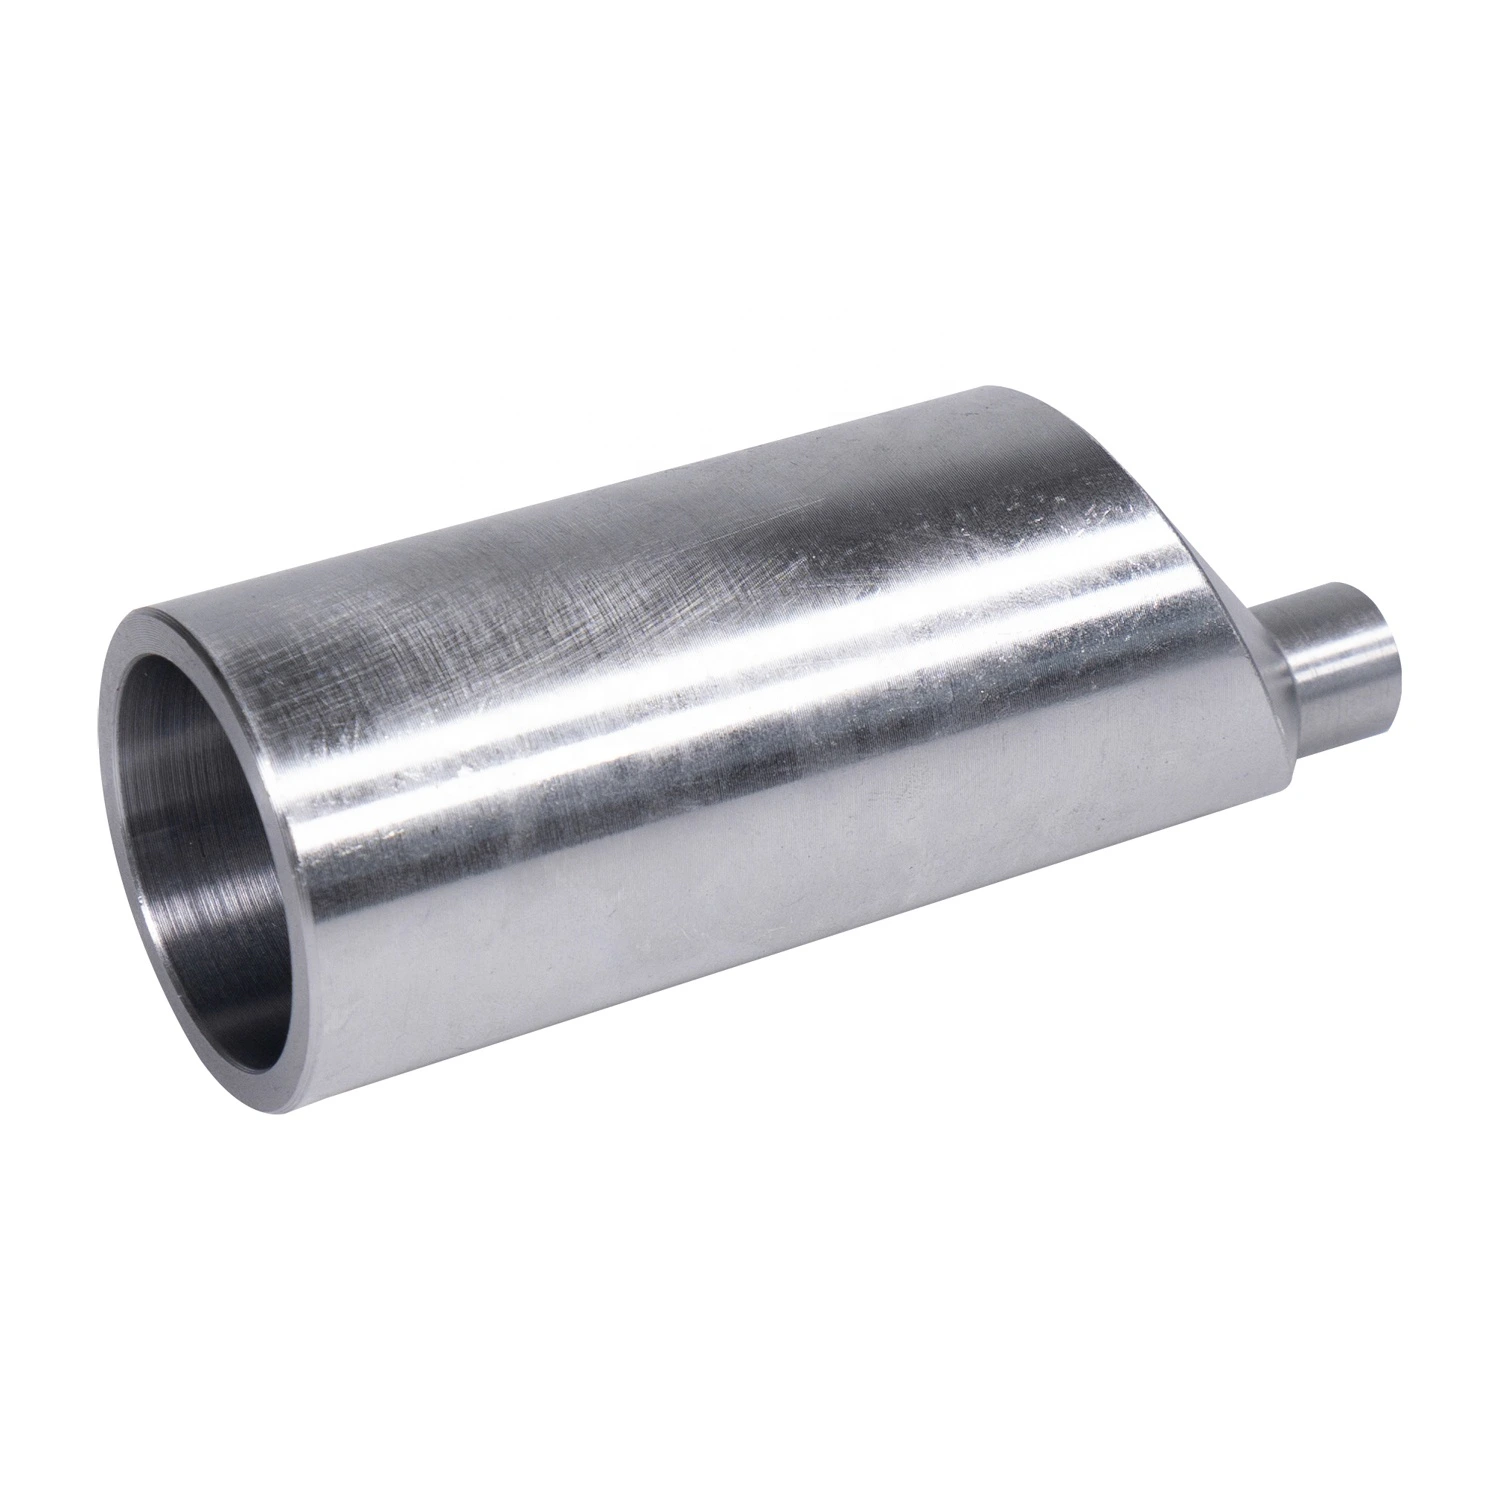
TP316L Stainless Steel Concentric Swage Nipple
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty1 Yearcustomized supportOEM
-
TechnicPolishedConnectivitySocket Weld
-
shapeRoundhead code90 Degree
-
Overall Length2 inSurface TreatmentSmooth
-
PressureHigh PressureSystem of Measurementinch
-
Mounting hole diameter0.25 inPipe FeaturesFlexible, Corrosion-resistant, Chemical Resistant, Uv Resistant, No additional Features, underground rated
-
Pipe Class3000#ApplicationAgricultural Irrigation, Automotive Repair, Heating Systems, Power Industry, Construction Engineering, Shipbuilding, petrochemical industry
-
Thread TypesNPT
This TP316L stainless steel concentric swage nipple is listed for oil-industry enquiries with an A312 material reference. The actual variant is 20NB stainless steel. Confirm the selected geometry, material records and end arrangement before assigning the component to an oil or chemical duty.
Define the concentric transition and both nominal ends
Provide a drawing identifying both end sizes, axis relationship, transition, wall thickness and tolerances. Clarify the concentric title against the 90-degree table code rather than assuming that code defines the actual nipple. Round does not establish equal ends or a complete transition geometry.
State the nominal sizing convention behind 20NB and allocate the listed 2 in length and 0.25 in hole to actual features. Confirm the envelope, installation orientation and selected availability. A single nominal label does not identify both sides of a swage nipple.
Verify TP316L supply and the actual end schedule
Specify the complete selected material designation, condition and governing document with its edition. Confirm the requirements and conformity scope associated with A312 for the ordered component, supported by traceability and material certificates. The title reference alone does not establish the complete supply package.
Obtain actual production and inspection records; Polished is finish wording rather than proof of manufacture. Resolve Socket Weld and NPT into an end schedule covering preparation, any full thread designation, mating parts, sealing and examination. Agree measurable Polished and Smooth criteria and delivery protection.
Qualify the oil composition and operating envelope
Identify actual oil composition, pressure and temperature, cycling, chemical exposure and mechanical loads. Establish the Class 3000 basis for the selected material without treating the class number as operating pressure. Require relevant corrosion, chemical or other claimed performance evidence and clarify any buried use. Document material/joint acceptance with the resolved drawing, interfaces, finish and testing requirements.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.