Steel Tube for Hydraulic Cylinders and Machinery
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
InvoicingBy Actual WeightOiled or Non-oiledNon-oiled
-
Section ShapeRoundSurface TreatmentCold Rolled
-
Tolerance±1%Alloy Or NotNon-Alloy
-
ApplicationFluid Pipe, Drill Pipe, Hydraulic Pipe, Gas Pipe, Oil PipeCertificateAPI , ISO 9001
-
Delivery Time8 ~ 14 daysGradestainless steel
-
Outer Diameter219 - 1066 mmSpecial PipeAPI Pipe, Other, EMT Pipe, Thick Wall Pipe
-
StandardASTMTechniqueERW
This steel tube listing addresses hydraulic cylinders and machinery with cold-drawn, seamless and precision-honed references. The table includes Cold Rolled, ERW and both Non-Alloy and stainless steel classifications. Confirm the actual material and processing sequence before accepting a particular bore finish or component tolerance.
Document forming and honing for the offered tube
Request the supplied specification, grade, condition, traceability and manufacturing records. Resolve the material classifications and establish seamless or ERW construction. Cold-drawn, cold-rolled and honed wording does not document one actual sequence or final condition; identify the operations and inspection evidence that apply to the order.
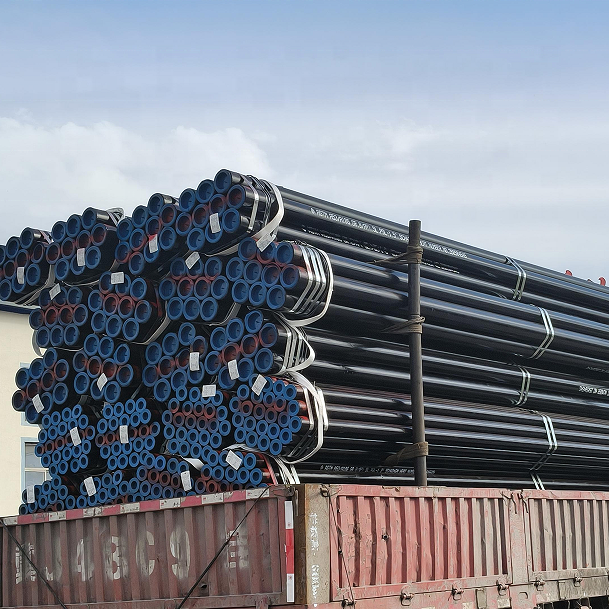
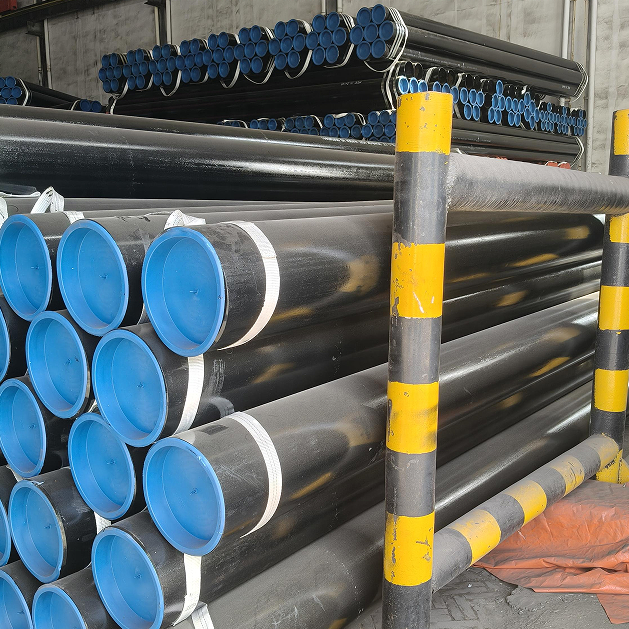
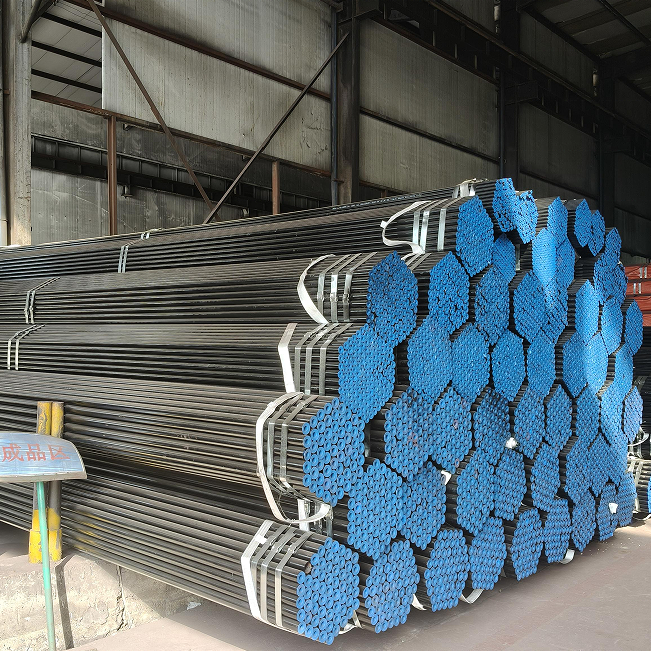
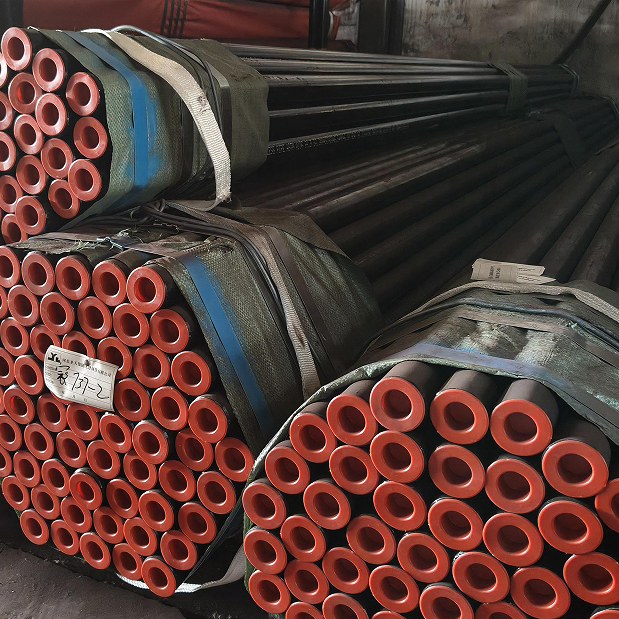
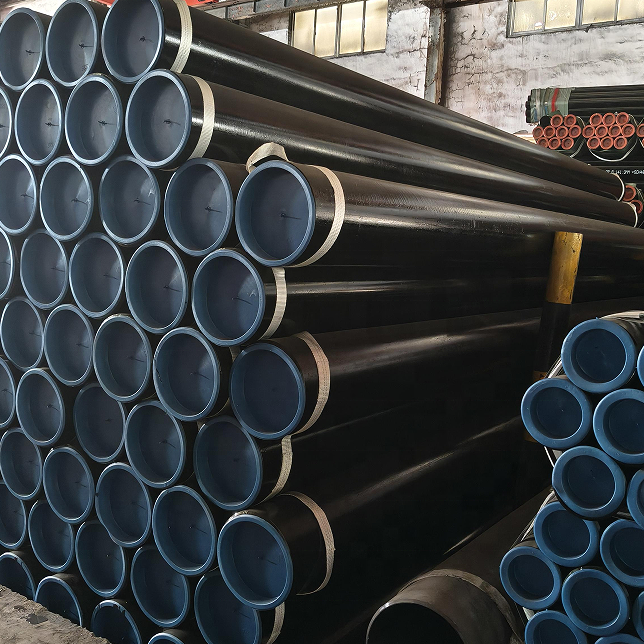
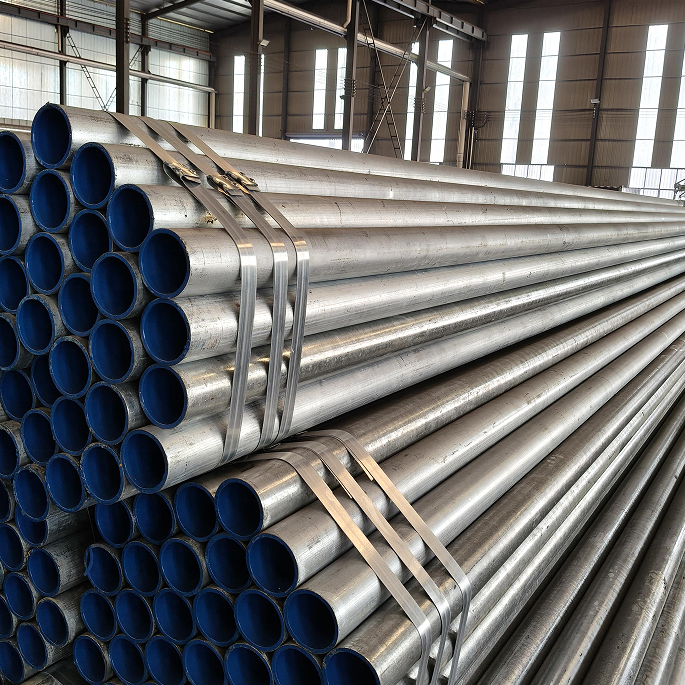
The original photograph shows bundled round tubular forms with protected ends on a truck. It cannot verify an internal honed surface, roughness or grade. Confirm the applicable material specification, edition and product coverage. General ASTM, API or ISO 9001 labels do not certify precision or a complete hydraulic-cylinder assembly.
Define the bore and fit on the component drawing
The variants offer a 6–20 mm wall range and lengths of 12 m or 6 m. Select actual outside diameter, bore, wall and cut length for the cylinder or machinery position. Reconcile the 219–1066 mm diameter range with the drawing instead of assuming it describes the selected internal bore.
Specify straightness, roundness, ends, internal surface and fit requirements. The ±1% entry needs a defined dimension and measurement method; it does not establish a honing tolerance. Confirm Non-oiled supply, required cleanliness and surface preservation. Agree actual end and mating-component criteria rather than inferring seal compatibility or leak performance from appearance.
Set operating duty and measurable inspection criteria
Provide medium, pressure, temperature, cycles, loads, joints and the relevant component requirements. Assess the documented material condition, geometry and surfaces against those inputs. Agree material, dimensional, bore, surface, end and required project tests with criteria and traceable reports. No numerical pressure rating, wear life or precision-performance guarantee follows from the title alone.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.