Lateral Butt-Weld Tee for Boilers and Power Plants
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty1 Yearcustomized supportOEM
-
TechnicFORGEDConnectivityWelding
-
shapeEqualhead codeHexagon
-
Overall LengthCustomized SizeHeightCustomized Size
-
Surface TreatmentPaintingPressureHigh Pressure
-
System of MeasurementMetricMounting hole diameterCustomized Size
-
Pipe FeaturesOtherPipe ClassOther
-
ApplicationOtherThread TypesCustomized Size
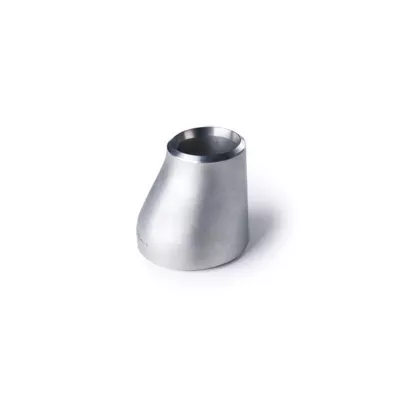
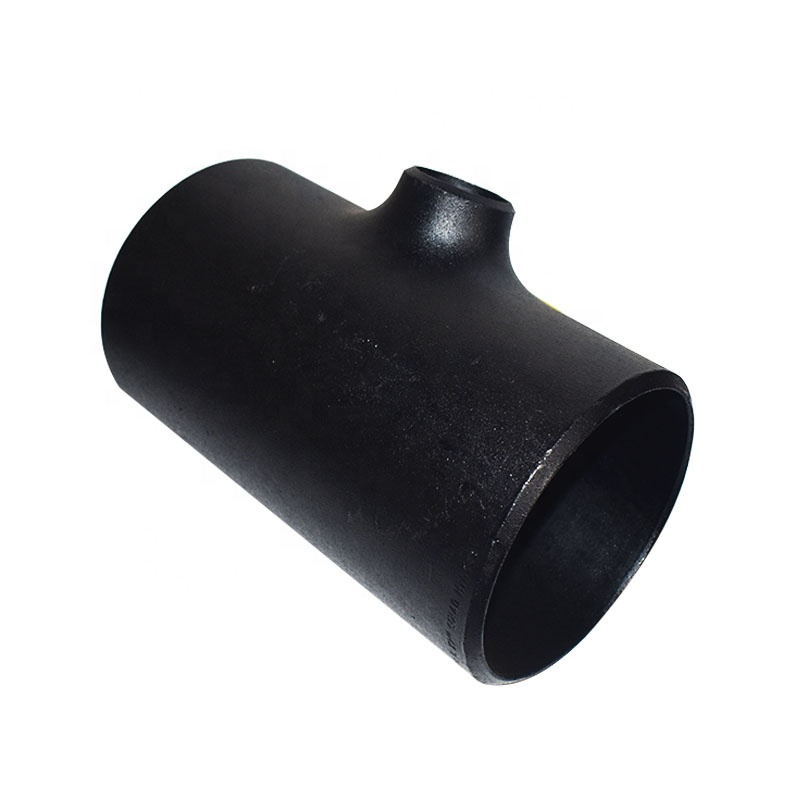
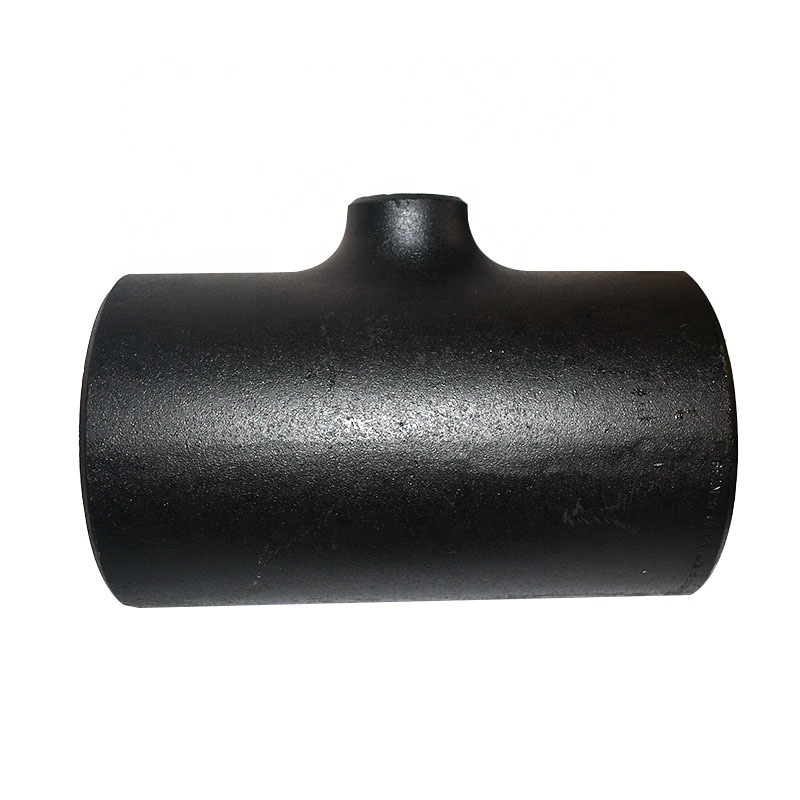
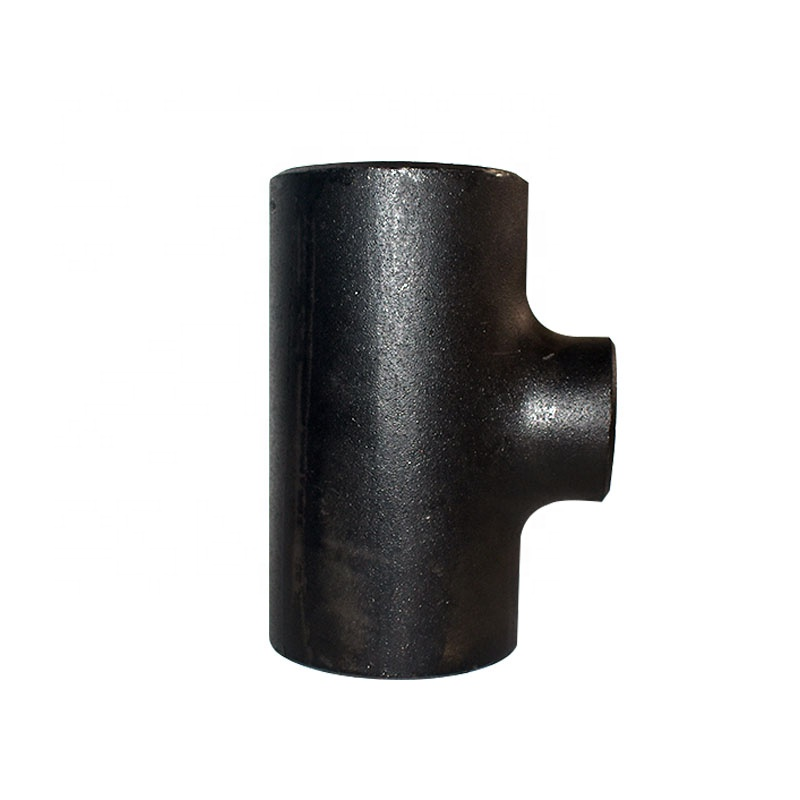
This lateral tee listing addresses boilers and power plants with ASTM A234, WP11, WP22 and alloy steel references. The variants instead use Reducer labels with Carbon Steel or a234wpb. Confirm the actual fitting family, supplied grade and branch drawing before evaluating the butt-weld connection for thermal service.
Resolve the alloy grade and selected branch fitting
Obtain the actual specification, grade, condition, traceability and material inspection records. The carbon options do not verify WP11 or WP22 alloy supply, and the title grades are not interchangeable selections. Identify one ordered material and its required conformity package rather than treating title wording as grade certification.
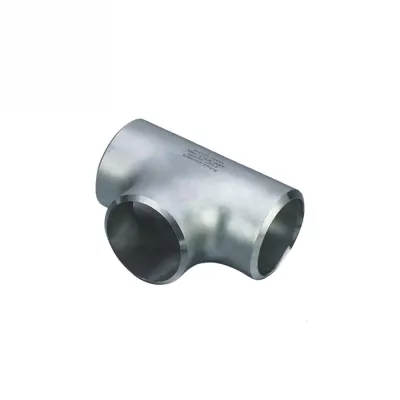
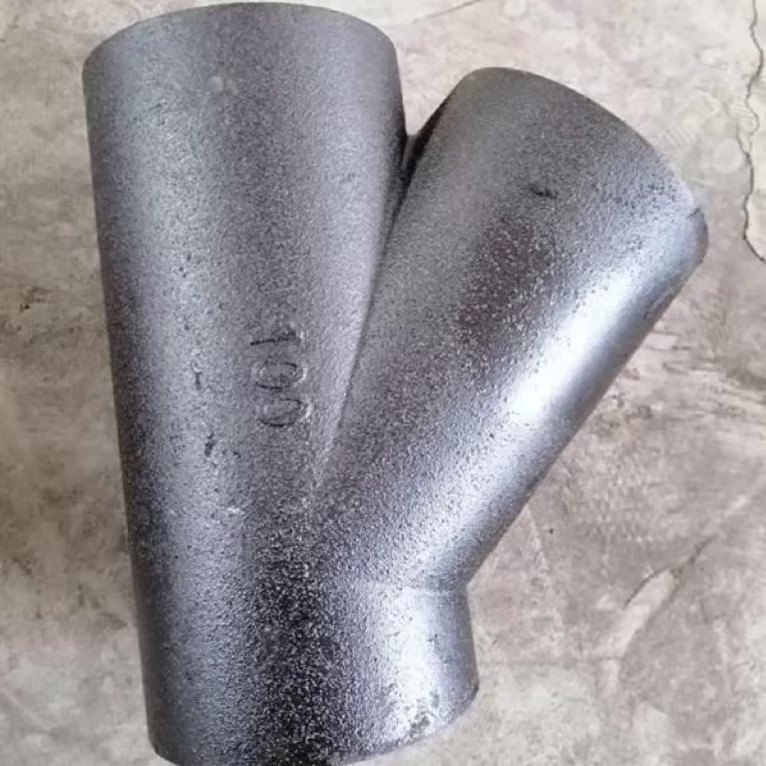
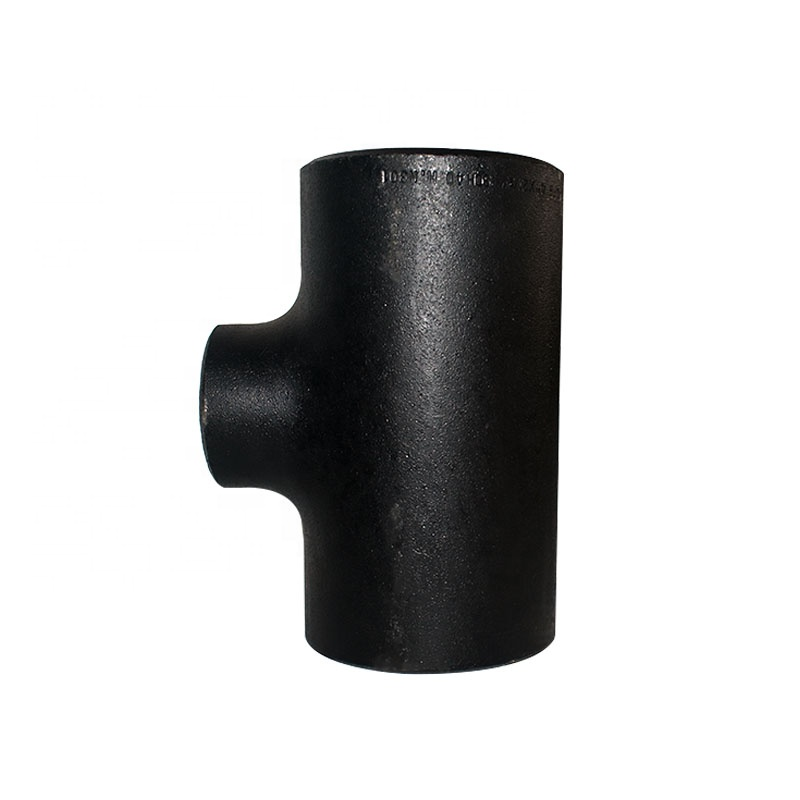
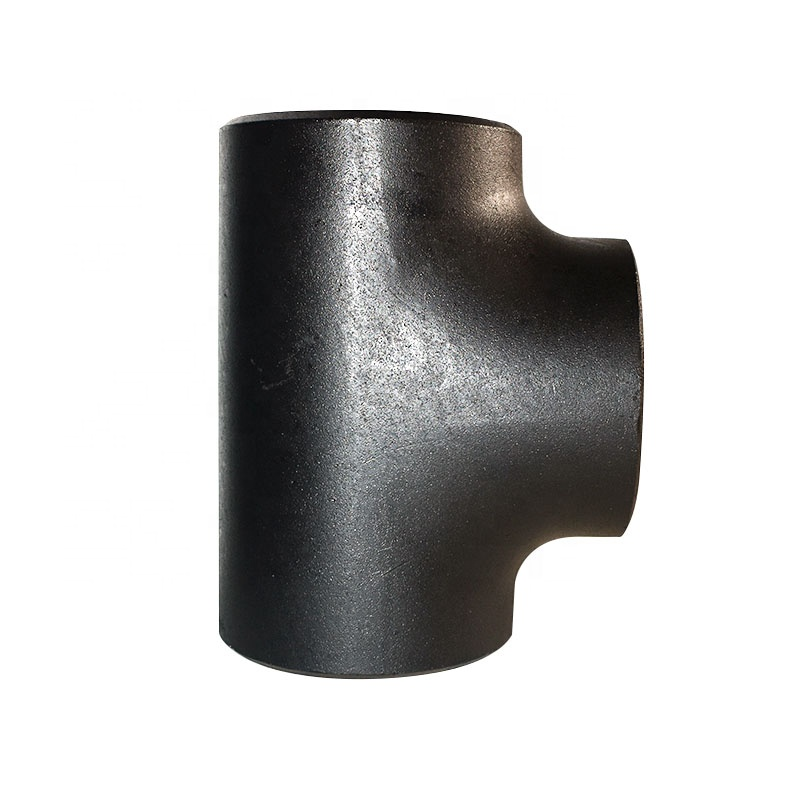
The original image shows a three-opening fitting with an angled branch. It supports a lateral tee enquiry but cannot measure angle or establish material. Map the Reducer-labelled choices to the supplied drawing. Identify the ASTM A234 edition, product coverage and project requirements after the actual material and fitting are confirmed.
Specify butt-weld geometry and thermal-joint requirements
The half-inch to 110-inch choice is a size range, not selected run and branch dimensions. Define actual diameters, bore, wall, branch angle and centre-to-end dimensions. Reconcile lateral geometry with the Equal table entry. Confirm the butt-weld ends, Welding connection, bevels and mating-pipe requirements.
Set ordered length and height values where the table says Customized Size. Verify actual production and finish against FORGED and Painting entries. Hexagon head, mounting-hole and thread fields do not establish a flange or threaded end. State relevant joint features and dimensional acceptance explicitly on the branch drawing.
Agree boiler conditions and traceable material acceptance
Provide medium, contaminants, pressure, temperature, cycles, gradients, loads and joint details. High Pressure and Other class entries supply no numerical allowable limit. Assess the documented material condition and geometry against the actual duty. Agree material, dimensional, angle, end, surface and required project tests with criteria and traceable reports before approving the branch for the installation.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.