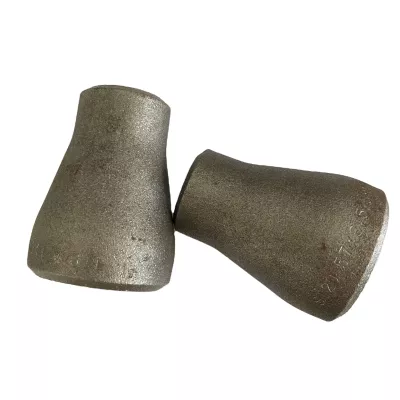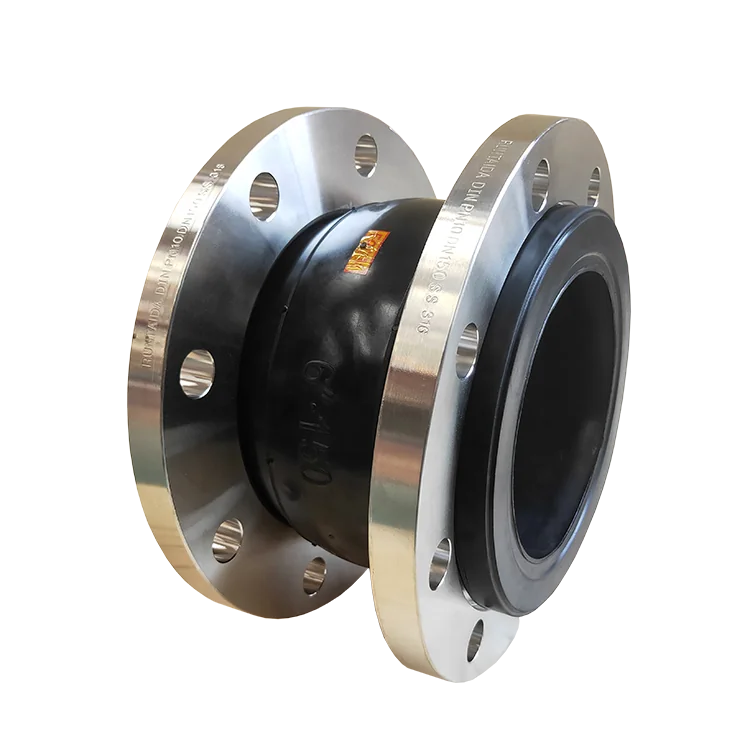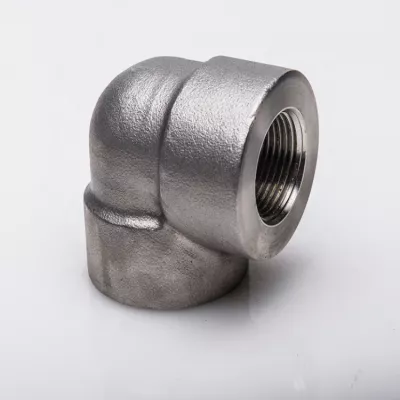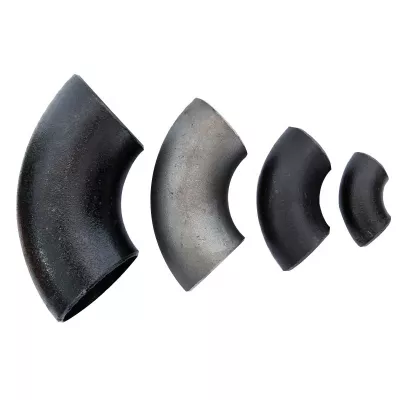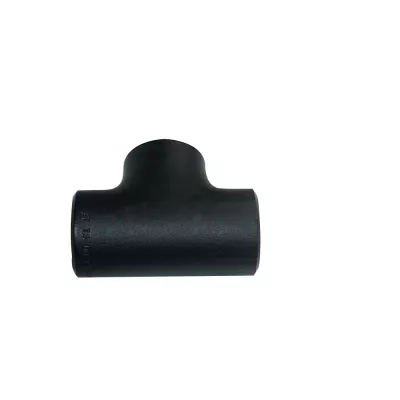
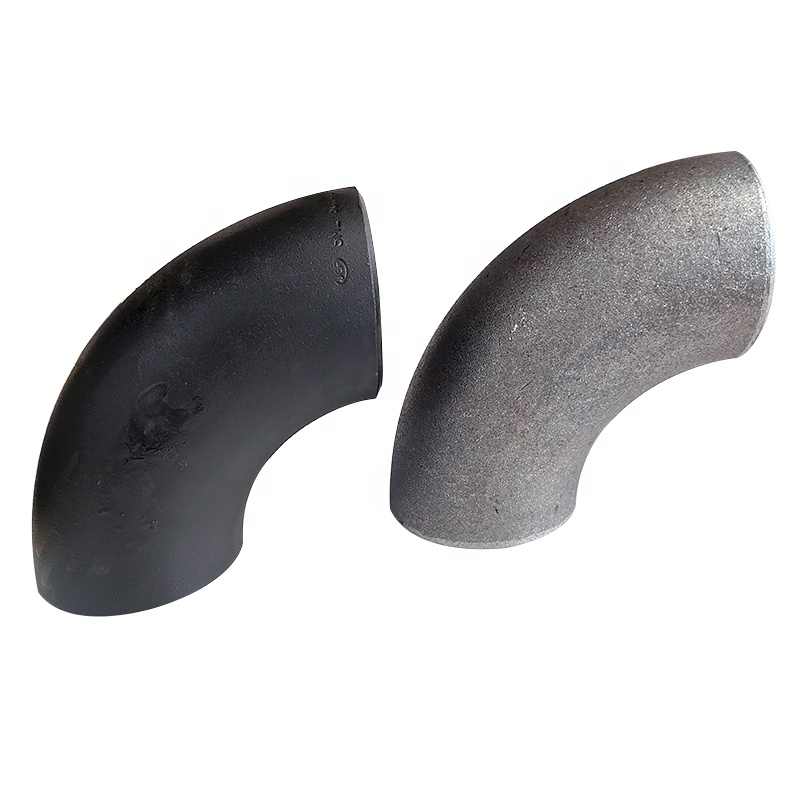
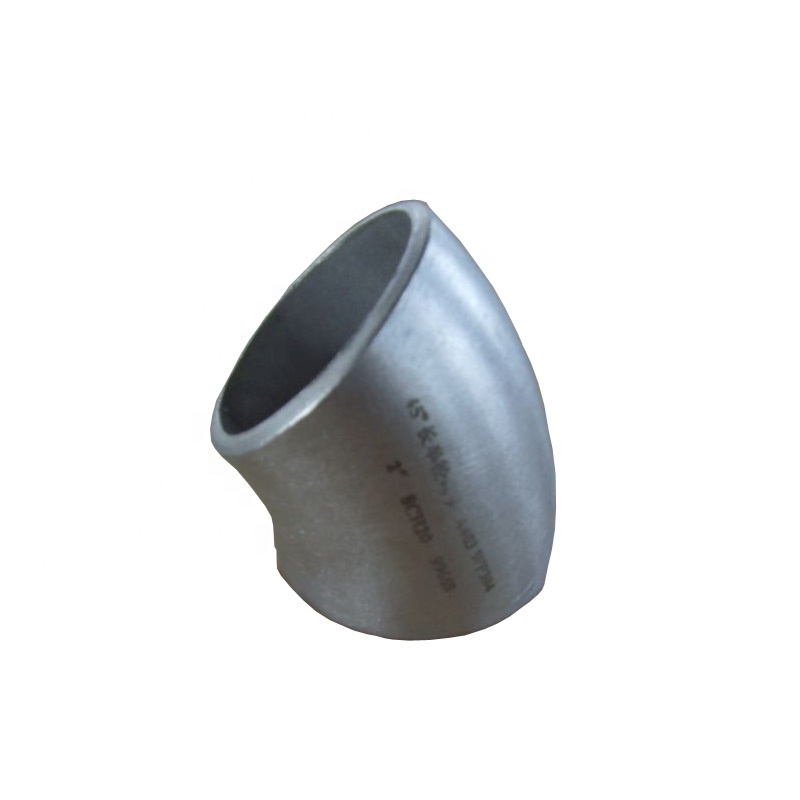
SCH80 Carbon Steel 60-Degree Butt-Weld Elbow
For industrial sourcing
Prepare a clearer RFQ
Include the details below so RELIA can understand the part and discuss the next step with you.
- Drawing, sample, or reference standard
- Material grade and preferred process
- Dimensions, tolerances, and surface finish
- Application, target quantity, and destination
Production timing, packing, and shipping terms are confirmed for each project after specifications and trade terms are agreed.
-
warranty3 Yearscustomized supportOEM
-
TechnicFORGEDConnectivityWelding
-
shapeBendhead codeHexagon
-
Overall Length1/2" - 12"Height1/2" - 12"
-
Surface TreatmentsmoothPressureLow Pressure
-
System of MeasurementINCHMounting hole diameter1/2" - 12"
-
Pipe Featurescorrosion resistantPipe ClassNot Rated
-
ApplicationConstruction EngineeringThread TypesNPT
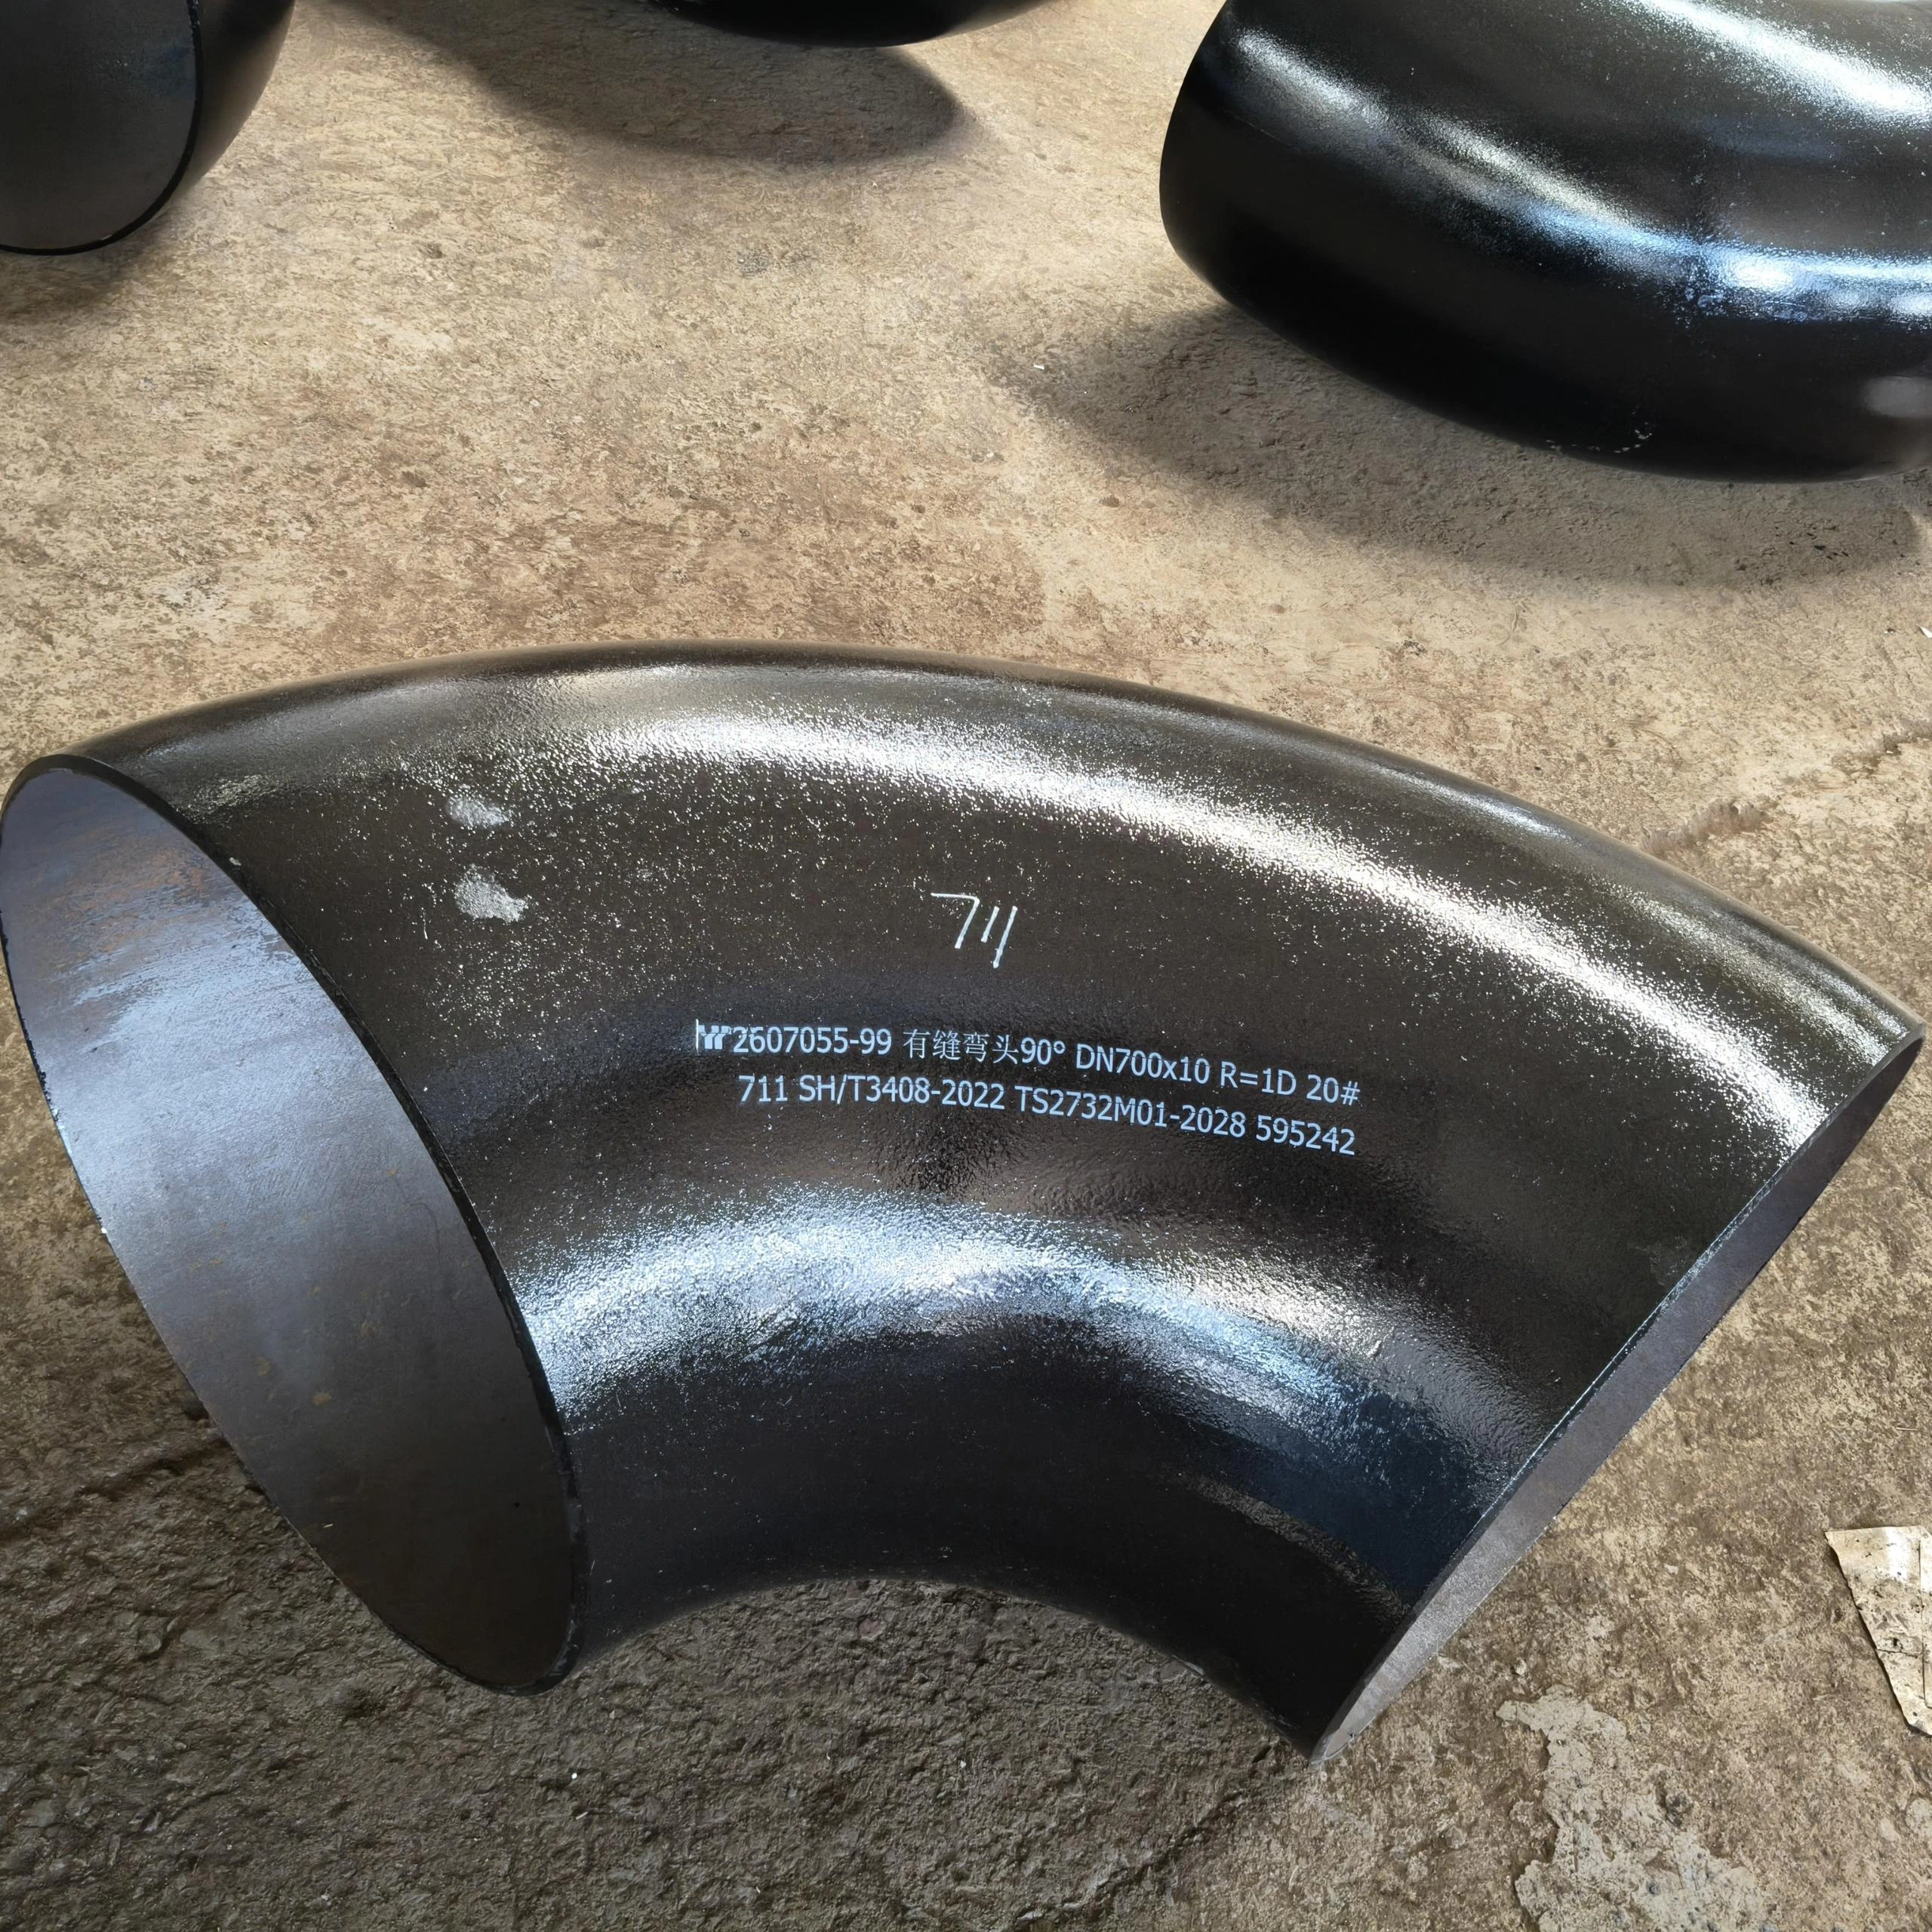
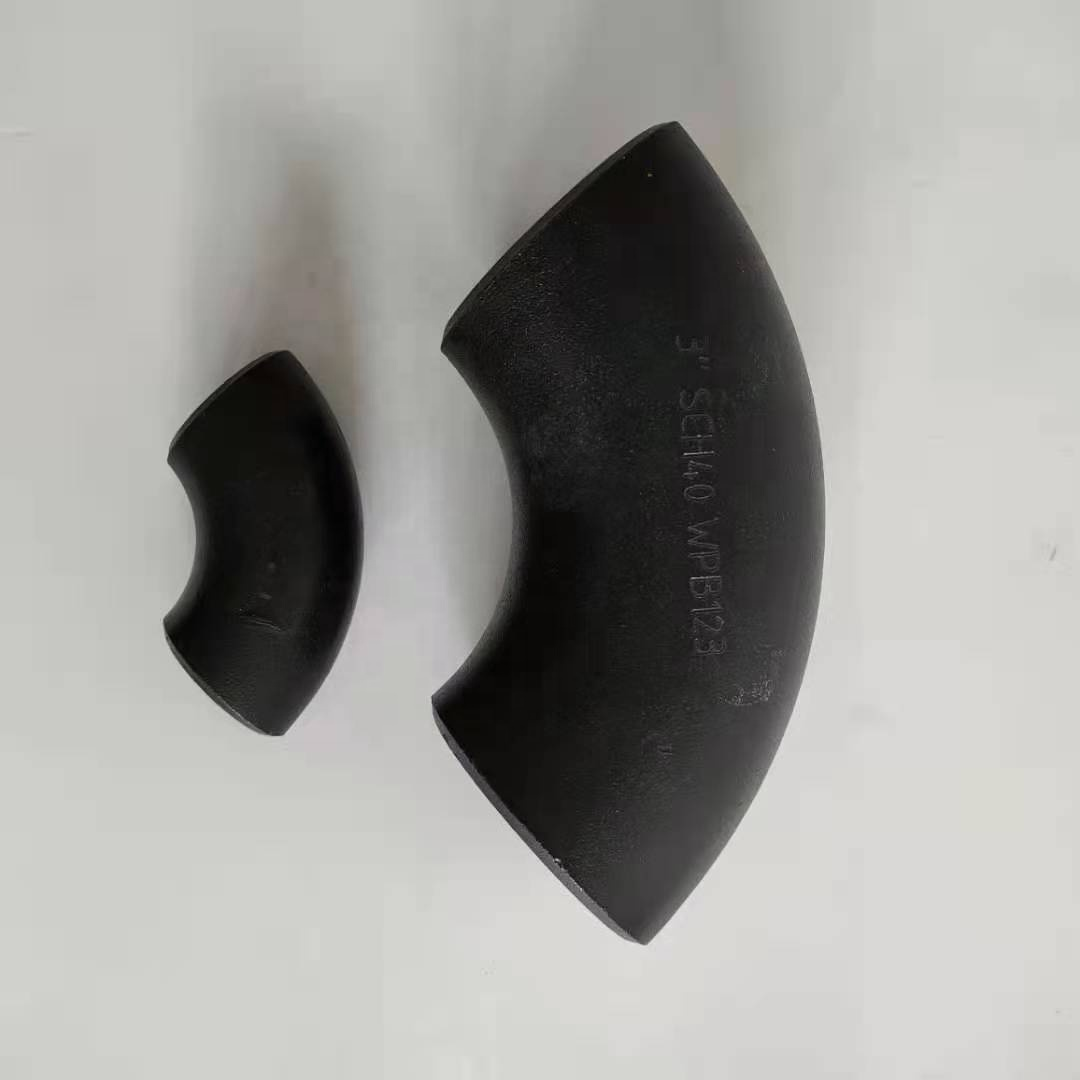
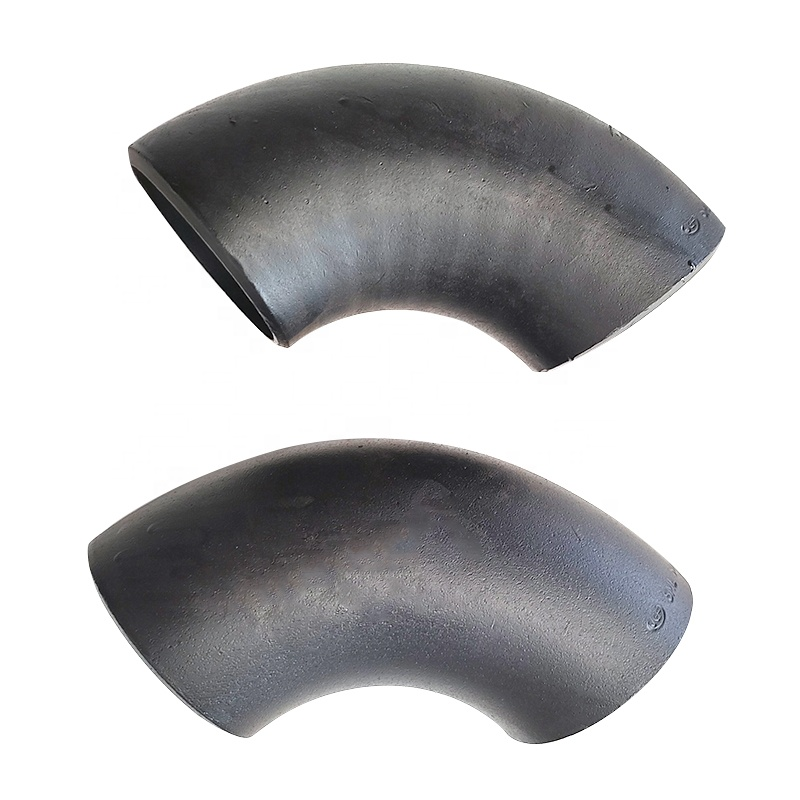
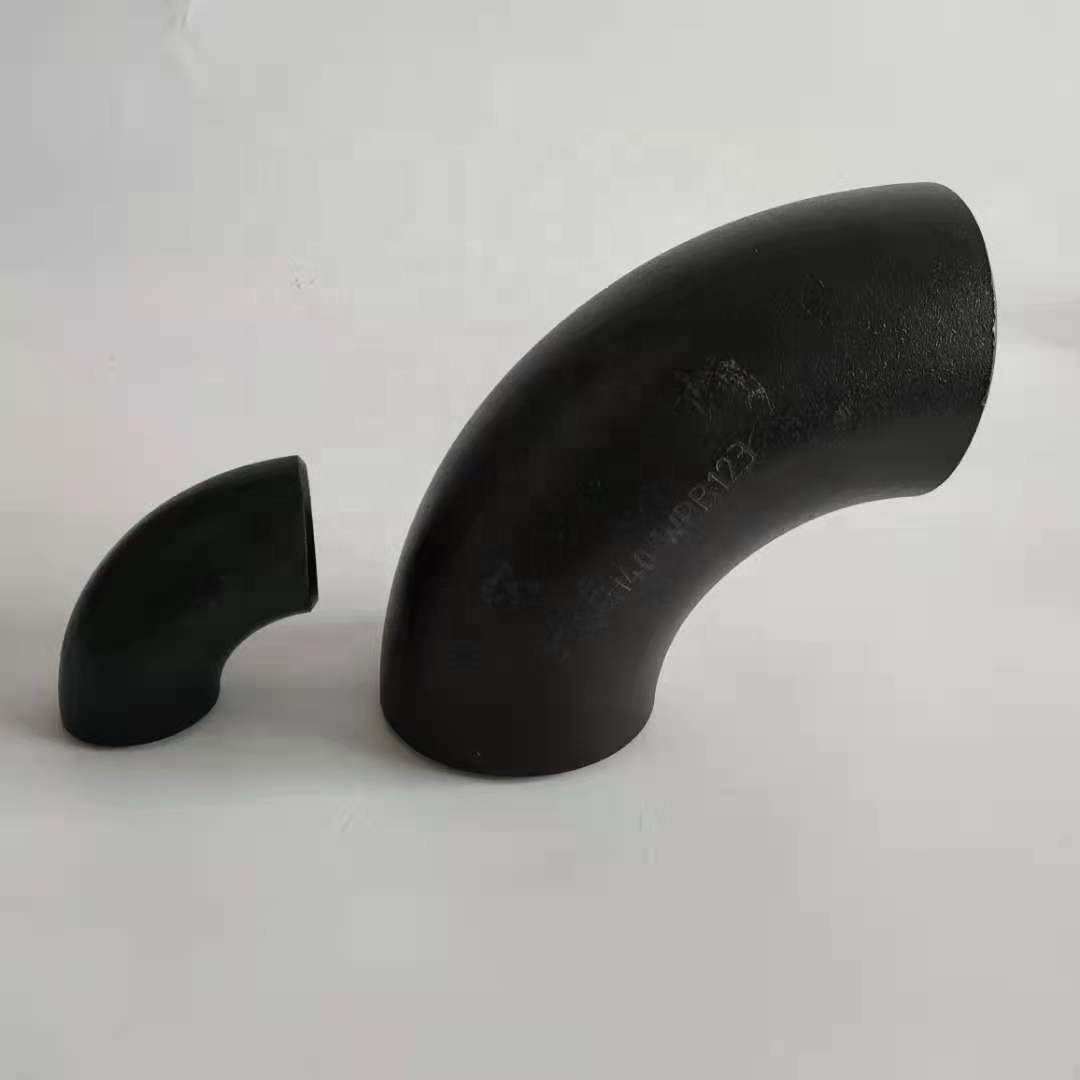
This SCH80 carbon steel elbow is listed with a 60-degree butt-weld configuration for construction engineering enquiries. The title also refers to seamless manufacture and A234, while the table records forging and NPT. Allocate these details to the actual ordered component before specifying supply.
Define the 60-degree elbow and schedule dimensions
Specify the nominal size, bend radius, wall thickness, overall dimensions and tolerances on a drawing. Verify the 60-degree angle and the dimensional document governing SCH80 at the selected size. The schedule label alone supplies no numerical wall thickness or radius.
The available option spans 1/2 inch to 12 inch, and that range also appears under length, height and mounting hole. Identify the actual meaning of those fields and the exact ordered dimensions. Confirm availability and installation clearance for the selection rather than treating the range as a complete drawing.
Complete the A234 material and production requirements
Request the full material designation, selected grade and condition, governing edition, traceability and certificates. A234 wording does not establish WPB or another complete grade. Clarify how the seamless title and forged table entry relate to the actual manufacturing route and inspection records.
Prepare an end schedule distinguishing butt-weld preparation from any NPT interface. State mating components, thread designation where applicable, sealing and examination requirements. The two labels do not prove interchangeable connections. Define measurable smooth surface criteria and transport protection.
Assess the selected construction operating conditions
Provide the medium, numerical pressure and temperature, cycling, corrosion exposure and mechanical loads. Qualitative low-pressure wording with an unrated class is insufficient to approve this construction duty. Obtain relevant corrosion evidence and agree material/joint acceptance, supported by geometry, manufacturing, interface, surface and test documents in the quotation.
Technical information for every product inquiry
Prepare the requirement before final product confirmation.
The product page is a starting point. Drawings, samples, interfaces, materials, quantities and acceptance requirements are reviewed before stock matching or custom production is confirmed.
Discuss this product in your project context.
Share the available drawing, sample, reference, target quantity and application information. Unknown items can remain open for review.