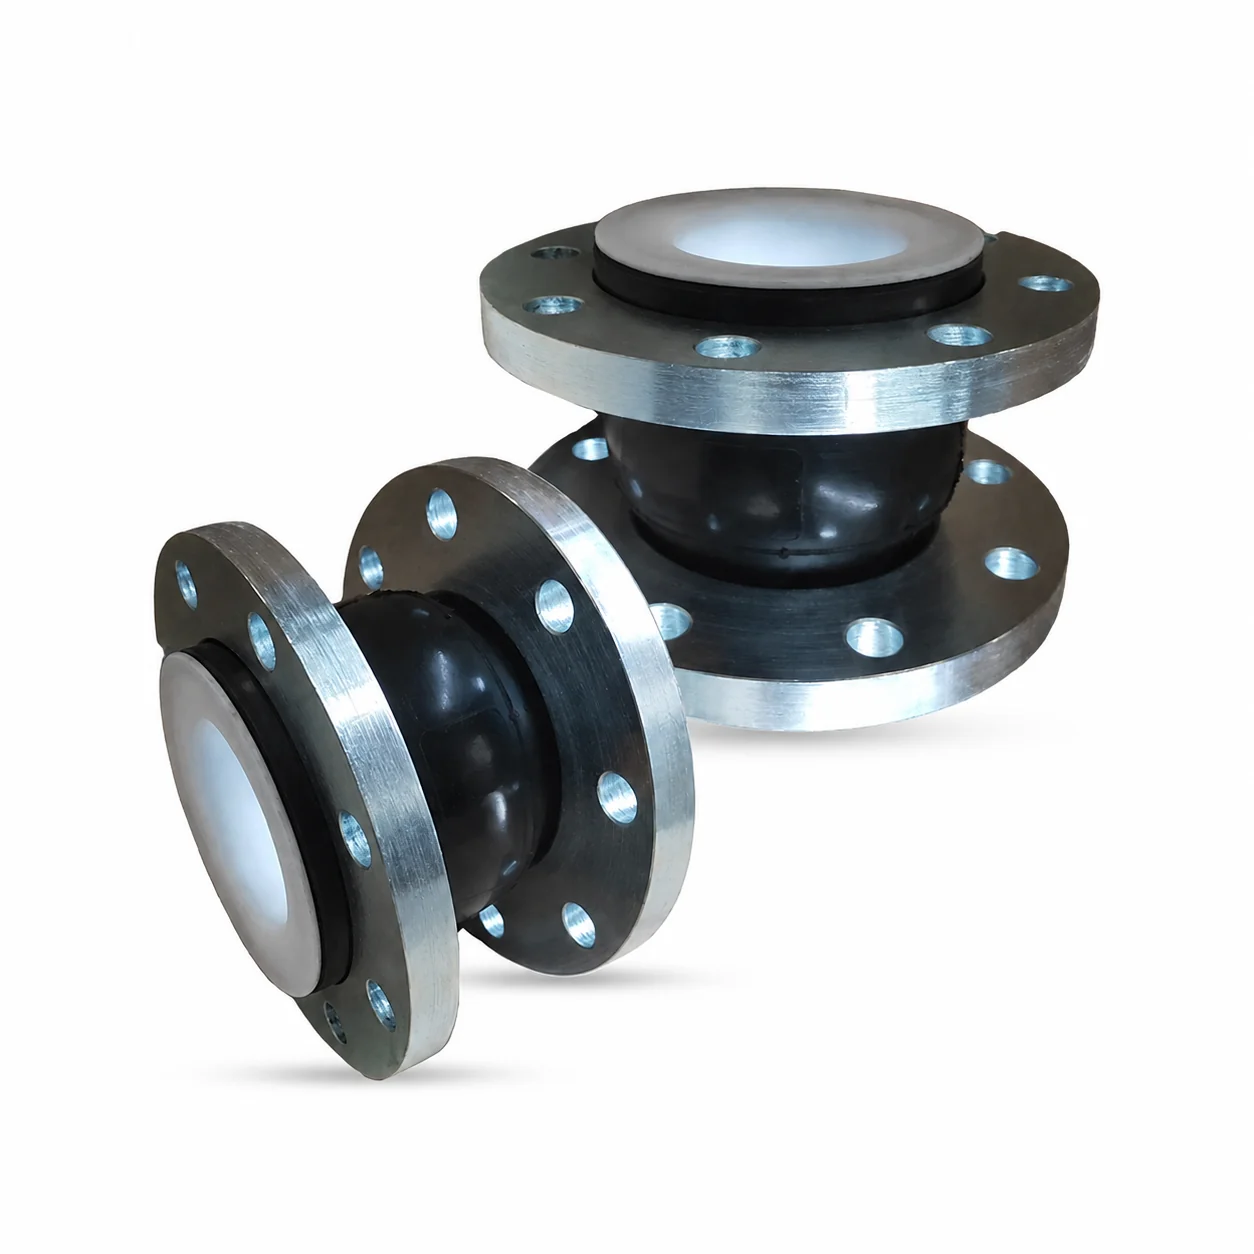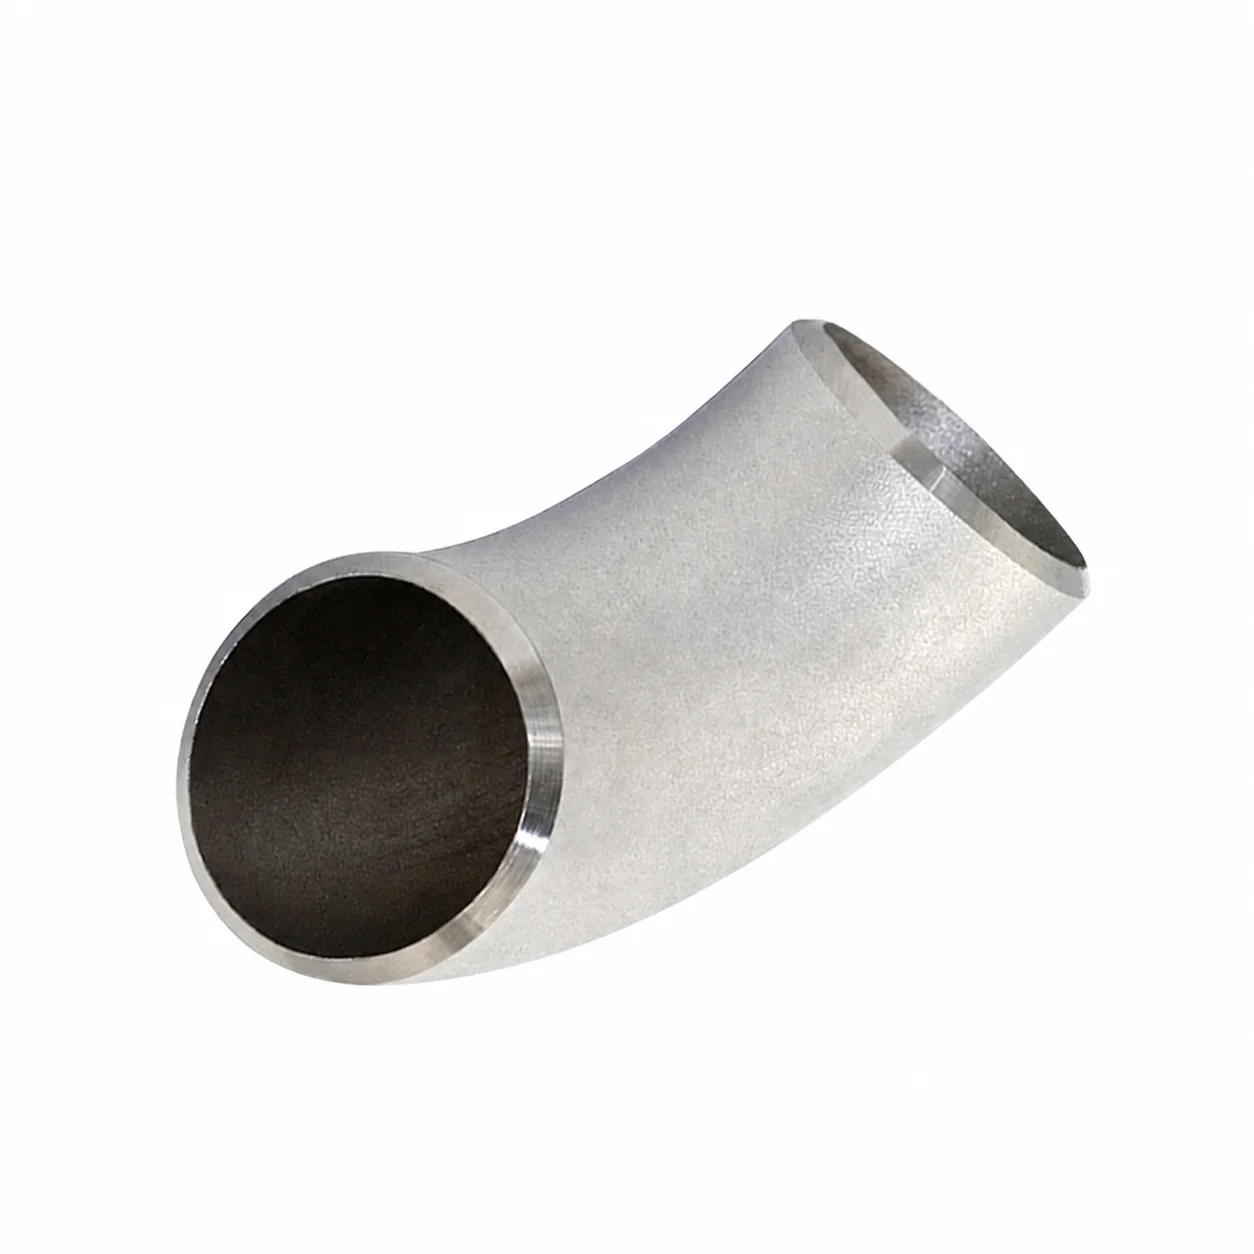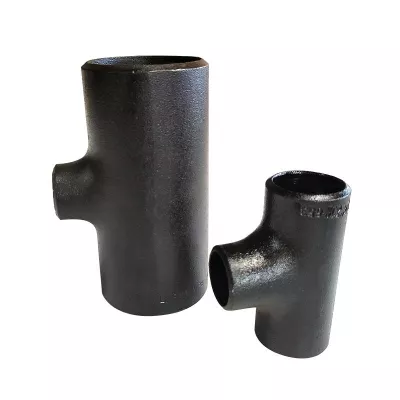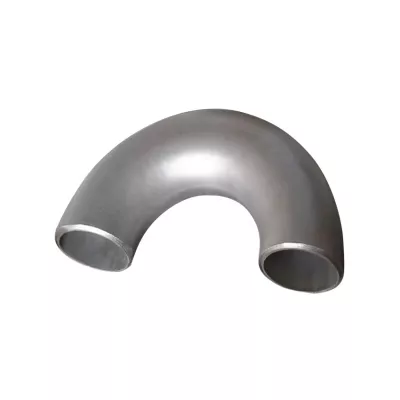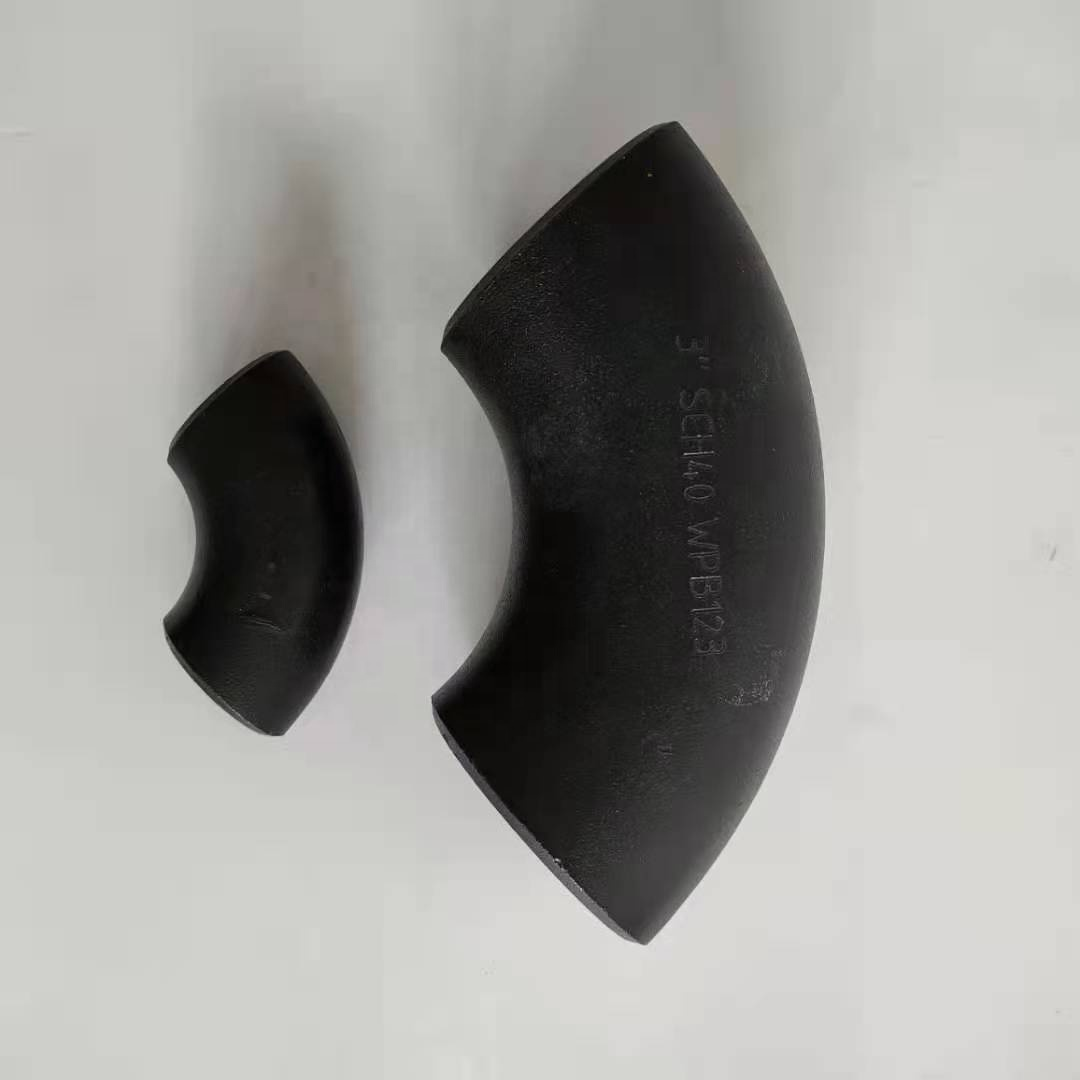
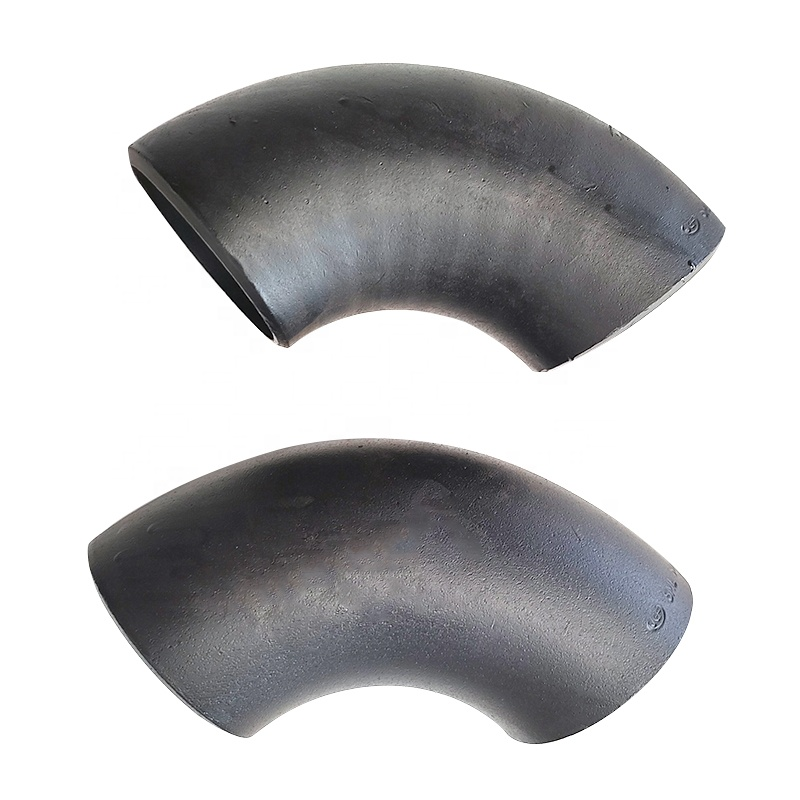
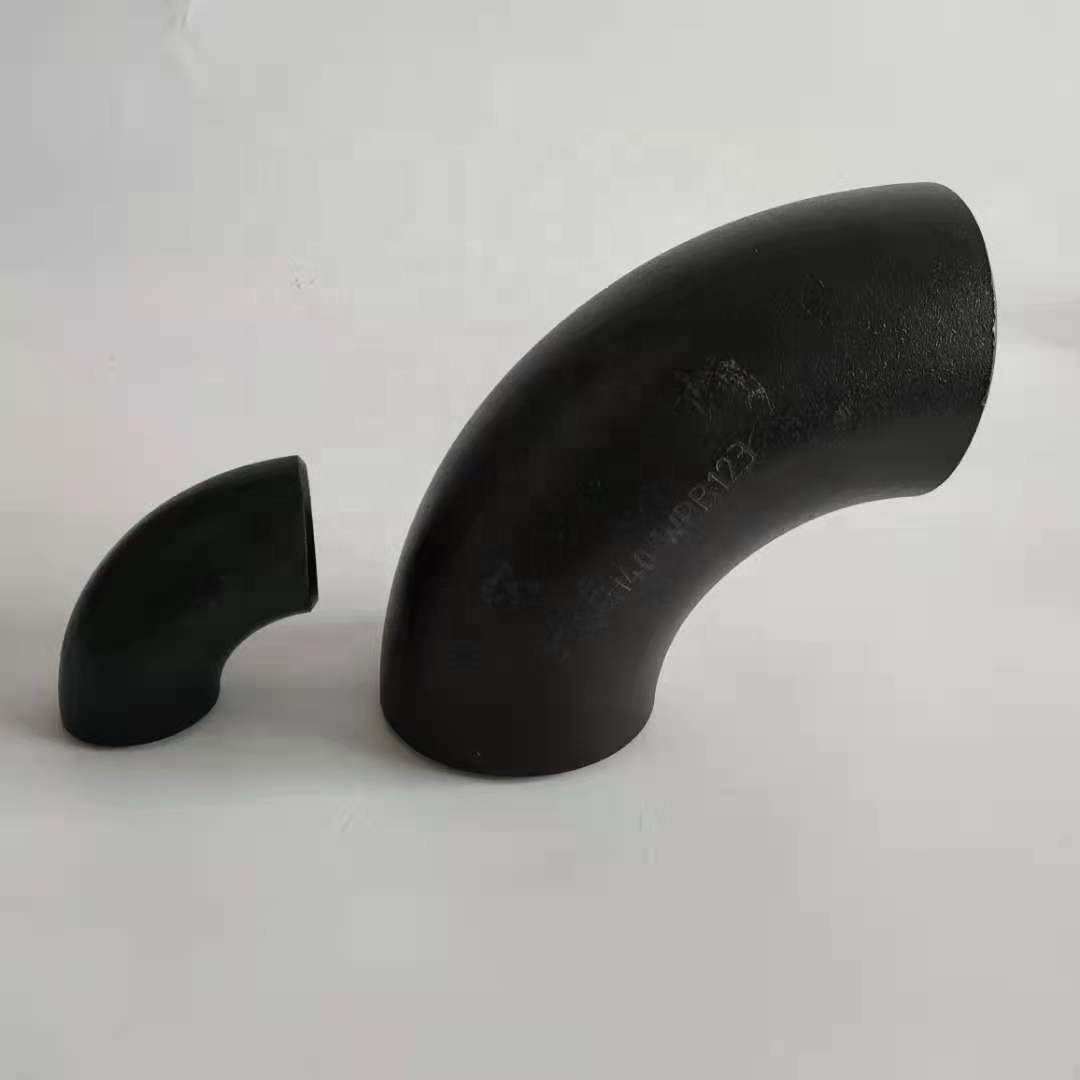
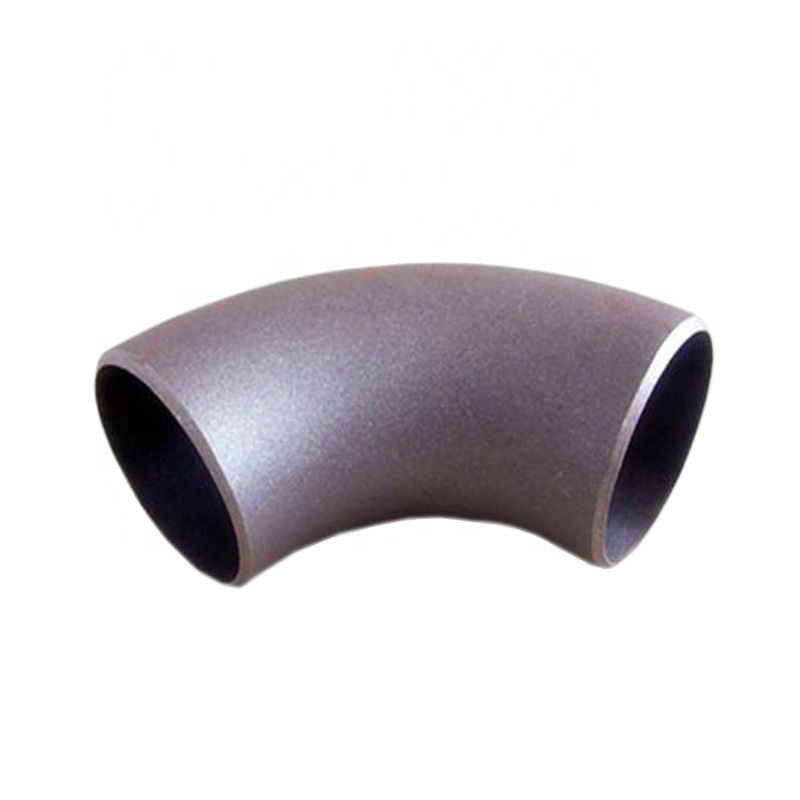
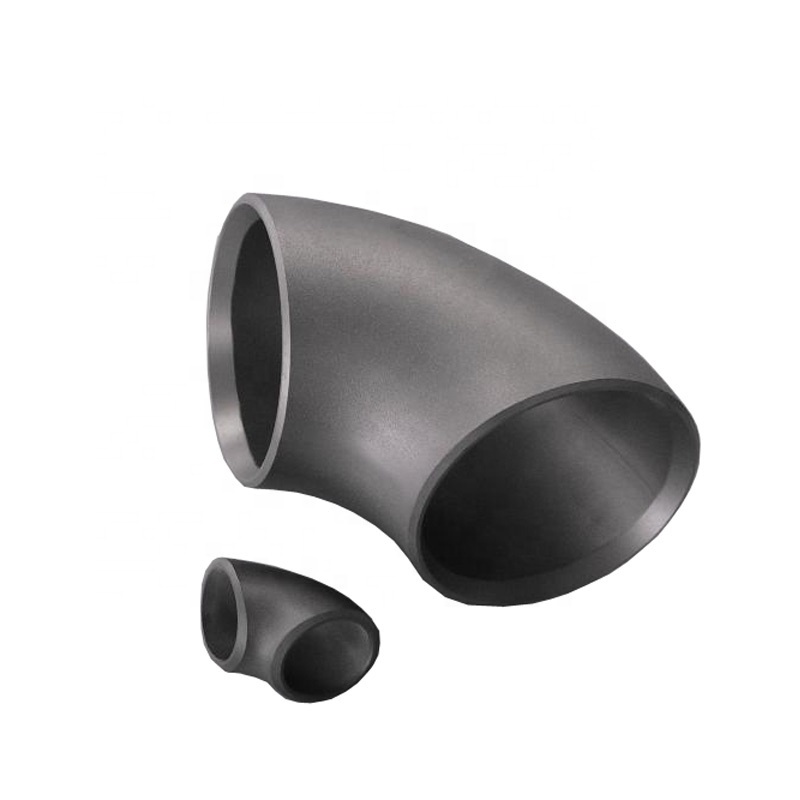
B16.9 Q235 1/2-Inch 90° Short-Radius Butt-Weld Elbow
Para compras industriales
Prepare una RFQ más clara
Incluya estos datos para que RELIA comprenda la pieza y pueda acordar el siguiente paso.
- Plano, muestra o norma de referencia
- Calidad del material y proceso preferido
- Dimensiones, tolerancias y acabado superficial
- Aplicación, cantidad objetivo y destino
Los plazos de producción, el embalaje y el envío se confirman para cada proyecto tras acordar especificaciones y condiciones comerciales.
-
warranty1 Yearcustomized supportOEM, ODM
-
model numberelbow 2417TechnicCasting
-
ConnectivityFemale/MaleshapeReducing
-
head codeRoundSurface TreatmentPainting
-
Mounting hole diameter0.17 inPipe Class150
This elbow enquiry starts with the half-inch Q235 requirement in the title and the intended 90-degree short-radius butt-weld configuration. Select one offered model before assigning those requirements to an option. The millimetre size labels, material alternatives and Reducing field need a documented relationship to the actual bend and its pipe connections.
Identify both pipe ends before choosing a size
State the required nominal size and outside diameter for each end. Ask which millimetre-labelled option corresponds to the half-inch requirement and whether the selected model has equal or reducing ends. A Reducing label alone does not define the two sizes. Request an elbow drawing with wall thickness, centreline radius, end-to-centre dimensions and the accepted 90-degree angle. Check that this measured envelope fits the pipe route rather than estimating radius or end sizes from a product image.
Keep Q235 separate from photographic markings
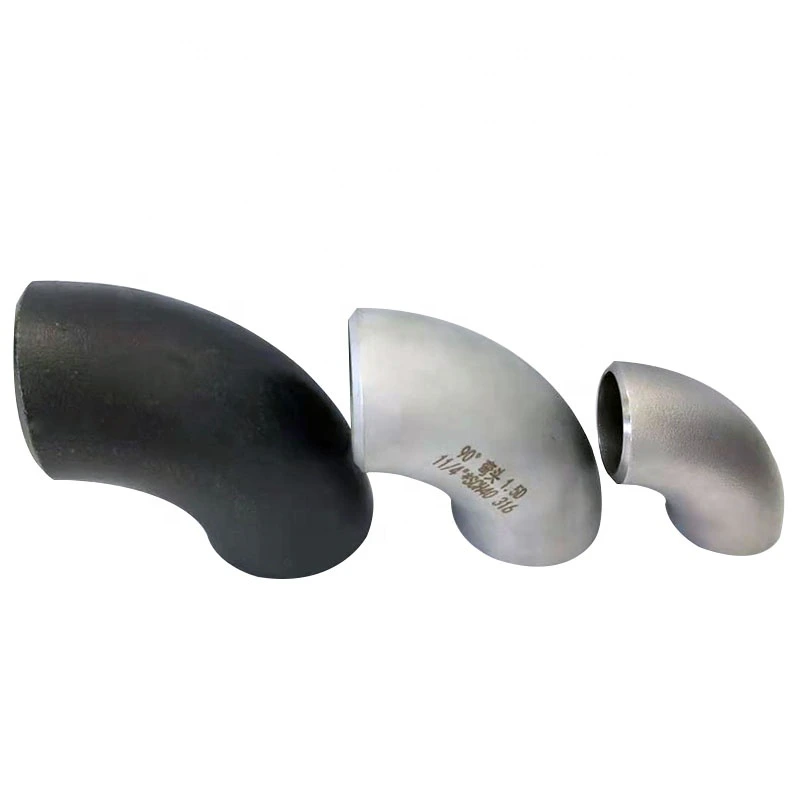
Confirm the governing Q235 material specification and records for the selected carbon-steel item. A stainless-steel choice requires its own agreed grade. Visible markings on one photographed fitting do not identify every variant's grade or wall schedule. Request production and inspection evidence for the actual model before accepting its manufacturing route; the Casting field cannot replace that evidence. Define bevel, land and end wall for the mating pipe instead of relying on Female/Male as the connection description.
Establish the acceptance basis
Give the required B16.9 edition and dimensional inspection criteria alongside the joining and inspection requirements. Provide the fluid, operating pressure and temperature and relevant corrosion conditions for assessment of the complete welded joint. Class 150 does not by itself establish its pressure-temperature limit, and Painting or mounting-hole information does not qualify a protective finish or bend geometry. An actionable enquiry joins the half-inch option mapping and end-pair drawing to the exact Q235 specification, documented production route and agreed acceptance records.
Información técnica para cada consulta
Prepare los requisitos antes de confirmar el producto.
La página es el punto de partida. Planos, muestras, interfaces, materiales, cantidades y criterios de aceptación se revisan antes de confirmar stock o fabricación.
Comente este producto en el contexto de su proyecto.
Comparta plano, muestra, referencia, cantidad y aplicación. Los puntos desconocidos pueden quedar abiertos para revisión.