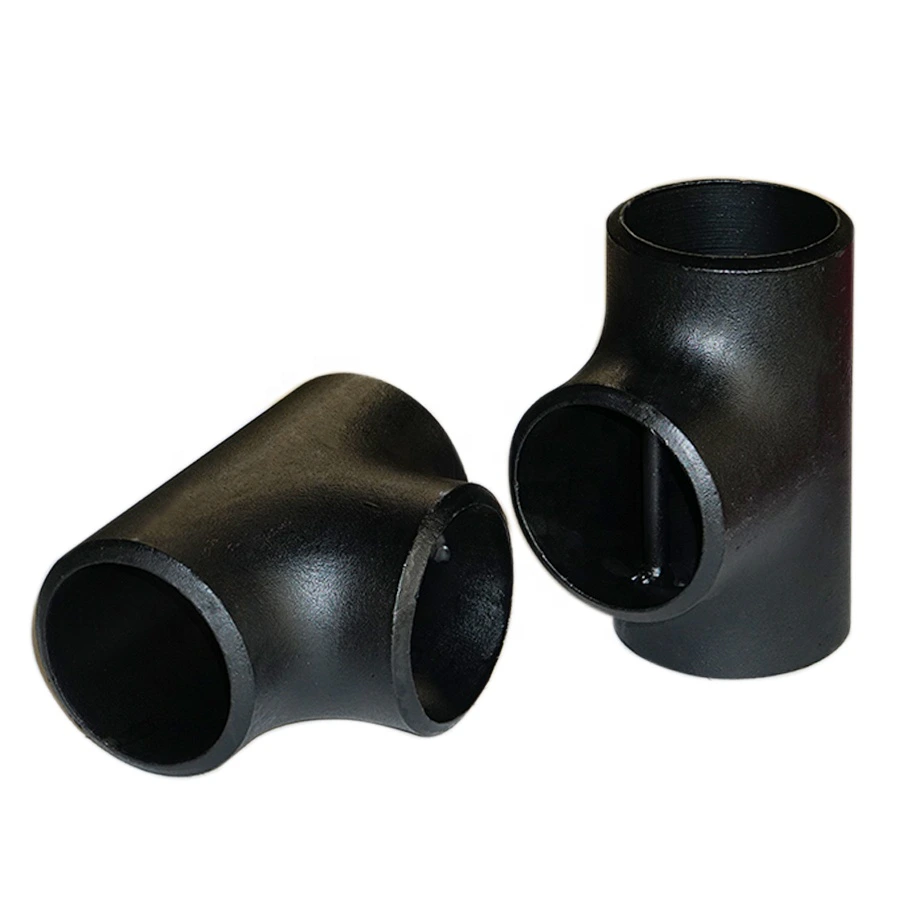
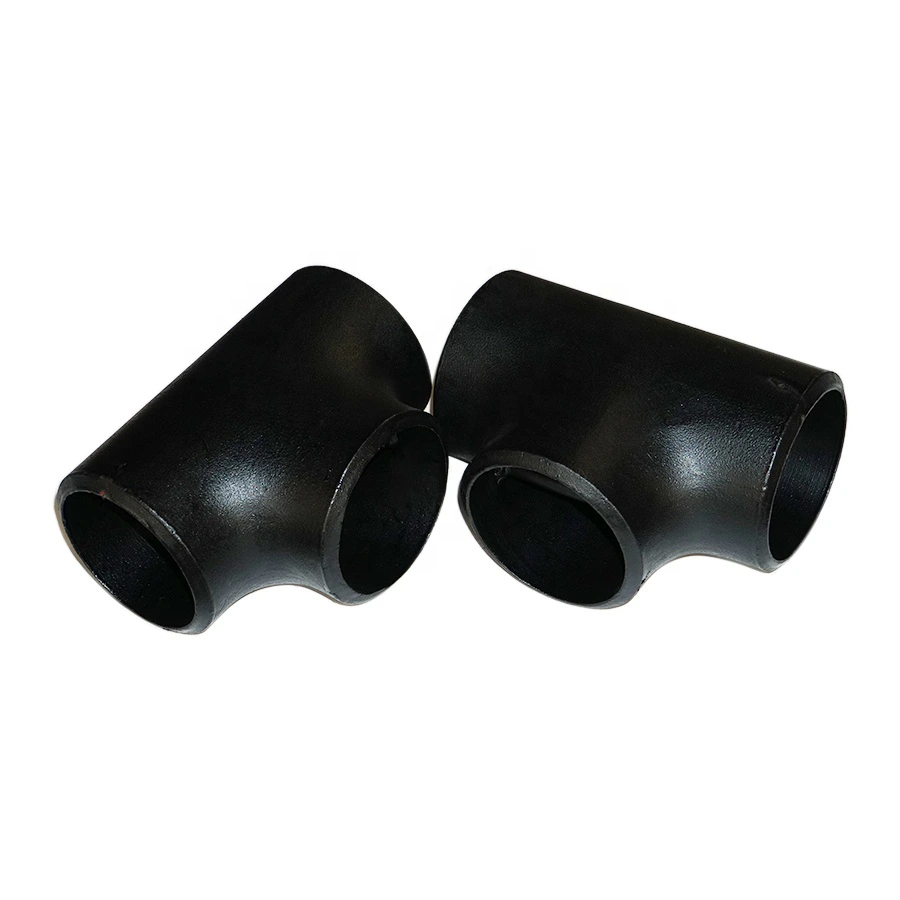
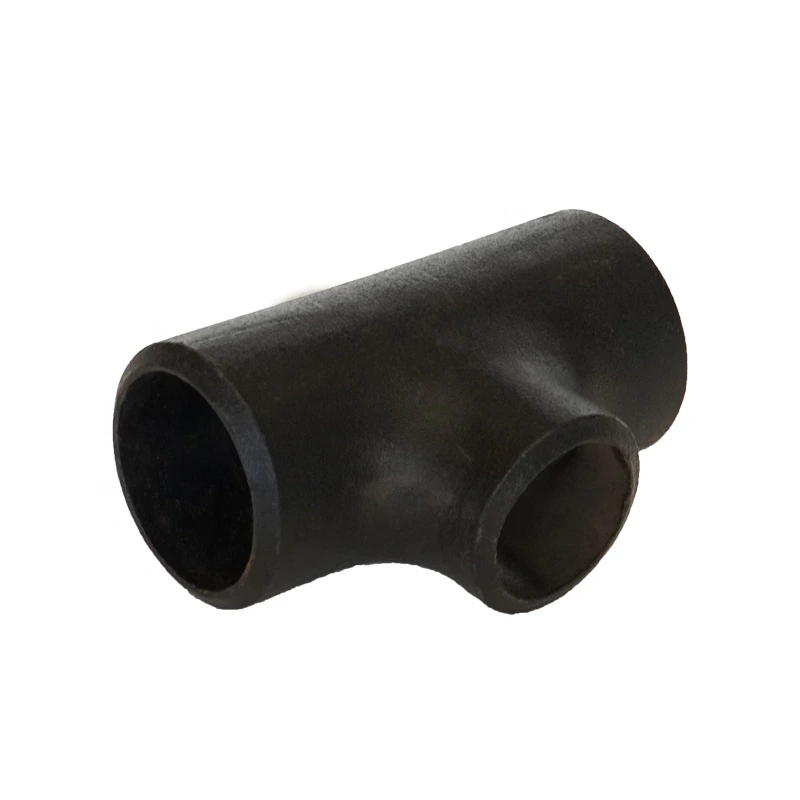
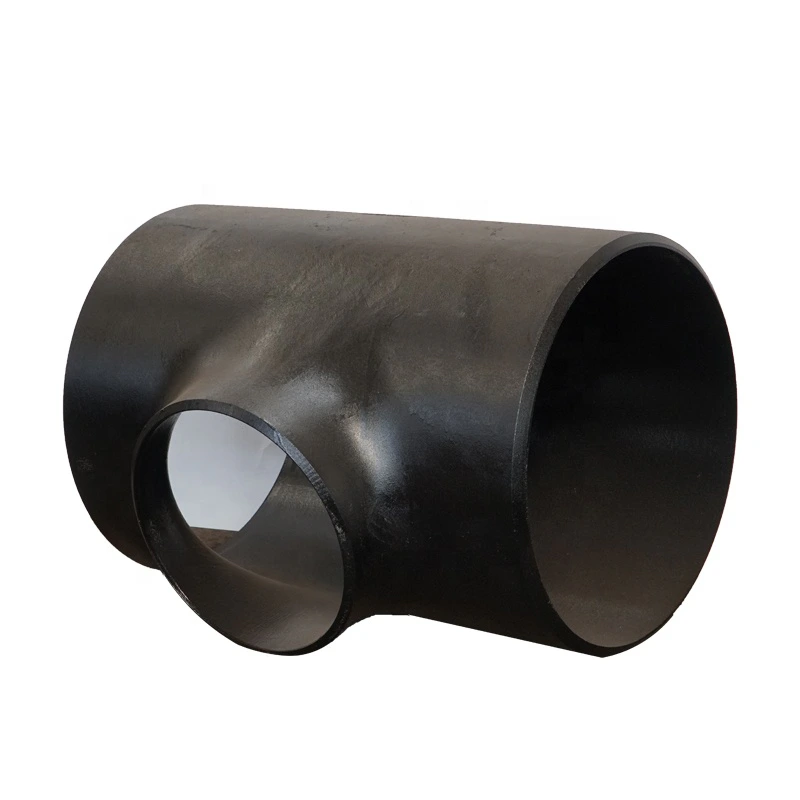
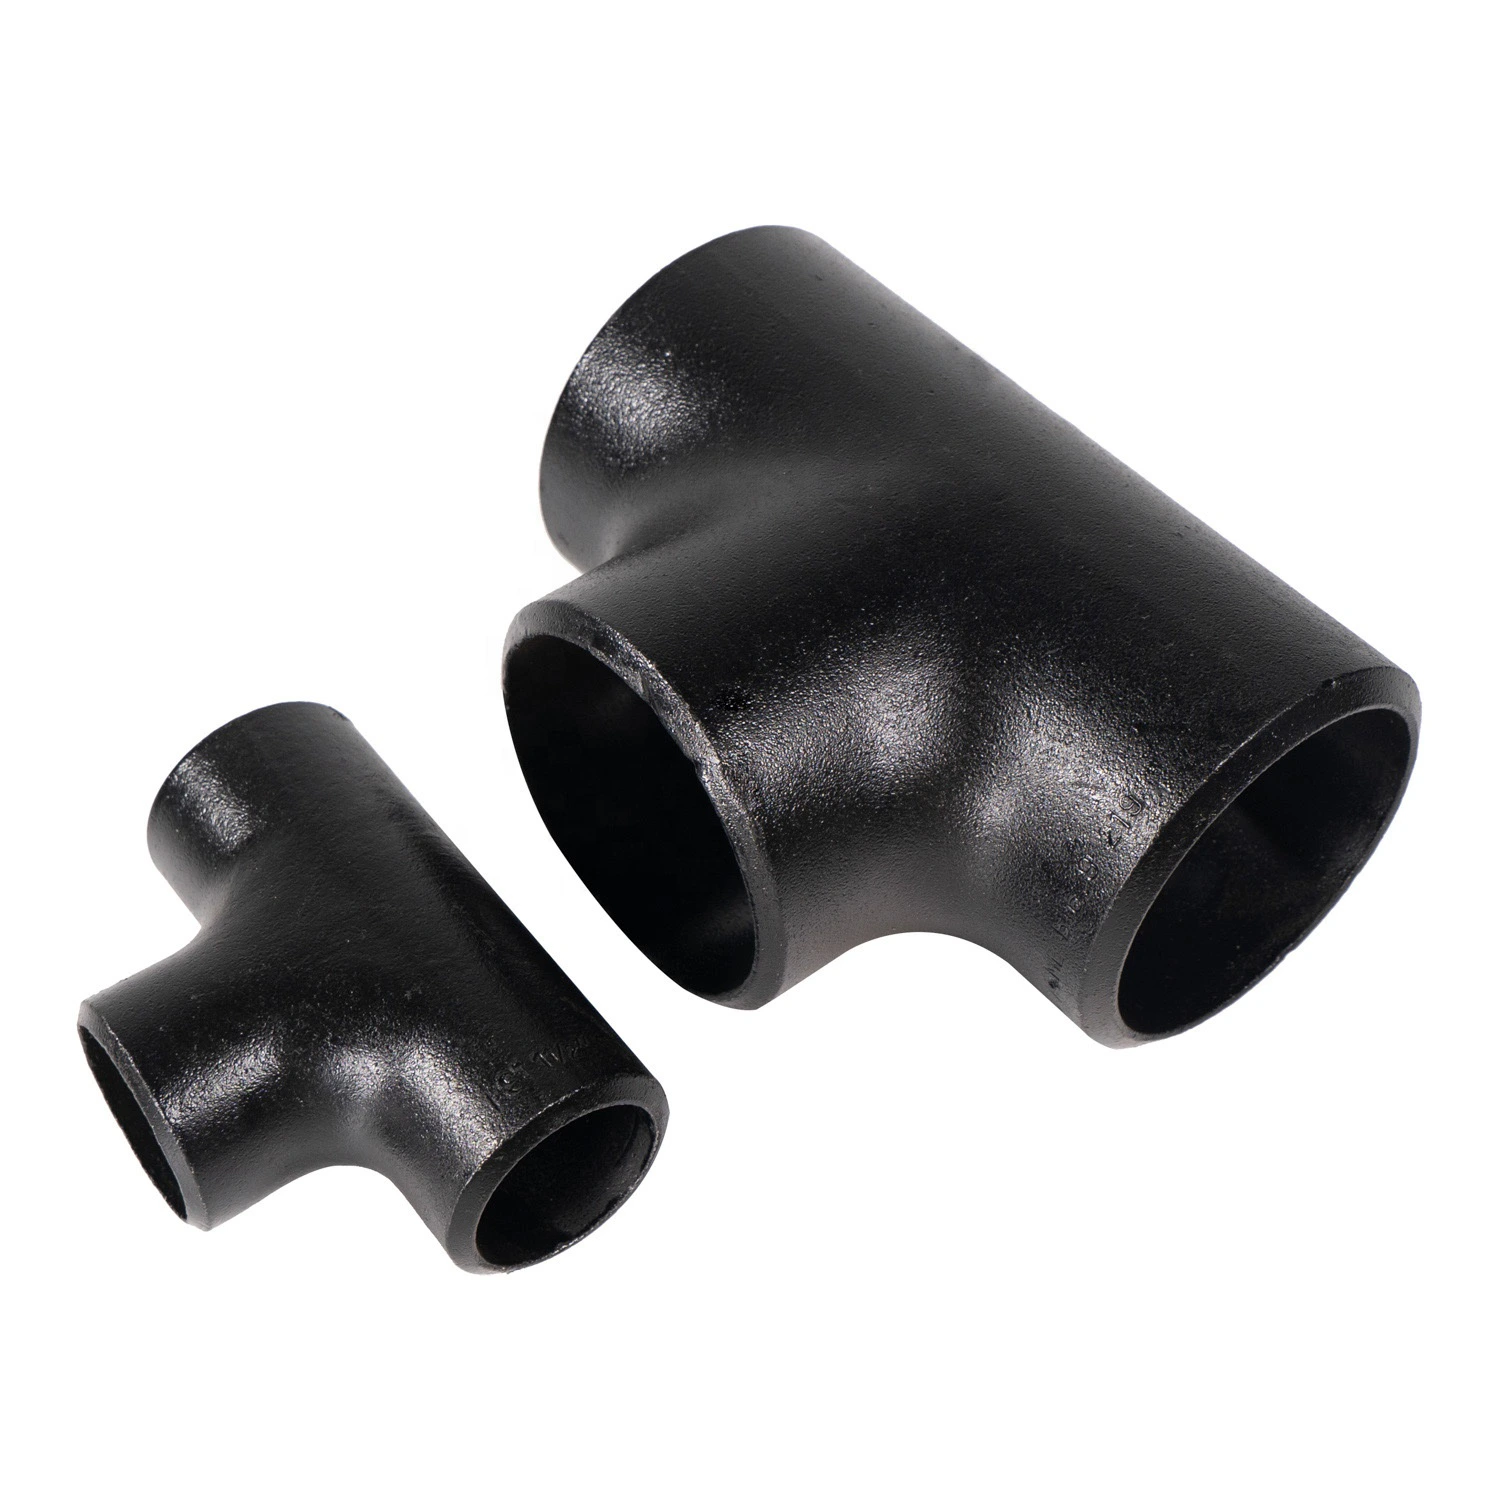
ASME B16.9 WPB Carbon Steel Reducing Butt-Welding Tee Enquiry
Per l’approvvigionamento industriale
Prepara una RFQ più chiara
Includi i dati seguenti per aiutare RELIA a comprendere il componente e definire il passo successivo.
- Disegno, campione o norma di riferimento
- Grado materiale e processo preferito
- Dimensioni, tolleranze e finitura superficiale
- Applicazione, quantità obiettivo e destinazione
Tempi di produzione, imballaggio e condizioni di spedizione vengono confermati per ogni progetto dopo l’accordo su specifiche e condizioni commerciali.
-
warranty1 yearcustomized supportOEM, ODM
-
model numbertee 6701TechnicCasting
-
ConnectivityMale/FemaleshapeEqual/Reducing
-
head codeHexagon/RoundSurface TreatmentPainting
-
Mounting hole diameter0.25 inPipe Class125
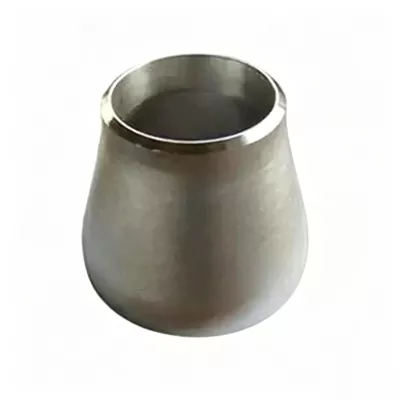
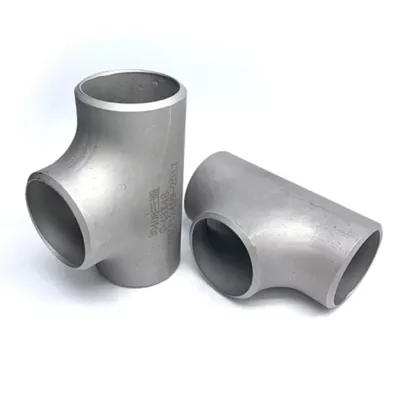
A reducing tee selection begins with the pipe routing and the three interfaces that must be joined. This enquiry retains the listing's WPB carbon-steel, butt-welding and ASME B16.9 requirements. Its mixed material choices and generic size labels need model-specific documentation before they establish an offered reducing configuration or its qualification.
Describe the branch layout before selecting an option
Show the two run connections and the branch on a sketch, with nominal size, outside diameter and wall thickness at each end. Explain the dimensional basis of the millimetre choices and identify the actual combination being offered. Confirm equal or reducing construction from that end map. Give centre-to-end dimensions, branch orientation and available space around the joining locations. Photographed tee forms do not establish those measurements for every option. The Male/Female, head-code and mounting-hole labels also cannot define the required weld preparation.
Link the chosen material to production evidence
For a WPB requirement, select carbon steel and request the full material specification and grade traceability. If a stainless-steel variant is proposed, agree a separate material grade and specification. Establish which ASME B16.9 edition and dimensional and inspection criteria apply to the selected item. Manufacturing records should reconcile the process wording before seamless or forged construction is accepted. Appearance alone cannot resolve that decision. State the coating preparation, coverage and condition required around the weld ends, since Painting does not describe a complete coating system.
Set acceptance for three joined interfaces
Review the run and branch connections together with the mating-pipe specifications and actual fluid, pressure, temperature and corrosion conditions. A Pipe Class 125 label is not a documented allowable-duty limit. Agree the joining and inspection requirements, then connect acceptance to one consistent drawing and matching material, manufacturing and inspection records.
Informazioni tecniche per ogni richiesta prodotto
Prepara i requisiti prima della conferma finale del prodotto.
La pagina prodotto è un punto di partenza. Disegni, campioni, interfacce, materiali, quantità e accettazione vengono verificati prima di confermare stock o produzione.
Valuta questo prodotto nel contesto del tuo progetto.
Condividi disegno, campione, riferimento, quantità e applicazione. I punti non definiti possono restare aperti.