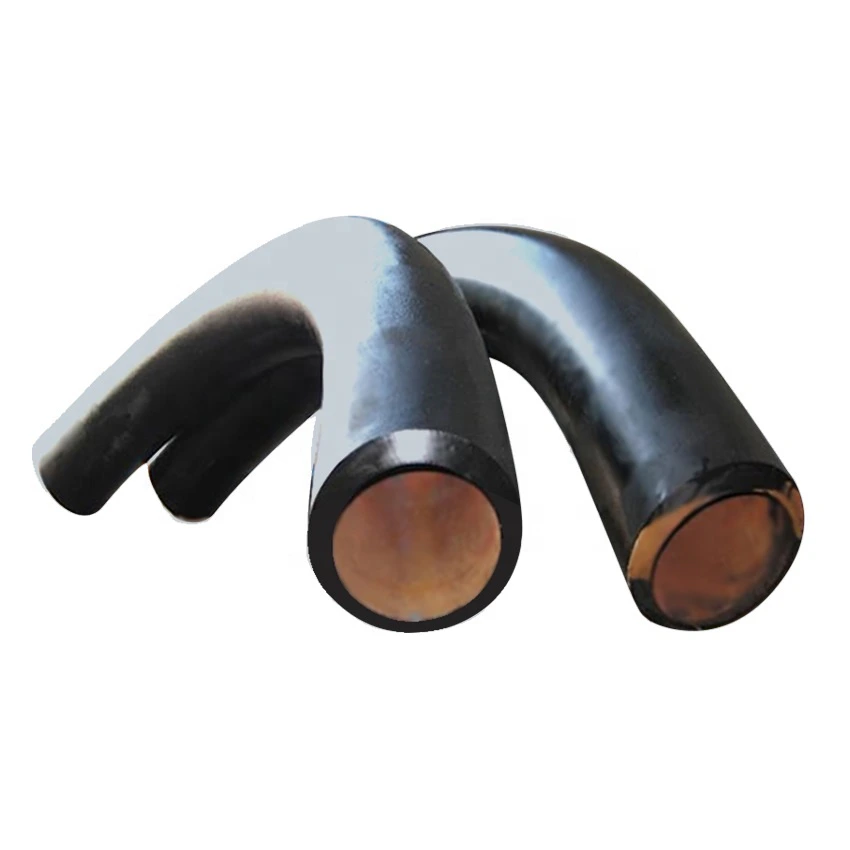
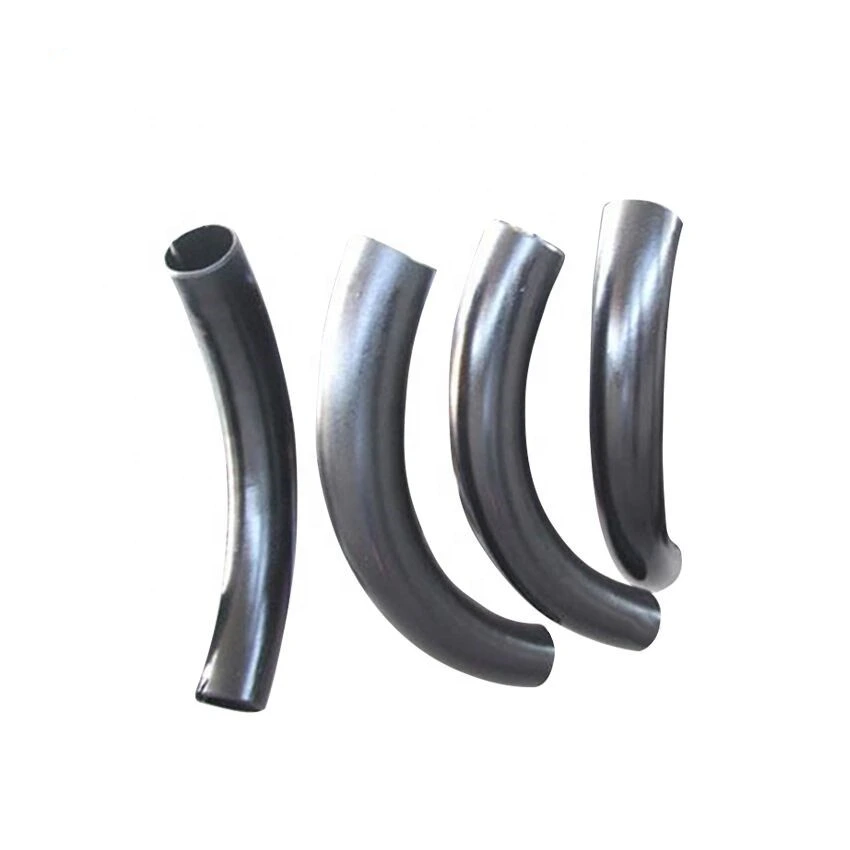
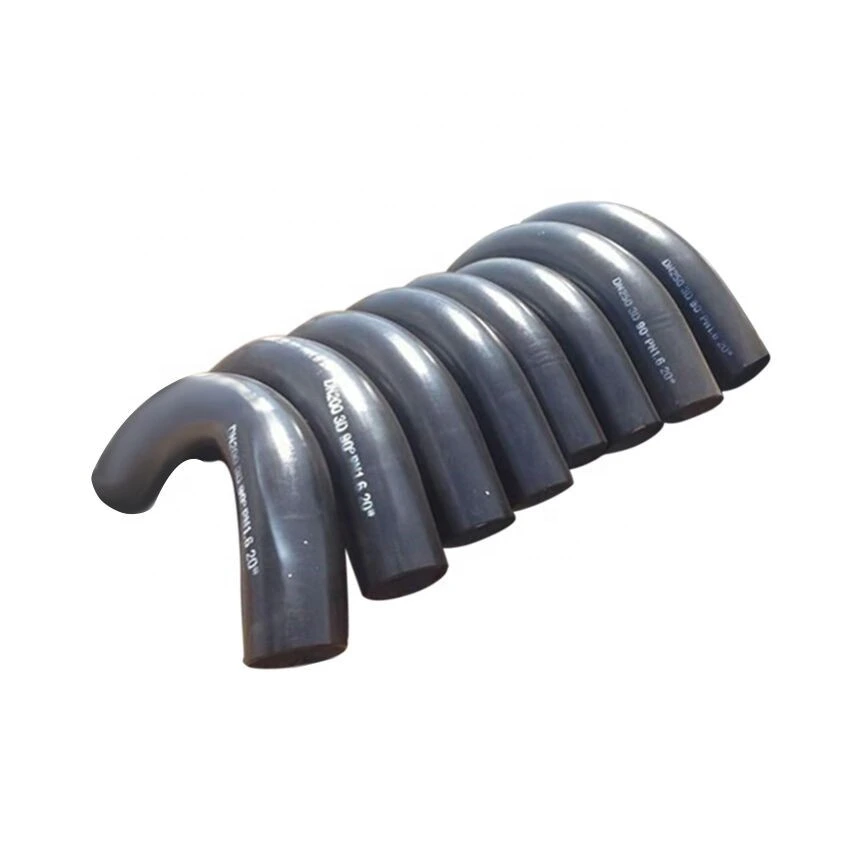
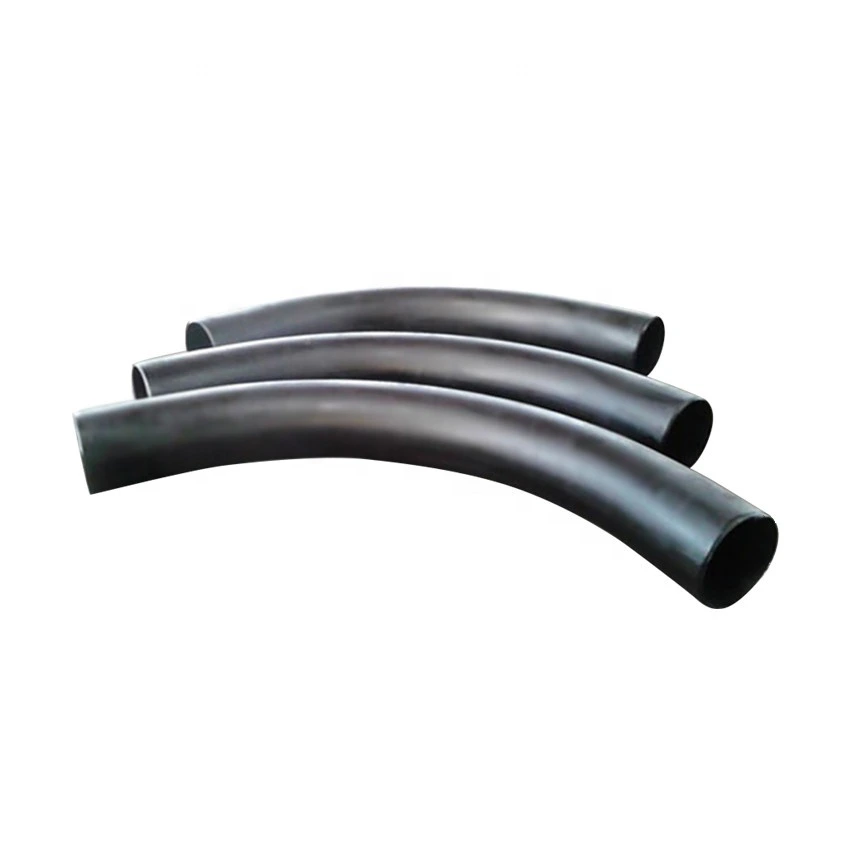
A106B 4D Carbon Steel Butt-Welding Pipe Bend Enquiry
للتوريد الصناعي
جهّز RFQ أكثر وضوحًا
أدرج المعلومات التالية كي تفهم RELIA القطعة وتناقش معك الخطوة التالية.
- رسم أو عينة أو معيار مرجعي
- درجة المادة والعملية المفضلة
- الأبعاد والتفاوتات وتشطيب السطح
- الاستخدام والكمية والوجهة
يتم تأكيد مدة الإنتاج والتعبئة وشروط الشحن لكل مشروع بعد الاتفاق على المواصفات والشروط التجارية.
-
warranty1 yearcustomized supportOEM, ODM
-
model numberbend 4056TechnicCasting
-
ConnectivityFemale/MaleshapeReducing
-
head codeRoundSurface TreatmentPainting
-
Mounting hole diameter0.26 inPipe Class150
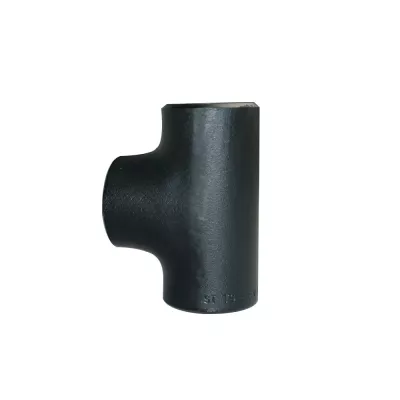
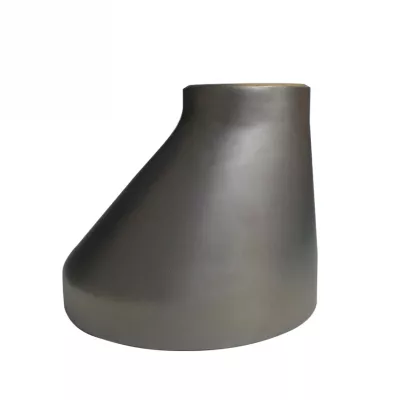
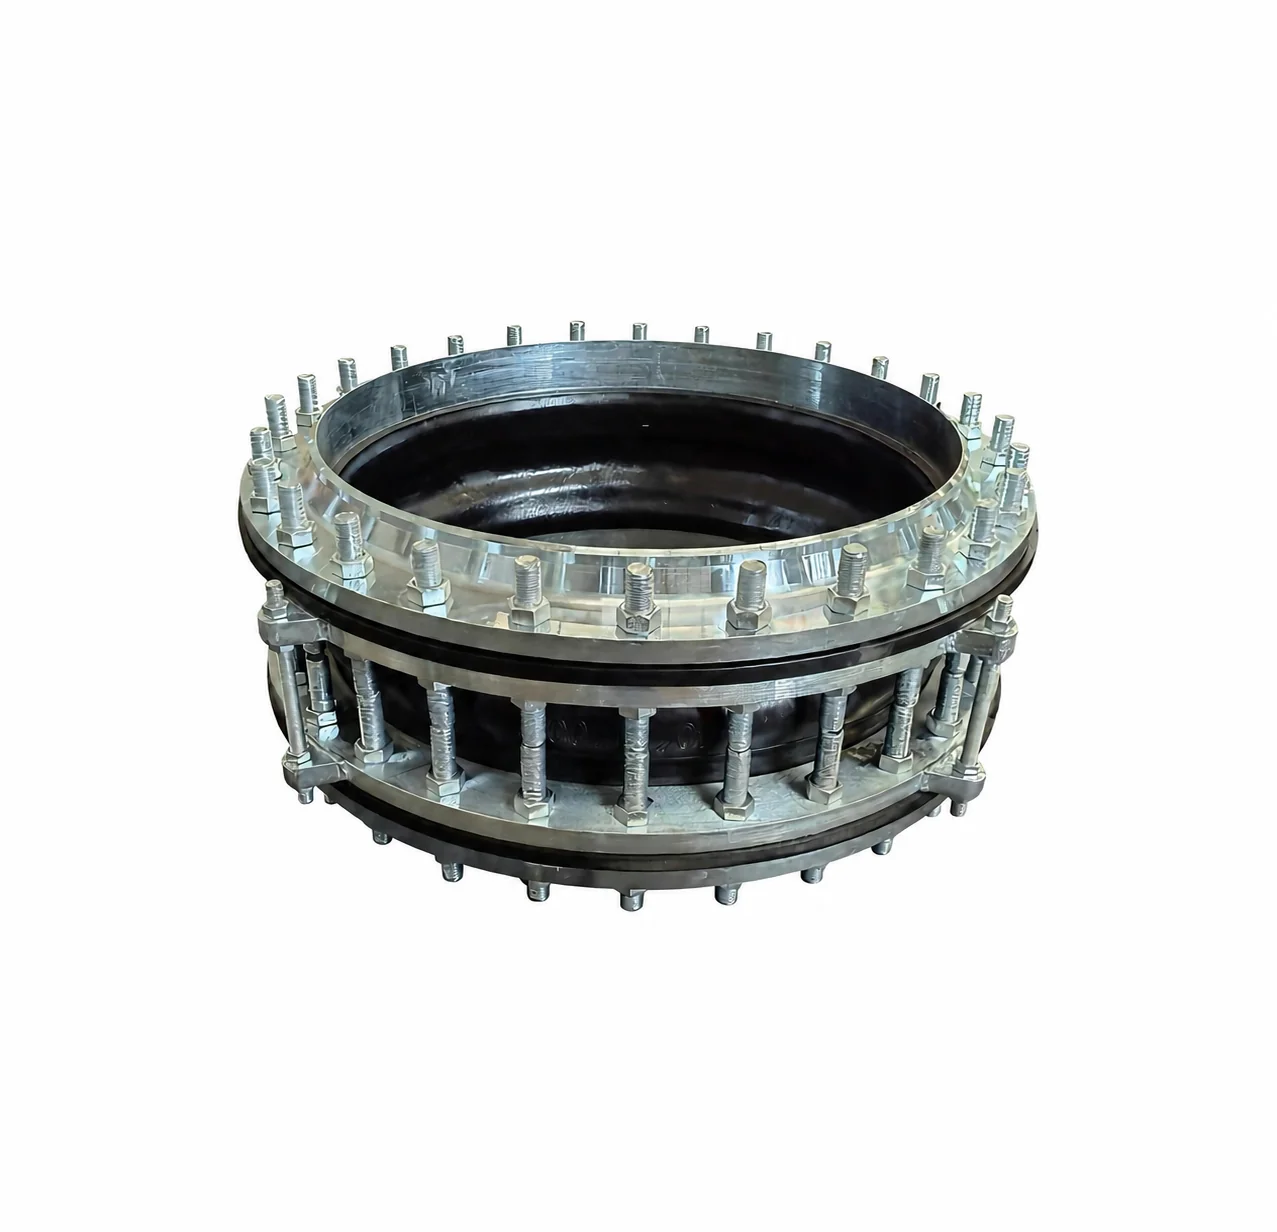
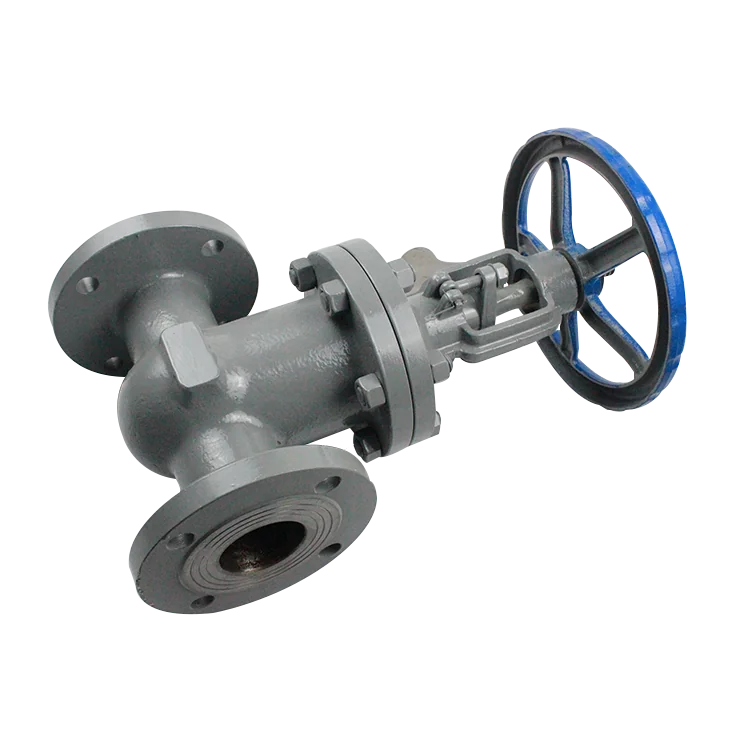
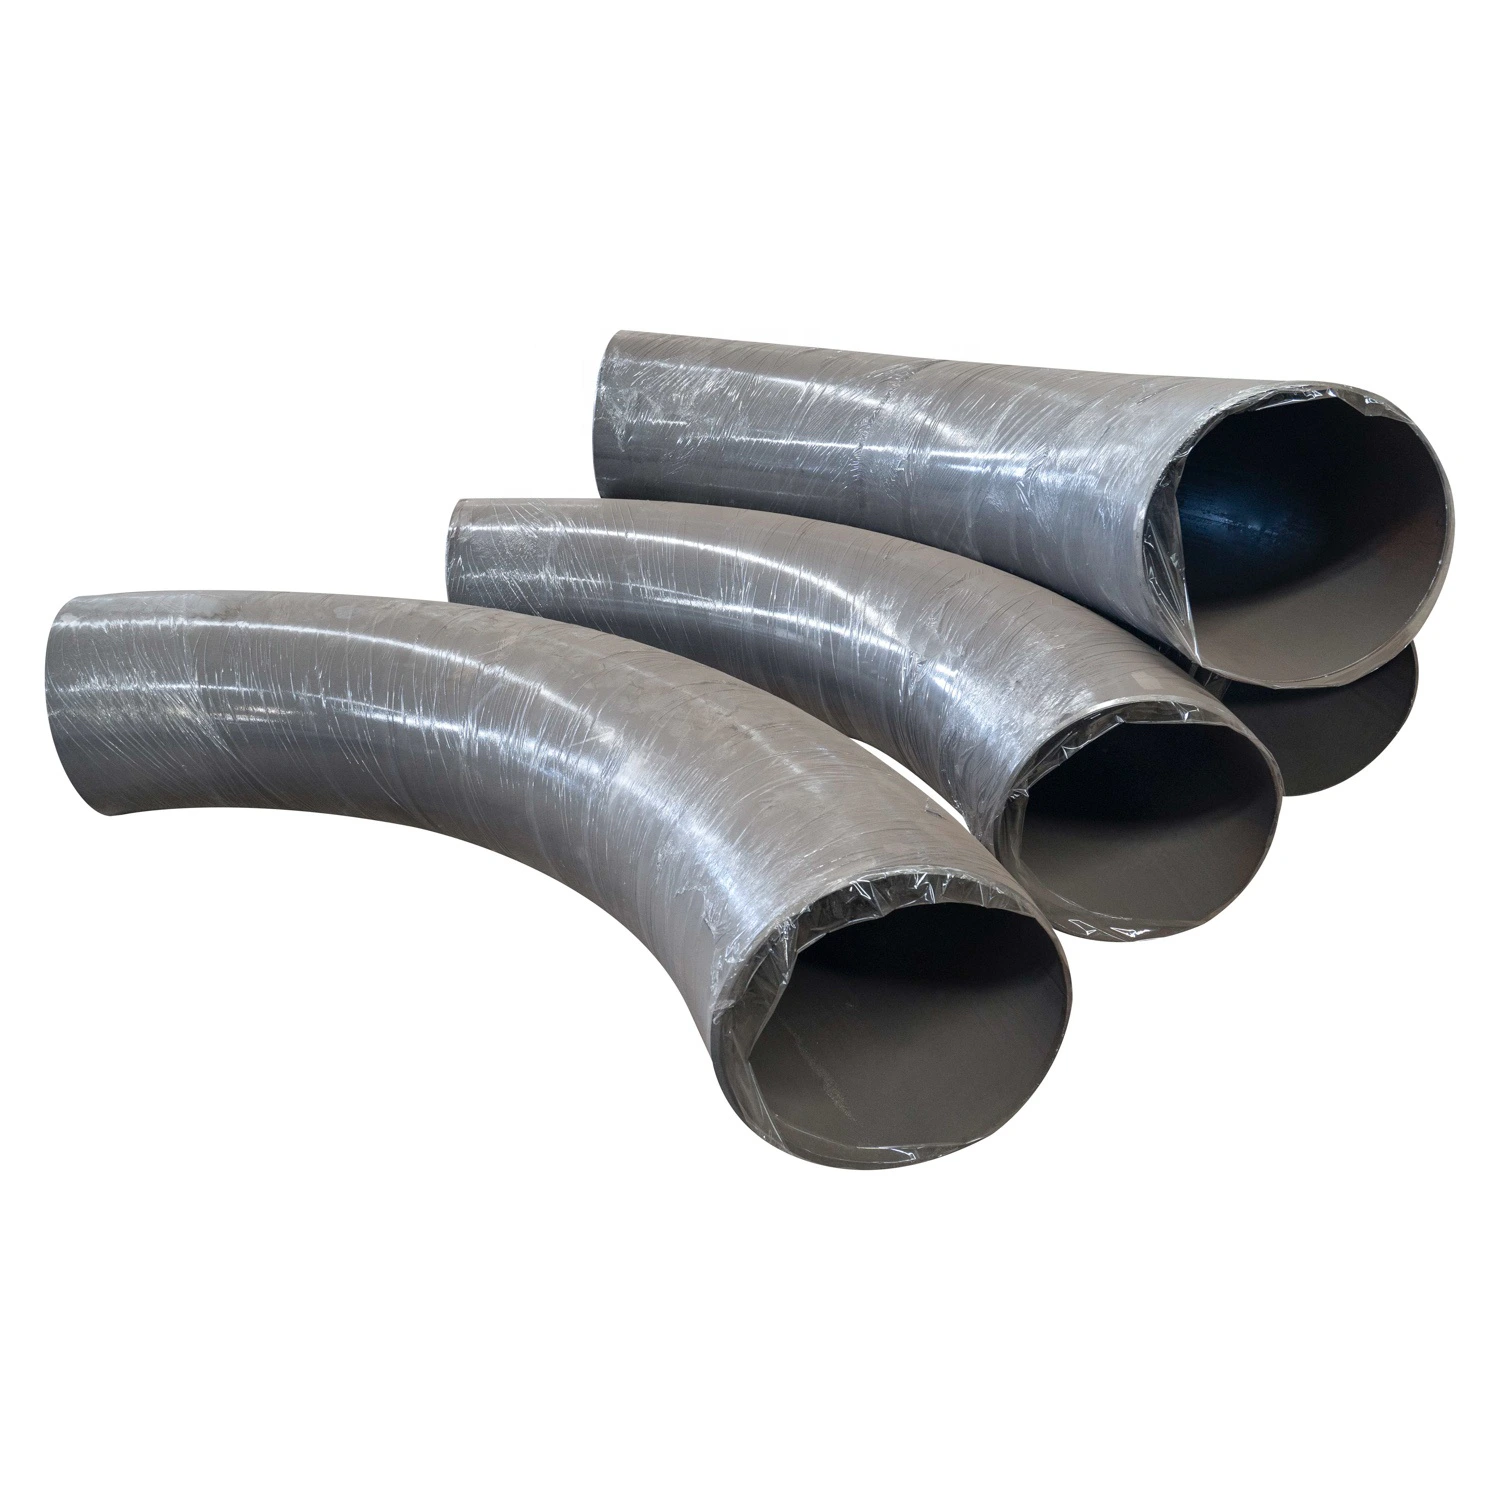
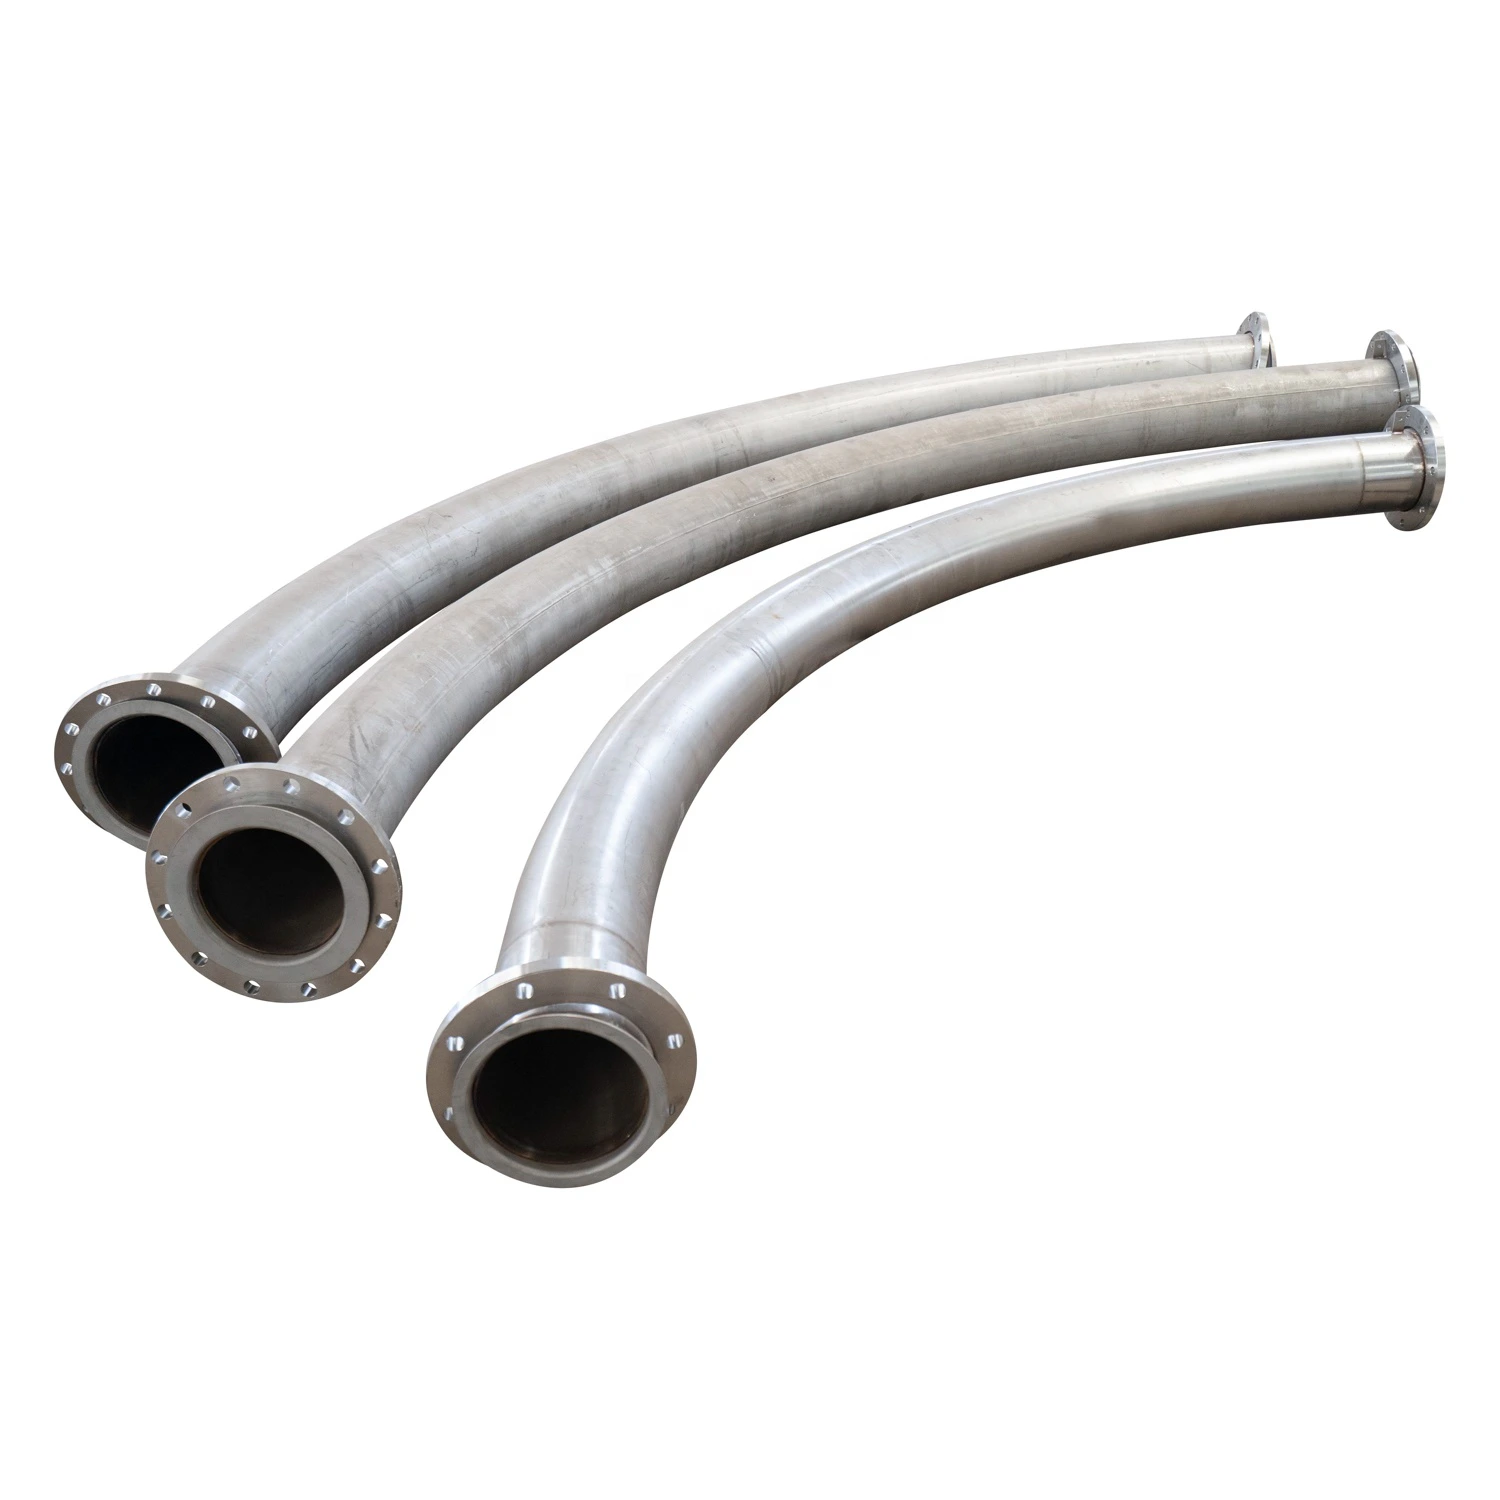
This carbon-steel bend enquiry retains the A106B, 4D and butt-welding requirements from the title. An actual selection needs those requirements linked to one drawing and material record. The Bend variants and curved-pipe photographs establish the family, but the photographs show different end forms and cannot assign one connection to every option.
Define the 4D convention on the route drawing
State the diameter basis used for 4D and identify the required centreline radius explicitly. Give the bend angle, tangent lengths and overall envelope against the pipe route. Explain what the millimetre options measure and specify nominal size, outside diameter and wall at both ends. If a reducing bend is required, identify the size pair and transition dimensions. Neither photographed curvature nor the Round and mounting-hole labels establish the measured radius or end geometry.
Identify the actual connection and material
Request an end-preparation drawing for the selected butt-welding model. Flanged ends visible in some photographs should not be assigned to that requirement without checking the offered item. Choose carbon steel and obtain the full material specification, grade and traceability records corresponding to A106B. A stainless-steel alternative requires separate grade selection. Ask which records cover the starting material and which cover the finished bend; a material label alone does not define the completed fitting's manufacturing and inspection acceptance.
Agree production and installed-joint evidence
Resolve the Casting field through production documentation before accepting a route. Define coating preparation and condition around the joining areas rather than relying on Painting alone. Provide mating-pipe details, fluid, pressure, temperature and corrosion conditions and the required joining and inspection plan. Pipe Class 150 does not establish an allowable pressure-temperature limit. Acceptance should connect one radius and end-pair drawing with matching material, finished-bend manufacturing and joint-duty records.
معلومات فنية لكل استفسار عن منتج
جهّز المتطلبات قبل التأكيد النهائي للمنتج.
صفحة المنتج هي نقطة البداية. تتم مراجعة الرسوم والعينات والواجهات والمواد والكميات ومتطلبات القبول قبل تأكيد المخزون أو الإنتاج المخصص.
ناقش هذا المنتج في سياق مشروعك.
شارك الرسم والعينة والمرجع والكمية ومعلومات التطبيق. يمكن ترك البنود غير المعروفة مفتوحة للمراجعة.