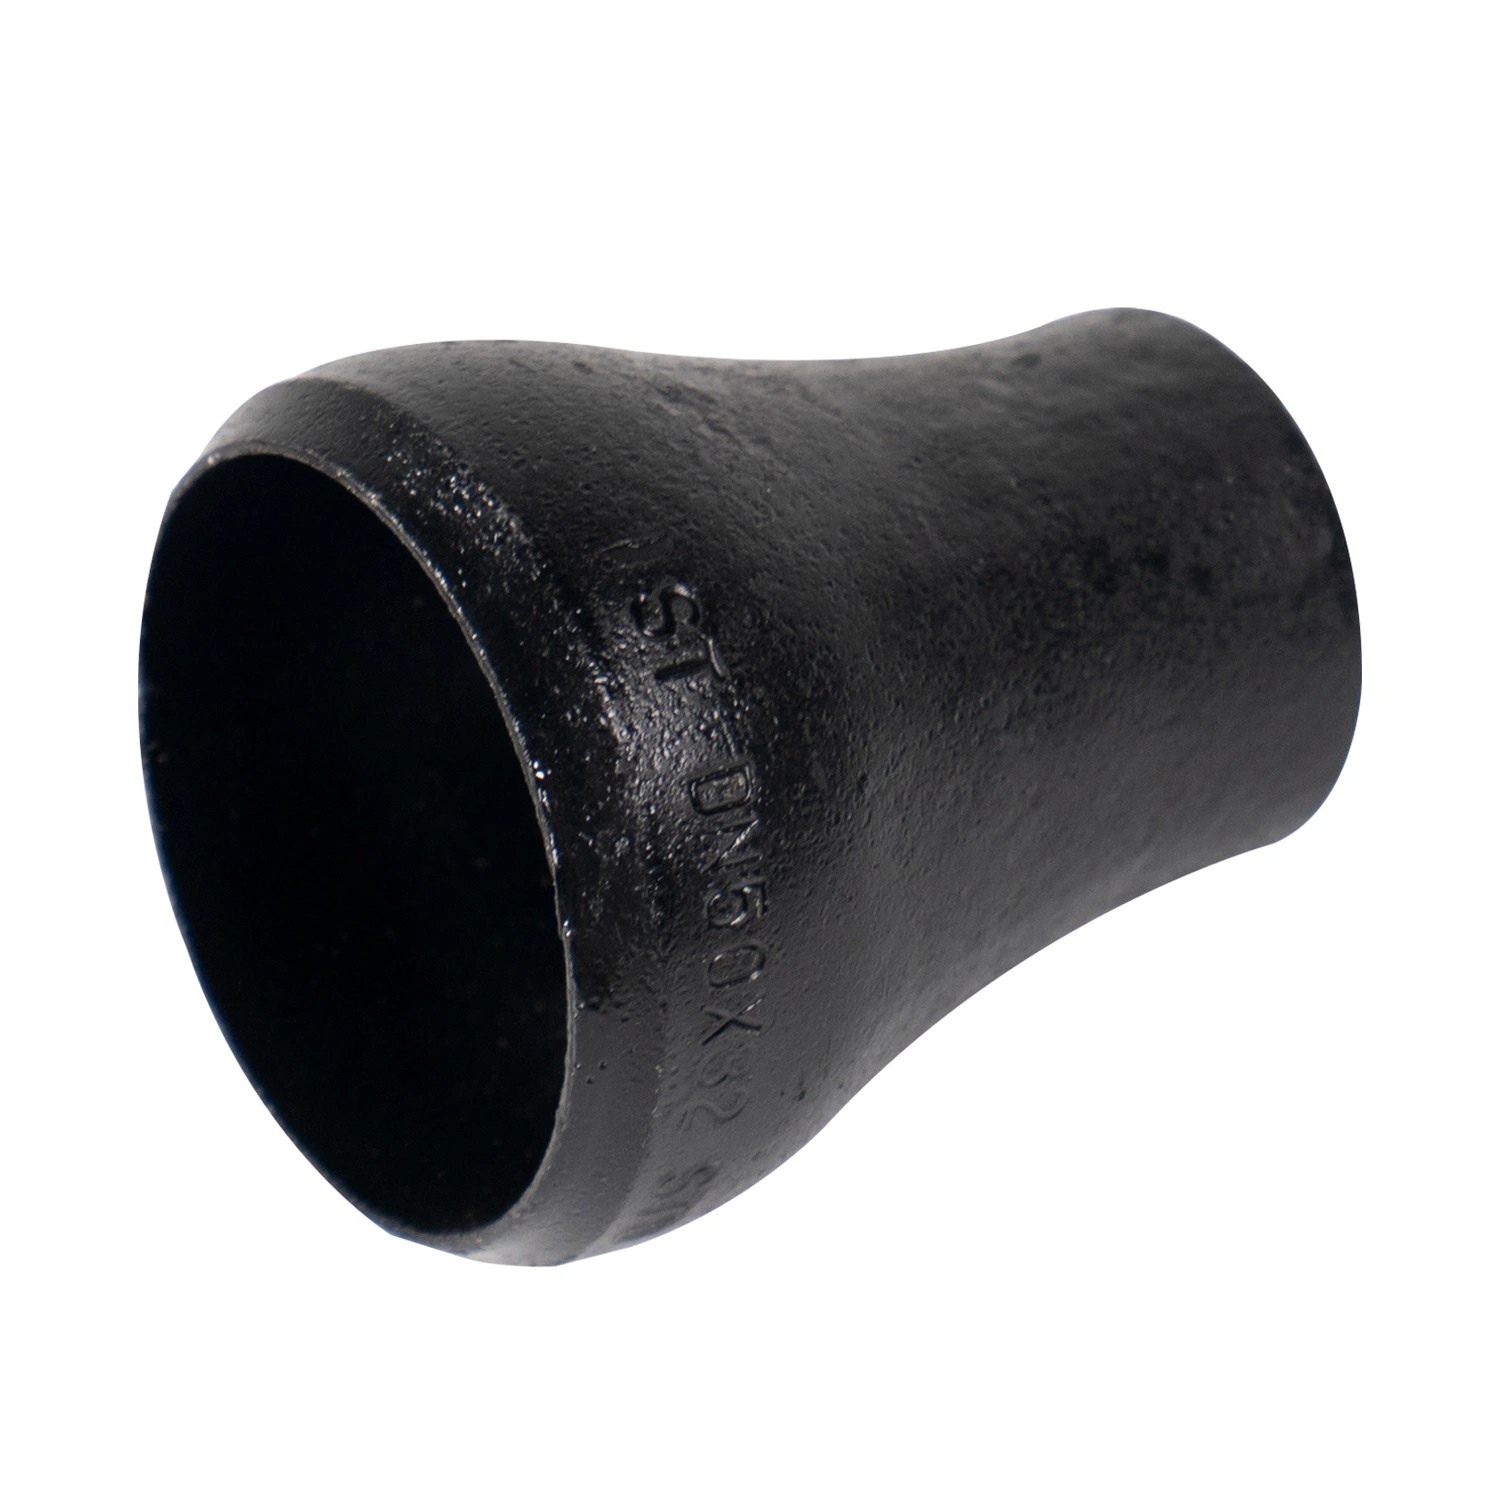
DN25 Carbon Steel Seamless Butt-Weld Concentric Reducer Enquiry
Для промышленных закупок
Подготовьте чёткий RFQ
Укажите данные ниже, чтобы RELIA поняла требования к детали и обсудила следующий шаг.
- Чертёж, образец или стандарт
- Марка материала и предпочтительный процесс
- Размеры, допуски и обработка поверхности
- Назначение, объём и место поставки
Срок производства, упаковка и условия доставки подтверждаются отдельно для каждого проекта после согласования спецификаций и торговых условий.
-
warranty1 yearcustomized supportOEM, ODM, OBM
-
TechnicForgedConnectivityWelding
-
shapeEqualhead codeHexagon
-
Surface TreatmentPaintingMounting hole diameter0.26 in
-
Pipe Class150SizeCustomized Size
-
Product nameElbow
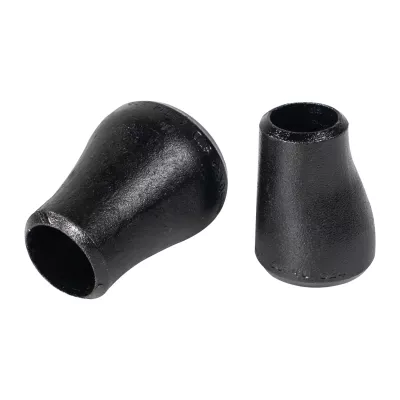
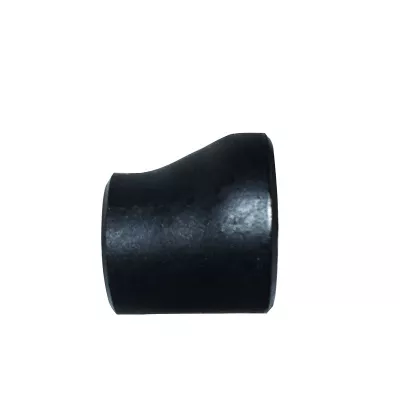
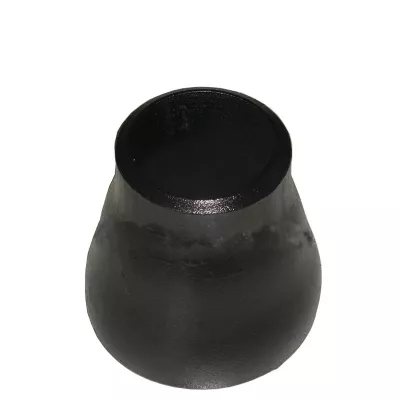
This carbon-steel butt-weld reducer enquiry includes DN25, seamless construction and a concentric transition requirement. The reducer options and tapered photograph establish the broad family. A selected drawing must explain which end DN25 describes and how the complete large-by-small pair relates to the listed millimetre choices.
Map DN25 to a complete two-ended transition
Identify the large and small nominal sizes separately, with measured outside diameters, actual walls and weld preparation. Show the required common centreline alignment, overall length and transition envelope. A single DN25 or millimetre label cannot define both openings. Compare the selected pair with the adjoining pipes and check installation clearance and access for welding and inspection. The photograph and its marking cannot establish the end sizes or exact concentric geometry of every option. Hexagon and the mounting-hole field do not substitute for that dimensional record.
Request the full ASTM specification and construction evidence
Select Carbon Steel for the title requirement and obtain the material specification number, edition and exact grade with traceable records. ASTM alone does not identify that package. Stainless Steel and Alloy choices require separate assignments. No wall schedule or dimensional standard number is supplied, so agree actual thickness, length, tolerances and inspection explicitly. Request records demonstrating the required seamless construction and explaining the actual forming route rather than treating Seamless or Forged wording as proof of manufacture.
Define finish and acceptance for both welded ends
Agree surface preparation, coating coverage and weld-zone condition beyond Painting. Supply both mating-pipe specifications and the fluid, pressure, temperature and corrosion conditions with joining and inspection requirements. Qualify the completed reducer for that service through material and joint evidence; the Pipe Class 150 label is insufficient by itself. Confirm the offered dimensional range and availability separately from Customized Size. Acceptance should identify the mapped DN25 end pair and link its drawing, actual walls and material/production records.
Техническая информация для каждого запроса
Подготовьте требования до финального подтверждения.
Страница товара — отправная точка. До подтверждения складского или заказного варианта проверяются чертежи, образцы, сопряжения, материалы, количество и приёмка.
Обсудите изделие в контексте вашего проекта.
Пришлите чертеж, образец, ссылку, количество и применение. Неясные пункты можно оставить открытыми.