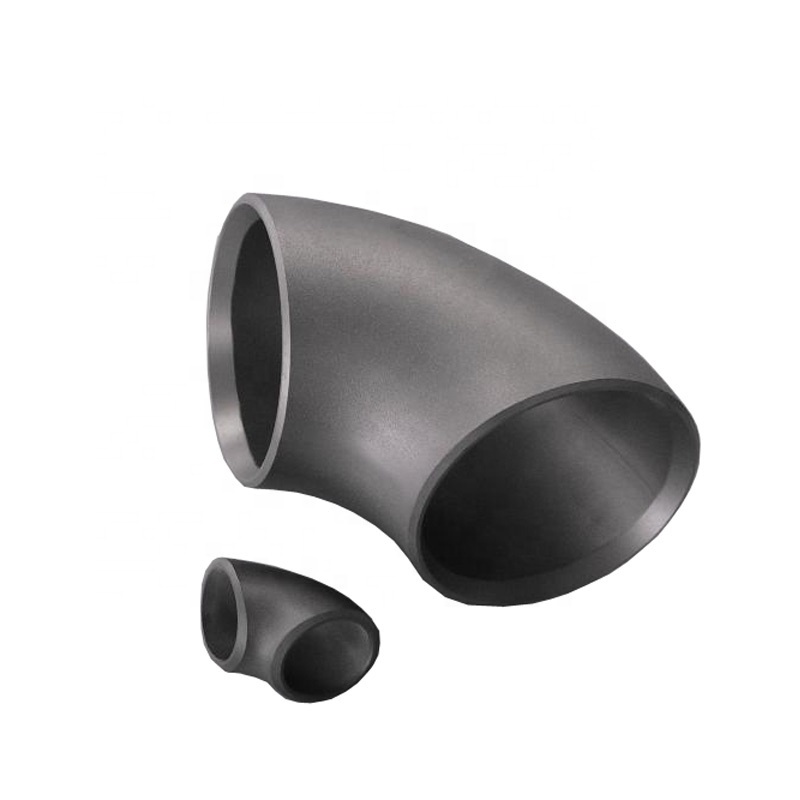
B16.9 Q235 1/2-Inch 90° Short-Radius Butt-Weld Elbow
Для промышленных закупок
Подготовьте чёткий RFQ
Укажите данные ниже, чтобы RELIA поняла требования к детали и обсудила следующий шаг.
- Чертёж, образец или стандарт
- Марка материала и предпочтительный процесс
- Размеры, допуски и обработка поверхности
- Назначение, объём и место поставки
Срок производства, упаковка и условия доставки подтверждаются отдельно для каждого проекта после согласования спецификаций и торговых условий.
-
warranty1 Yearcustomized supportOEM, ODM
-
model numberelbow 2417TechnicCasting
-
ConnectivityFemale/MaleshapeReducing
-
head codeRoundSurface TreatmentPainting
-
Mounting hole diameter0.17 inPipe Class150
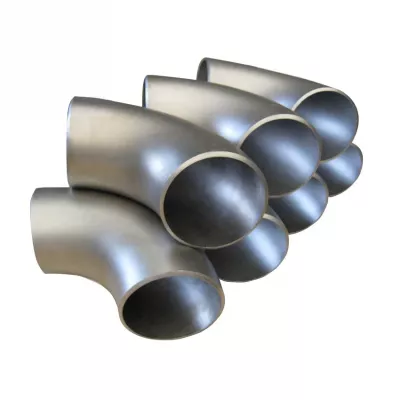
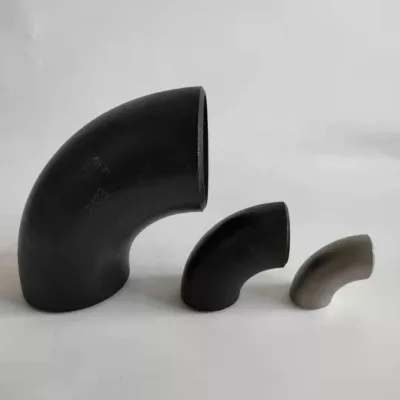
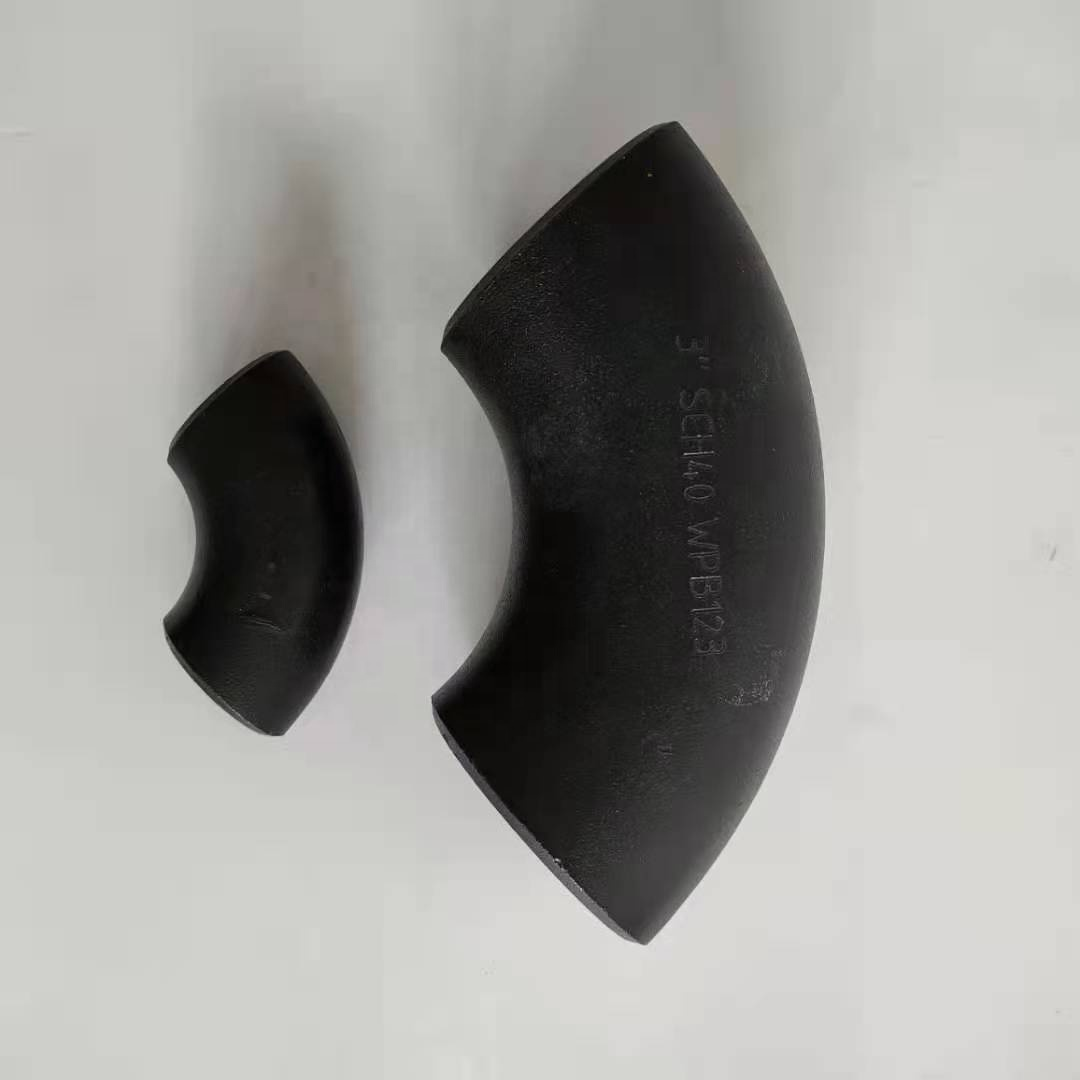
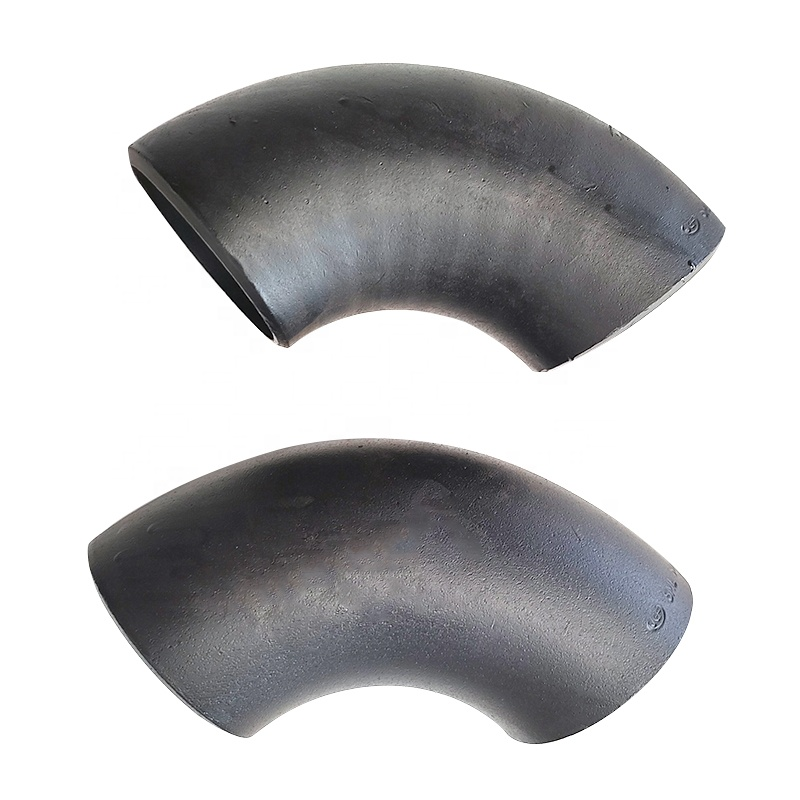
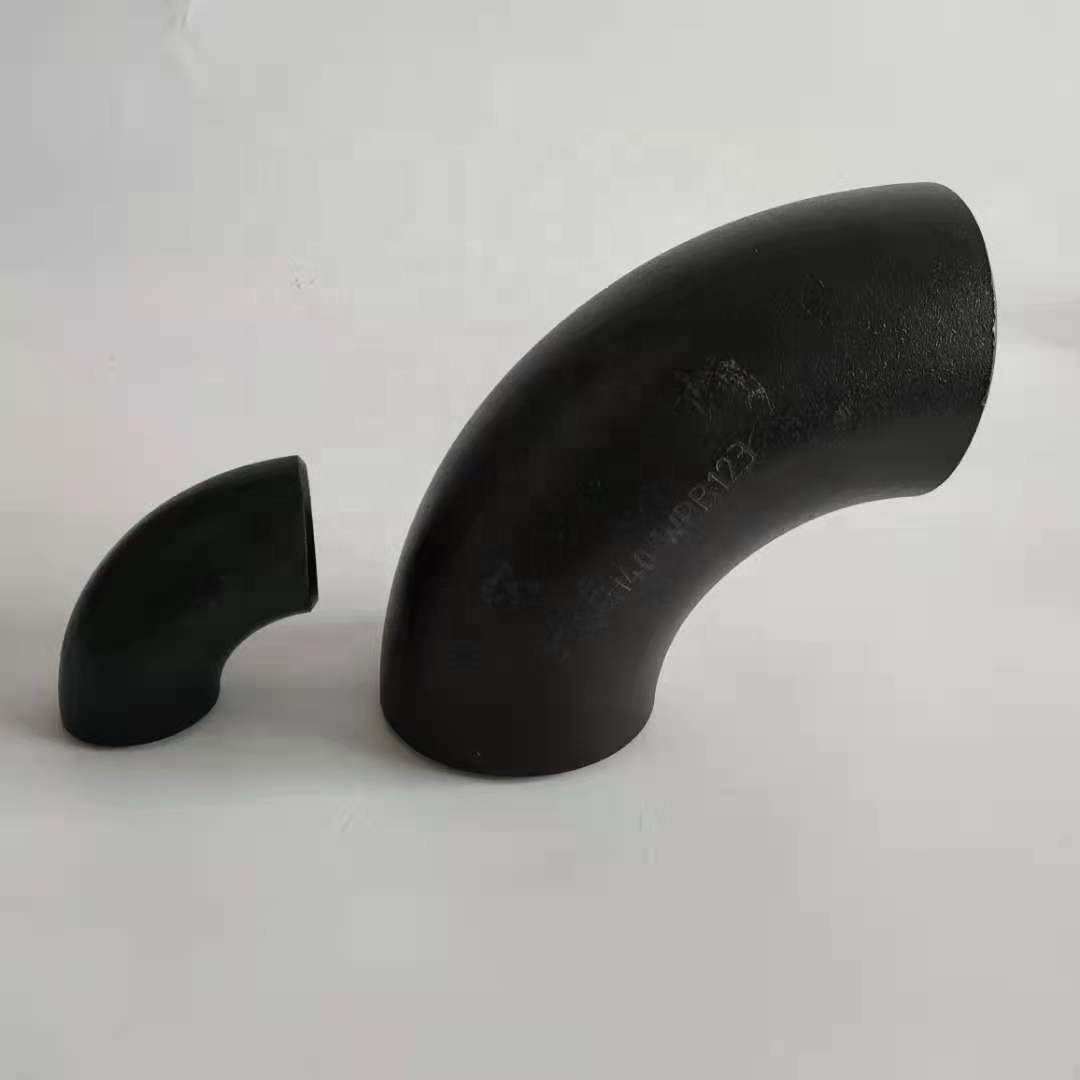
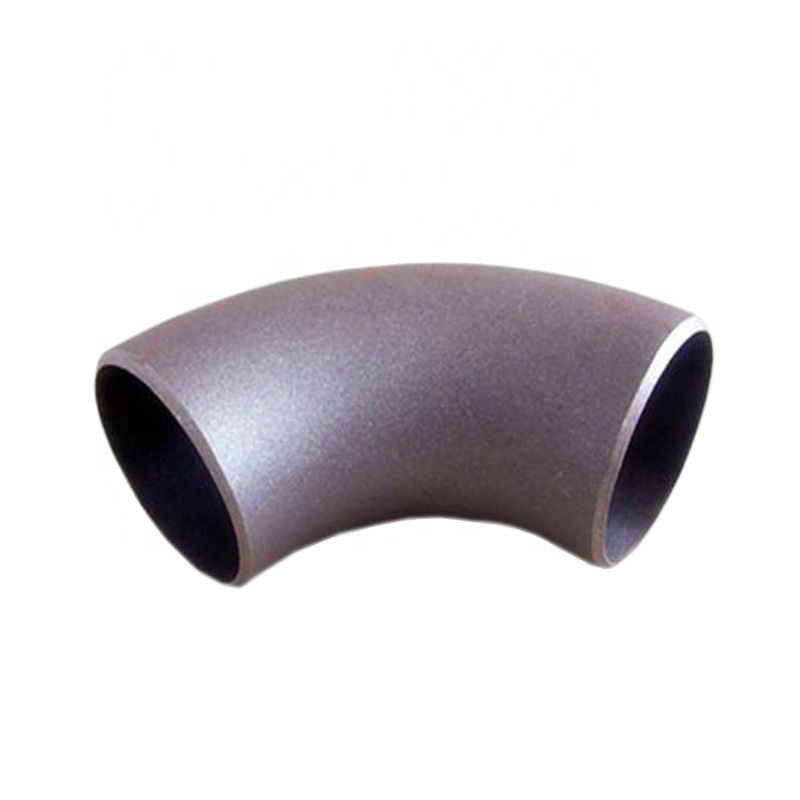
This elbow enquiry starts with the half-inch Q235 requirement in the title and the intended 90-degree short-radius butt-weld configuration. Select one offered model before assigning those requirements to an option. The millimetre size labels, material alternatives and Reducing field need a documented relationship to the actual bend and its pipe connections.
Identify both pipe ends before choosing a size
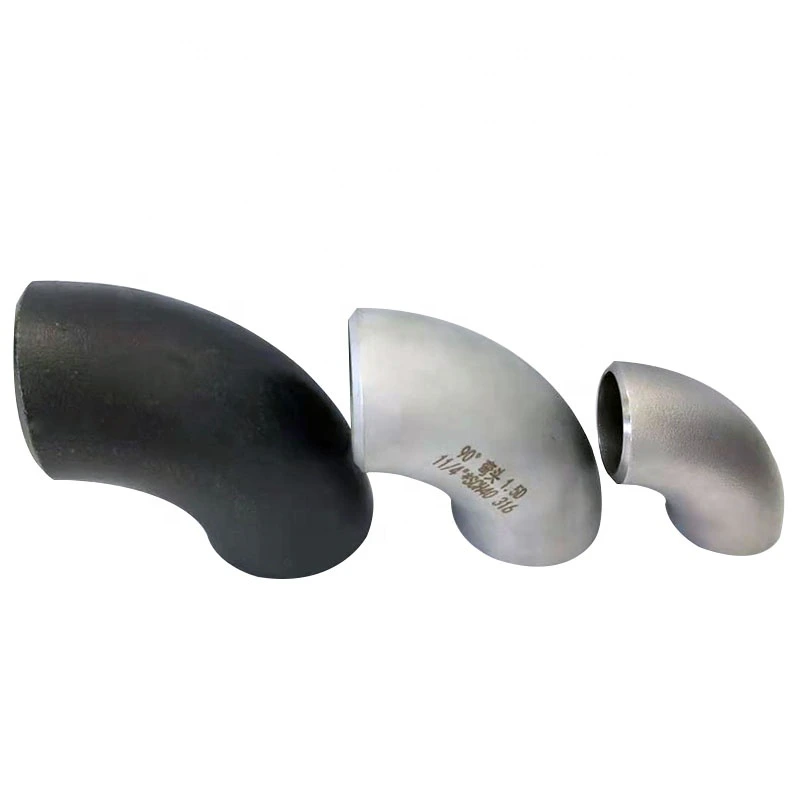
State the required nominal size and outside diameter for each end. Ask which millimetre-labelled option corresponds to the half-inch requirement and whether the selected model has equal or reducing ends. A Reducing label alone does not define the two sizes. Request an elbow drawing with wall thickness, centreline radius, end-to-centre dimensions and the accepted 90-degree angle. Check that this measured envelope fits the pipe route rather than estimating radius or end sizes from a product image.
Keep Q235 separate from photographic markings
Confirm the governing Q235 material specification and records for the selected carbon-steel item. A stainless-steel choice requires its own agreed grade. Visible markings on one photographed fitting do not identify every variant's grade or wall schedule. Request production and inspection evidence for the actual model before accepting its manufacturing route; the Casting field cannot replace that evidence. Define bevel, land and end wall for the mating pipe instead of relying on Female/Male as the connection description.
Establish the acceptance basis
Give the required B16.9 edition and dimensional inspection criteria alongside the joining and inspection requirements. Provide the fluid, operating pressure and temperature and relevant corrosion conditions for assessment of the complete welded joint. Class 150 does not by itself establish its pressure-temperature limit, and Painting or mounting-hole information does not qualify a protective finish or bend geometry. An actionable enquiry joins the half-inch option mapping and end-pair drawing to the exact Q235 specification, documented production route and agreed acceptance records.
Техническая информация для каждого запроса
Подготовьте требования до финального подтверждения.
Страница товара — отправная точка. До подтверждения складского или заказного варианта проверяются чертежи, образцы, сопряжения, материалы, количество и приёмка.
Обсудите изделие в контексте вашего проекта.
Пришлите чертеж, образец, ссылку, количество и применение. Неясные пункты можно оставить открытыми.